
The
pharmaceutical industry requires reliable, hygienic, and efficient equipment
for manufacturing high-quality liquid medicines. A Liquid Syrup
Manufacturing Process Plant is an important solution for pharmaceutical
manufacturers involved in the production of oral liquid syrups. It helps
organize and streamline different stages of syrup manufacturing while
maintaining hygienic processing conditions.
For
pharmaceutical companies, choosing the right manufacturing plant is important
for achieving consistent production, maintaining product quality, and improving
overall manufacturing efficiency. A properly designed Liquid Syrup
Manufacturing Process Plant can support different production requirements
and help manufacturers manage their syrup production processes more
effectively.
What Is a Liquid Syrup Manufacturing Process Plant?
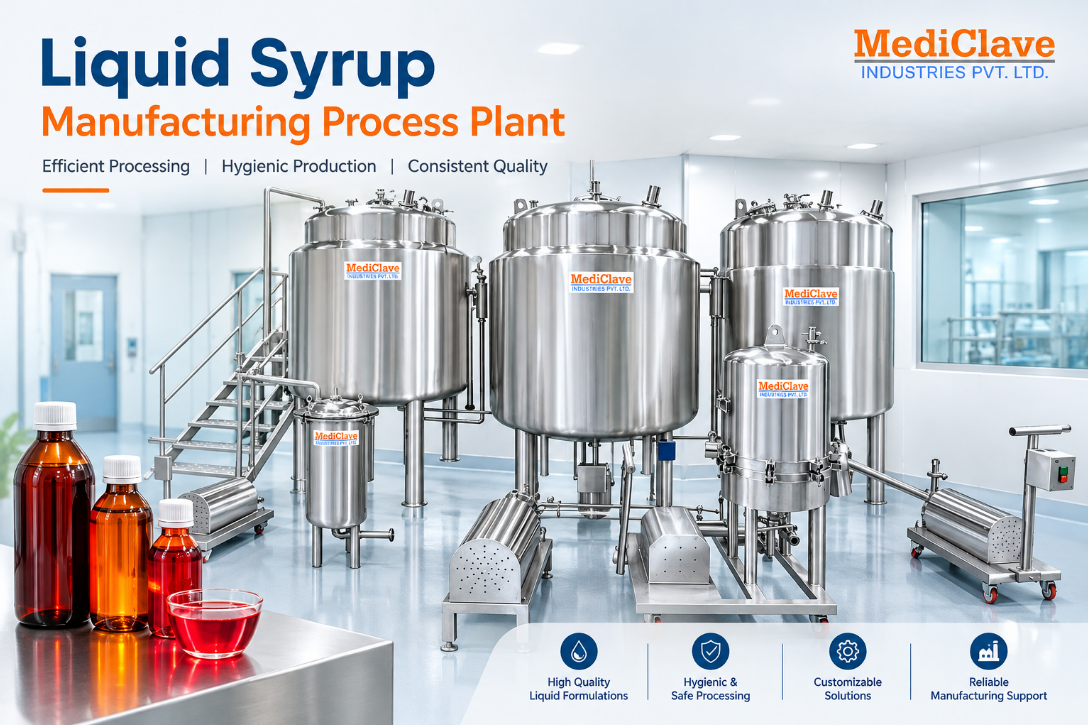
A Liquid
Syrup Manufacturing Process Plant is a complete processing setup used for manufacturing
pharmaceutical syrups and other liquid oral formulations. It can be used for
products such as medicinal syrups, oral solutions, vitamin syrups, pediatric
formulations, and other pharmaceutical liquid preparations.
The plant
brings together various processing activities into an organized manufacturing
system. Depending on the production requirement, the plant may include
different vessels, mixing systems, transfer arrangements, filtration equipment,
storage vessels, and other supporting equipment.
The
objective is to provide pharmaceutical manufacturers with a controlled and
hygienic environment for producing liquid formulations consistently.
How Does the Liquid Syrup Manufacturing Process
Work?
The
liquid syrup manufacturing process generally begins with the preparation of
purified water and other required ingredients. Raw materials are introduced
into the appropriate processing vessel according to the formulation and
manufacturing procedure.
The
ingredients are mixed carefully to achieve a uniform solution. Sugar or other
sweetening agents may be dissolved according to the formulation requirements.
Active pharmaceutical ingredients, flavors, colors, preservatives, and other
ingredients can then be incorporated during the appropriate processing stages.
Once
mixing and processing are completed, the liquid may undergo filtration to
remove unwanted particles and obtain the desired clarity. The processed syrup
can then be transferred to a suitable storage vessel before being sent for
further processing or filling.
The exact
manufacturing sequence depends on the formulation, production capacity, and
pharmaceutical manufacturing requirements.
Why Is a Good Manufacturing Plant Important?
A
well-designed liquid syrup manufacturing plant can help pharmaceutical
manufacturers maintain consistency throughout production. Manual handling and
poorly organized processing can create difficulties in maintaining uniformity
and hygienic conditions.
A
suitable manufacturing plant provides an organized approach to processing and
material transfer. It can also help reduce unnecessary handling and improve
workflow between different stages.
For
manufacturers producing pharmaceutical syrups on a regular basis, the right
processing setup can become an important part of maintaining efficient
production operations.
Key Benefits of a Liquid Syrup Manufacturing
Process Plant
A modern
Liquid Syrup Manufacturing Process Plant can offer several benefits to
pharmaceutical manufacturers.
Efficient Production:
The plant helps organize multiple stages of syrup manufacturing, supporting a
smoother production workflow.
Consistent Mixing:
Proper mixing arrangements help achieve better uniformity of ingredients
throughout the liquid formulation.
Hygienic Processing:
Pharmaceutical liquid products require hygienic manufacturing conditions.
Suitable equipment and controlled processing arrangements help support these
requirements.
Reduced Manual Handling:
An organized plant can reduce unnecessary manual intervention during processing
and material transfer.
Flexible Manufacturing:
Depending on the plant design, manufacturers can use the processing system for
different liquid formulations and production requirements.
Better Workflow:
A properly planned plant allows different manufacturing stages to be connected
logically, helping improve overall operational efficiency.
Applications of Liquid Syrup Manufacturing Plants
Liquid
syrup manufacturing plants are commonly used in pharmaceutical manufacturing
facilities for producing different types of oral liquid formulations.
Applications
can include:
- Pharmaceutical
syrups
- Oral
liquid medicines
- Pediatric
syrups
- Vitamin
and nutritional syrups
- Herbal
and healthcare liquid formulations
- Oral
solutions
- Flavored
medicinal liquids
- Other
liquid pharmaceutical preparations
The appropriate plant configuration depends on the product formulation, production volume, manufacturing process, and facility requirements.
Choosing the Right Liquid Syrup Manufacturing Process Plant
Before purchasing a Liquid Syrup Manufacturing Process Plant, pharmaceutical manufacturers should carefully consider their production requirements.
The
expected production volume is one of the important factors. Manufacturers
should select a plant that matches their current production needs while also
considering future expansion.
The type
of formulation is another important consideration. Different pharmaceutical
liquids may require different processing and mixing arrangements.
Manufacturers
should also consider hygienic design, ease of cleaning, material compatibility,
operating workflow, and integration with other production equipment.
Working
with an experienced pharmaceutical process equipment manufacturer can help
customers select a suitable solution based on their specific manufacturing
requirements.
Why Choose Mediclave Industries?
Mediclave
Industries is a pharmaceutical process equipment manufacturer providing
equipment and manufacturing solutions for pharmaceutical and healthcare
industries. The company focuses on developing equipment designed around
customer production requirements.
For
companies looking for a Liquid Syrup Manufacturing Process Plant,
Mediclave Industries can provide solutions suitable for different
pharmaceutical liquid manufacturing applications.
The right
equipment selection can help manufacturers establish an efficient production
workflow while supporting hygienic and consistent processing.
Conclusion
A Liquid
Syrup Manufacturing Process Plant plays an important role in modern
pharmaceutical liquid manufacturing. From ingredient preparation and mixing to
filtration, storage, and transfer, the plant helps organize the overall
production process in a systematic manner.
For
pharmaceutical manufacturers, selecting the right plant is an important
investment. Production capacity, formulation requirements, hygienic processing,
workflow, cleaning requirements, and future expansion should all be considered
before making a purchase decision.
If you
are planning to establish or upgrade a pharmaceutical liquid syrup manufacturing
facility, choosing the right process equipment manufacturer can make the
planning and implementation process easier.
Mediclave Industries provides pharmaceutical process equipment
solutions for manufacturers looking to improve their liquid manufacturing
operations. Contact the team to discuss your Liquid Syrup Manufacturing
Process Plant requirements and find a suitable solution for your production
facility.