
Steam + Air Mixture Sterilizer Ahmedabad | Reliable Sterilization | Ahmedabad
the pharmaceutical and biotechnology industries, sterilization is not just another manufacturing step—it is one of the most critical processes that directly impacts product safety, quality, and regulatory compliance. Every injectable medicine, IV fluid, ophthalmic product, medical device, and pharmaceutical solution must be sterilized correctly before it reaches patients. Even a minor variation in sterilization temperature or pressure can affect product integrity, making the selection of the right sterilization equipment extremely important.
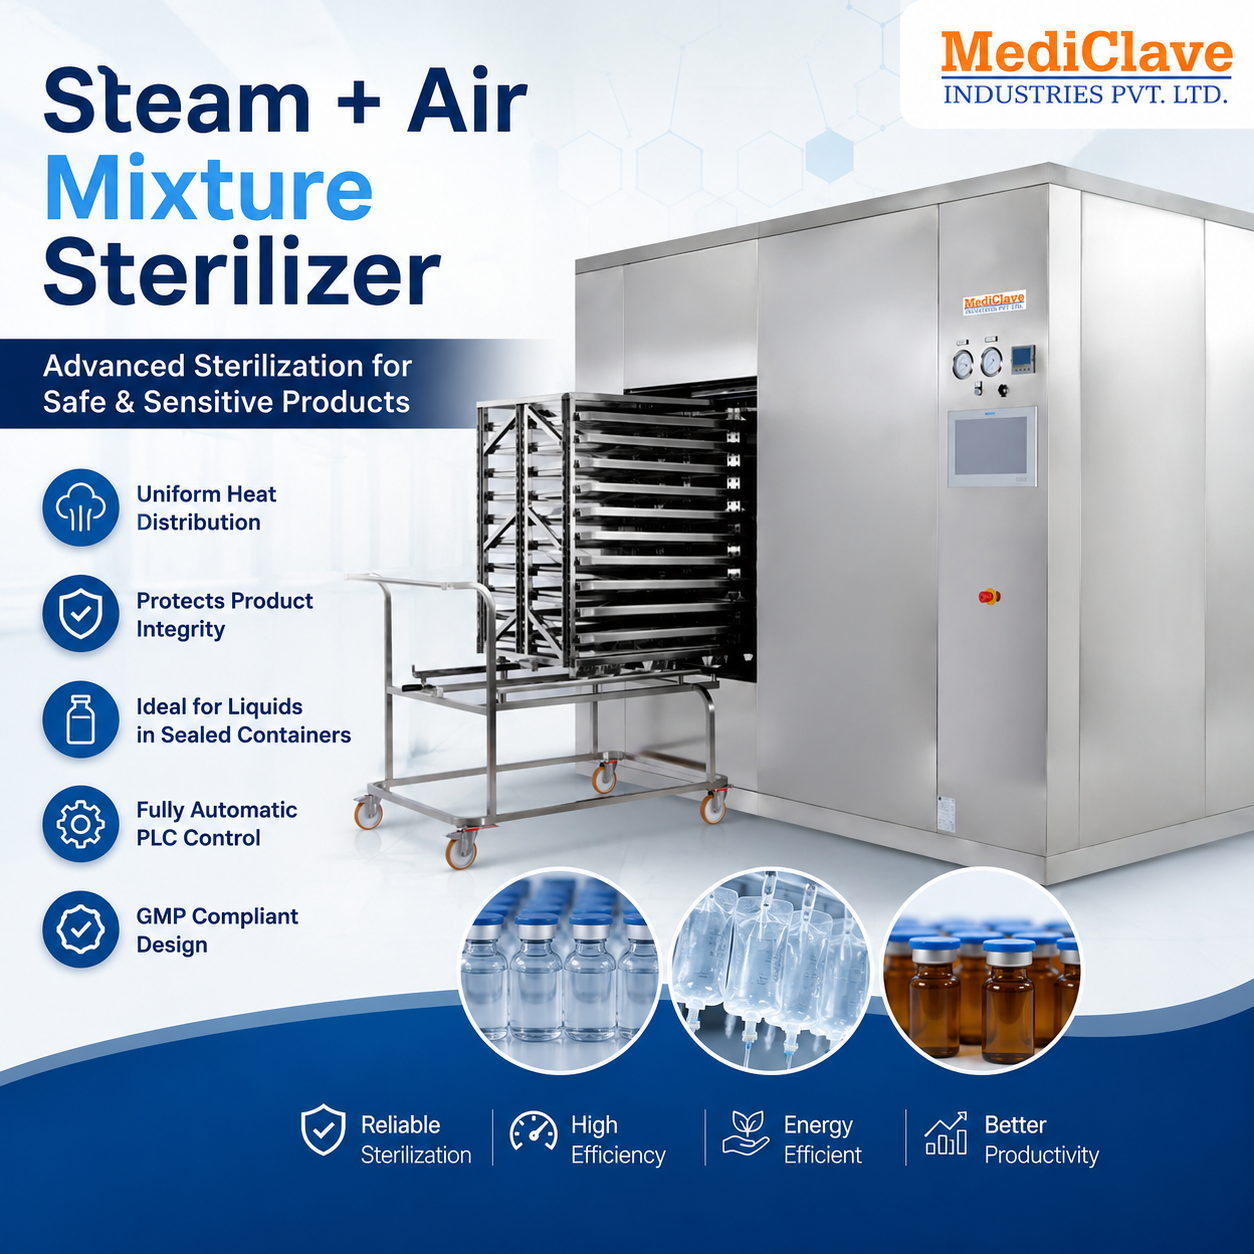
Among the most advanced sterilization technologies available today, the Steam + Air Mixture Sterilizer has become the preferred choice for manufacturers producing temperature-sensitive products in sealed containers. Unlike conventional saturated steam sterilizers, this system combines saturated steam with filtered compressed air to achieve highly uniform heat distribution throughout the sterilization chamber. This ensures every product receives the same sterilization conditions while preventing damage caused by excessive pressure differences.
At Mediclave Industries Pvt. Ltd., we manufacture advanced pharmaceutical sterilization equipment designed to meet the demanding requirements of GMP, FDA, WHO-GMP, and international pharmaceutical standards. Our Steam + Air Mixture Sterilizer is engineered to provide outstanding sterilization efficiency, consistent performance, and maximum product protection.
In this comprehensive guide, you will learn everything about Steam + Air Mixture Sterilizers, including their working principle, applications, advantages, technical features, validation requirements, maintenance practices, and how to select the ideal sterilizer for your pharmaceutical facility.
What is a Steam + Air Mixture Sterilizer?
A Steam + Air Mixture Sterilizer is a pharmaceutical sterilization system that uses a controlled mixture of saturated steam and sterile compressed air inside the chamber. The steam provides the necessary sterilization temperature, while compressed air balances chamber pressure and ensures uniform heat distribution.
This technology is especially suitable for products packed in:
Glass bottles
Plastic bottles
Flexible IV bags
Ampoules
Vials
Prefilled syringes
Infusion containers
Sealed pharmaceutical containers
Unlike ordinary steam sterilizers, the Steam + Air Mixture Sterilizer prevents container deformation, breakage, or leakage by maintaining precise pressure throughout the sterilization cycle.
Why Traditional Steam Sterilizers May Not Be Enough
Conventional steam sterilizers work exceptionally well for porous loads, stainless steel equipment, and many pharmaceutical materials. However, when sterilizing sealed liquid containers, they may create uneven heat transfer or pressure imbalances.
This can result in:
Broken glass containers
Swollen plastic bottles
Deformed IV bags
Product leakage
Inconsistent sterilization
Reduced product quality
For these reasons, pharmaceutical manufacturers increasingly choose Steam + Air Mixture Sterilizers for terminal sterilization applications.
For products requiring conventional saturated steam sterilization, Mediclave Industries also manufactures the Saturated Steam Sterilizer (Autoclave):
https://www.mediclaveindustries.in/saturated-steam-sterilizer/
How Does a Steam + Air Mixture Sterilizer Work?
The sterilization process involves carefully controlling temperature, pressure, steam flow, and sterile air throughout the cycle.
The basic process includes:
Loading
Products are arranged inside stainless steel loading racks to allow proper circulation.
Air Removal
The chamber is prepared for sterilization using a controlled process.
Steam Introduction
Pure saturated steam enters the chamber.
Sterile Air Injection
Filtered compressed air is introduced simultaneously.
This air performs two important functions:
Maintains chamber pressure
Improves heat distribution
Sterilization Holding Time
The chamber maintains the required sterilization temperature for the validated duration.
Cooling Phase
Cooling water and air pressure are carefully controlled to protect the containers.
Drying and Unloading
Products are removed after completing the validated sterilization cycle.
Industries Using Steam + Air Mixture Sterilizers
This equipment is widely used in:
Pharmaceutical manufacturing
Injectable medicine production
Biotechnology companies
Vaccine manufacturing
IV fluid manufacturing
Ophthalmic solution production
Nutraceutical manufacturing
Medical device sterilization
Research laboratories
Healthcare manufacturing facilities
Products Commonly Sterilized
Steam + Air Mixture Sterilizers are suitable for:
Injectable solutions
Saline bottles
IV fluids
Glucose solutions
Eye drops
Dialysis fluids
Vaccines
Biological products
Pharmaceutical liquids
Plastic infusion bottles
Glass bottles
Sealed containers
Prefilled syringes
Key Features
Modern Steam + Air Mixture Sterilizers include numerous advanced features that improve efficiency and reliability.
Some important features include:
Stainless steel construction
PLC-based automatic control
Touchscreen HMI
Recipe management
Real-time pressure monitoring
Uniform temperature distribution
Sterile compressed air filtration
Automatic cycle recording
GMP-compliant design
Validation-friendly software
Safety interlocks
Data logging
SCADA compatibility
Low maintenance requirements
Major Advantages
Uniform Temperature Distribution
The combination of steam and air ensures even heating across every shelf and every container.
Product Protection
Controlled chamber pressure prevents bottle breakage and package deformation.
Better Sterilization Efficiency
Every product receives identical sterilization exposure.
Suitable for Heat-Sensitive Containers
Plastic containers remain stable throughout the cycle.
Regulatory Compliance
Designed to satisfy pharmaceutical validation requirements.
High Automation
Minimal operator intervention improves consistency.
Faster Batch Processing
Efficient cycle management increases productivity.
Lower Product Rejection
Reduced damage means better production yield.
Importance of Pressure Control
Pressure is just as important as temperature.
During sterilization, liquid products expand because of heat. If external chamber pressure is too low:
Glass bottles may crack.
Plastic containers may swell.
Caps may loosen.
Products may leak.
The Steam + Air Mixture Sterilizer continuously adjusts air pressure to match the product's internal pressure, ensuring container integrity throughout the cycle.
Validation Requirements
Validation is essential in pharmaceutical manufacturing.
A validated Steam + Air Mixture Sterilizer typically undergoes:
Installation Qualification (IQ)
Operational Qualification (OQ)
Performance Qualification (PQ)
Heat Distribution Study
Heat Penetration Study
Biological Indicator Validation
Temperature Mapping
Pressure Mapping
These validation activities confirm that the sterilizer consistently delivers the required sterilization conditions.
Construction Details
High-quality pharmaceutical sterilizers generally include:
SS 316L product contact surfaces
SS 304 external body
High-quality insulation
Automatic pneumatic valves
Sterile air filters
Steam control valves
Pressure sensors
RTD temperature sensors
Safety relief valves
Automatic door locking system
Control System
Modern pharmaceutical facilities demand intelligent automation.
The control system may include:
PLC controller
HMI touchscreen
Password protection
User access management
Batch reporting
Alarm history
Data export
Ethernet communication
SCADA integration
Audit trail
Comparison with Other Sterilization Technologies
Each sterilization technology has a specific application.
For dry products, glassware, and metal components, the Dry Heat Sterilizer is an excellent choice:
https://www.mediclaveindustries.in/dry-heat-sterilizer/
For rubber closures and pharmaceutical stoppers, manufacturers often use the Rubber Bung Processor Cum Steam Sterilizer:
https://www.mediclaveindustries.in/rubber-bung-processor-cum-steam-sterilizer/
For products requiring water spray sterilization, Mediclave Industries also offers the Super Heated Water Shower Sterilizer:
https://www.mediclaveindustries.in/super-heated-water-shower-sterilizer/
Each sterilization method is designed for different product characteristics, packaging materials, and manufacturing processes.
Maintenance Tips
Regular maintenance ensures long service life and reliable sterilization performance.
Recommended maintenance practices include:
Inspect steam pipelines regularly.
Check compressed air quality.
Replace air filters as scheduled.
Verify sensor calibration.
Inspect chamber gasket condition.
Test safety valves.
Clean the chamber after every batch.
Monitor pressure gauges.
Review PLC alarms.
Perform annual preventive maintenance.
Choosing the Right Steam + Air Mixture Sterilizer
Before purchasing a sterilizer, evaluate:
Chamber Capacity
Choose a size that matches production requirements.
Automation Level
Fully automatic systems reduce human error.
Validation Support
Ensure IQ, OQ, and PQ documentation is available.
Construction Quality
Prefer pharmaceutical-grade stainless steel construction.
Temperature Uniformity
Consistent temperature distribution improves product safety.
After-Sales Service
Reliable technical support reduces downtime.
Customization
The sterilizer should match your production layout and process requirements.
Why Pharmaceutical Manufacturers Prefer Mediclave Industries
Mediclave Industries Pvt. Ltd. designs and manufactures advanced pharmaceutical sterilization solutions that combine engineering excellence with reliable performance.
Our solutions offer:
High-quality manufacturing
GMP-compliant designs
Advanced automation
Customized chamber sizes
Validation-ready systems
Energy-efficient operation
Reliable technical support
Competitive pricing
Long operational life
Excellent service network
In addition to Steam + Air Mixture Sterilizers, we also manufacture pharmaceutical utility systems such as the Pure Steam Generator, which produces high-purity steam essential for pharmaceutical sterilization processes:
https://www.mediclaveindustries.in/pure-steam-generator/
For complete pharmaceutical water systems, manufacturers can integrate the Multi Column Distillation Plant:
https://www.mediclaveindustries.in/multi-column-distillation-plant/
Future Trends in Pharmaceutical Sterilization
The pharmaceutical industry continues to adopt smarter sterilization technologies.
Future systems are expected to include:
AI-assisted cycle optimization
Remote monitoring
Predictive maintenance
Advanced energy-saving controls
Digital batch records
Cloud connectivity
Enhanced validation software
Industry 4.0 integration
These innovations will further improve product safety, manufacturing efficiency, and regulatory compliance.
Frequently Asked Questions (FAQs)
What is a Steam + Air Mixture Sterilizer used for?
It is primarily used for sterilizing pharmaceutical liquids and sealed containers such as IV bottles, glass bottles, plastic containers, ampoules, and vials while maintaining product quality.
Why is compressed air added during sterilization?
Compressed sterile air balances chamber pressure, protects containers from damage, and ensures uniform heat distribution.
Is this sterilizer suitable for injectable products?
Yes. It is widely used for injectable medicines, IV fluids, ophthalmic products, vaccines, and other pharmaceutical liquids.
Can plastic containers be sterilized safely?
Yes. Controlled pressure prevents deformation, making it ideal for plastic bottles and IV bags.
Does the system support pharmaceutical validation?
Absolutely. It is designed to support IQ, OQ, PQ, heat distribution studies, and other validation protocols required by pharmaceutical manufacturers.
Conclusion
The Steam + Air Mixture Sterilizer has become an indispensable solution for modern pharmaceutical manufacturing because it delivers precise sterilization while protecting sensitive products and packaging. By combining saturated steam with sterile compressed air, it achieves exceptional temperature uniformity, controlled chamber pressure, and consistent sterilization results that meet the stringent expectations of global regulatory authorities.
Whether you manufacture injectables, IV fluids, ophthalmic solutions, vaccines, biologics, or other sterile pharmaceutical products, investing in a high-quality Steam + Air Mixture Sterilizer can significantly improve product safety, operational efficiency, and production reliability. With robust engineering, intelligent automation, validation-ready designs, and dependable after-sales support, Mediclave Industries Pvt. Ltd. provides sterilization solutions that help pharmaceutical manufacturers maintain the highest standards of quality while preparing for future growth.