
What Makes a Liquid Syrup Manufacturing Process Plant Essential for Modern Pharmaceutical Production?
The pharmaceutical industry is constantly evolving, and the demand for safe, consistent, and high-quality liquid medicines continues to grow. From cough syrups and pediatric medicines to vitamin formulations, antacids, herbal preparations, and nutraceutical liquids, many products require carefully controlled manufacturing processes to achieve the desired quality and consistency. This is where a Liquid Syrup Manufacturing Process Plant becomes an important part of a modern pharmaceutical production facility.
A liquid syrup manufacturing plant is not simply a large mixing tank. It is an integrated processing system designed to handle multiple stages of production, including purified water charging, sugar dissolution, ingredient mixing, heating, cooling, homogenization, filtration, storage, and product transfer. When these operations are properly integrated, pharmaceutical manufacturers can achieve better batch consistency, improved hygiene, reduced manual intervention, and more efficient production.
For manufacturers planning a new pharmaceutical facility or upgrading an existing production line, choosing the right processing equipment is an important investment decision. The plant must be designed around the product formulation, batch size, production capacity, cleaning requirements, material compatibility, automation level, and applicable GMP requirements.
Mediclave Industries Pvt. Ltd. designs and manufactures pharmaceutical process equipment for companies looking for reliable and hygienic production solutions. Its range includes liquid processing systems as well as equipment for other pharmaceutical manufacturing applications.
What Is a Liquid Syrup Manufacturing Process Plant?
A Liquid Syrup Manufacturing Process Plant is an integrated pharmaceutical processing system used to manufacture liquid formulations such as pharmaceutical syrups, oral solutions, oral suspensions, pediatric formulations, nutritional liquids, herbal syrups, vitamin preparations, and similar products.
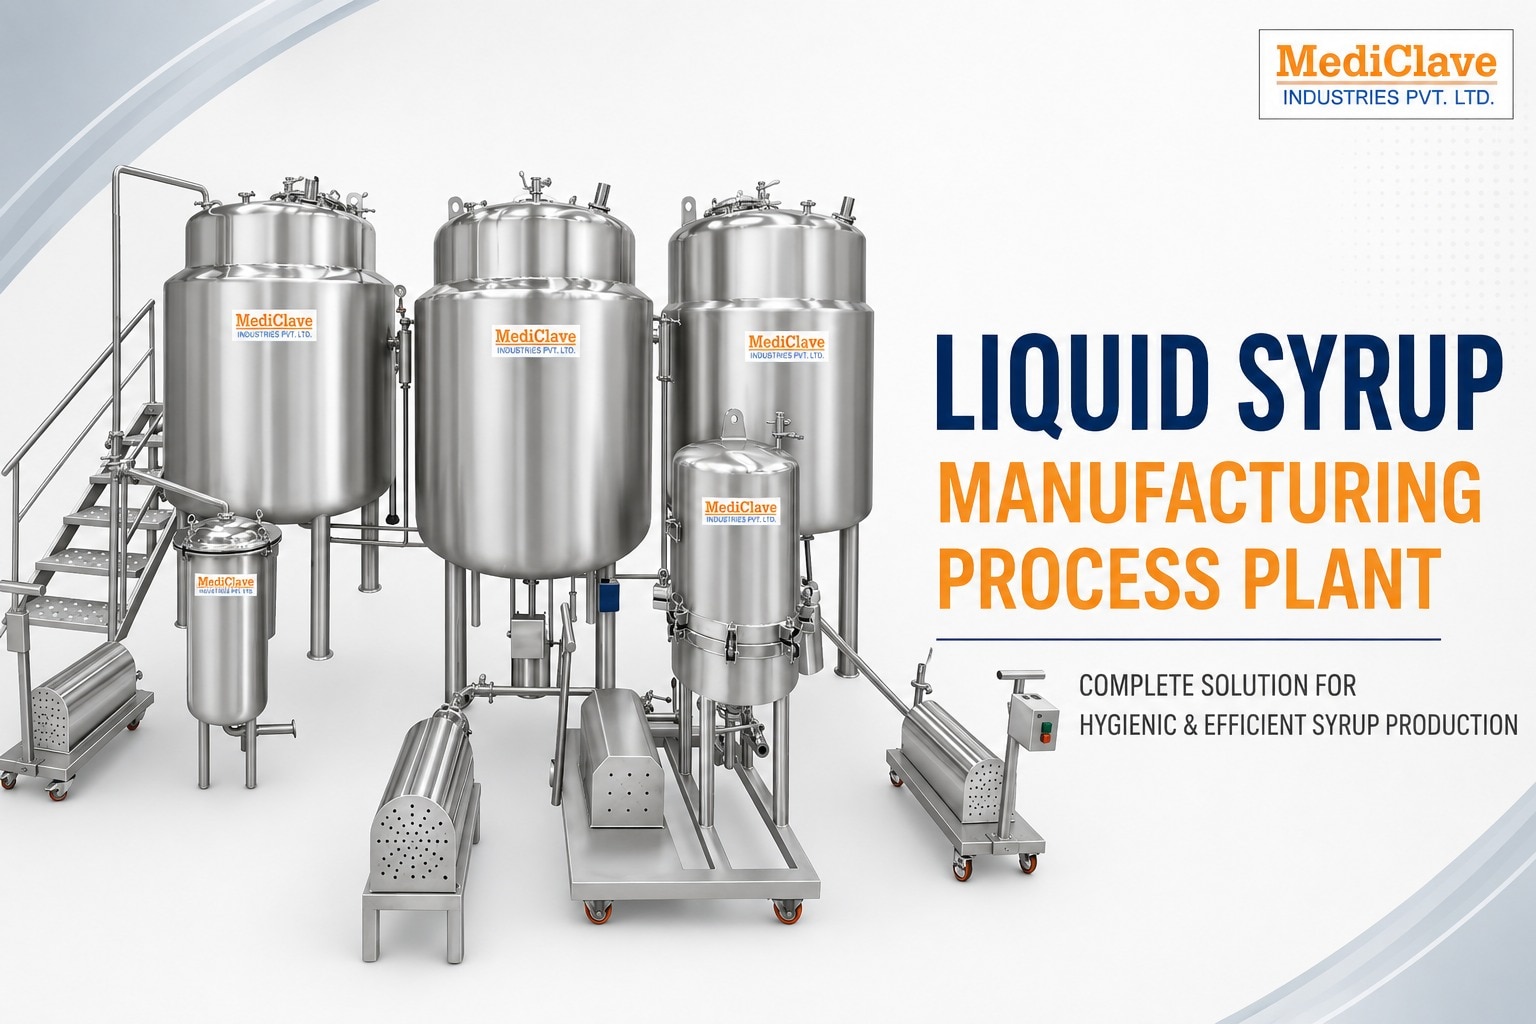
The plant generally combines several pieces of equipment into one coordinated production system. Depending on the formulation and production requirement, a typical system can include a sugar syrup preparation vessel, manufacturing vessel, storage vessel, agitator, transfer pumps, filtration system, heating and cooling arrangement, control panel, sanitary piping, and cleaning system.
The objective is to move the product smoothly from one manufacturing stage to another while maintaining controlled processing conditions.
A modern plant can also incorporate PLC and HMI-based automation. This allows operators to monitor important parameters such as temperature, mixing speed, process time, and other configured operating conditions.
For pharmaceutical manufacturers, this level of process control is valuable because consistency is one of the most important requirements in batch manufacturing.
Why Is a Syrup Manufacturing Plant Important?
Liquid pharmaceutical formulations can be more challenging to manufacture than they may initially appear. Ingredients must be properly dissolved or dispersed, the formulation must achieve the required consistency, and the finished product must be protected from contamination throughout processing.
Traditional manual processing can create several challenges. Different operators may use slightly different procedures, mixing may not be uniform, temperature control may be inconsistent, and transferring the product between vessels can increase handling.
A properly engineered Liquid Syrup Manufacturing Process Plant helps address these challenges by creating a controlled and repeatable manufacturing process.
The major benefits include:
Consistent batch-to-batch production
Better ingredient distribution
Controlled heating and cooling
Reduced manual handling
Improved production efficiency
Hygienic product processing
Easier cleaning and maintenance
Better process monitoring
Reduced risk of cross-contamination
Improved scalability for growing production requirements
For a pharmaceutical company, these benefits can directly contribute to smoother production operations and more reliable product quality.
How Does a Liquid Syrup Manufacturing Process Plant Work?
Although the exact process depends on the formulation, a typical syrup manufacturing operation follows a logical sequence.
1. Raw Material Preparation
The first stage involves preparing and verifying the raw materials required for the batch. Depending on the formulation, these may include purified water, sugar, active pharmaceutical ingredients, preservatives, flavors, colors, sweeteners, stabilizers, and other excipients.
Accurate weighing and controlled material handling are essential because even small variations can affect the final formulation.
2. Purified Water Charging
Purified water is introduced into the appropriate preparation or manufacturing vessel.
Water quality is particularly important in pharmaceutical production because water is often one of the largest components of a liquid formulation. The water system should therefore be selected according to the formulation and applicable quality requirements.
For pharmaceutical facilities that require high-purity water generation, Mediclave Industries also provides solutions within its pharmaceutical water systems range.
3. Sugar Syrup Preparation
For formulations containing sugar, the sugar is added to purified water and dissolved under controlled conditions.
A jacketed vessel can be used to provide controlled heating, while an agitator promotes uniform mixing. Proper temperature and agitation help achieve effective dissolution and a consistent syrup base.
The design of this stage can vary depending on the formulation, viscosity, batch size, and manufacturing process.
4. Ingredient Addition
Once the base solution has been prepared, the required ingredients are introduced according to the approved formulation.
These may include active pharmaceutical ingredients, preservatives, flavors, colors, sweeteners, stabilizers, or other excipients.
Controlled addition is important because certain ingredients may require specific mixing conditions or addition sequences.
5. Mixing and Homogenization
The manufacturing vessel plays a central role in this stage.
The agitator continuously mixes the formulation so that the ingredients are distributed uniformly throughout the batch. Depending on the product, additional homogenization may be required to achieve the desired consistency and stability.
Efficient agitation helps reduce variations within the batch and supports repeatable manufacturing.
6. Heating and Cooling
Some formulations require controlled heating to dissolve ingredients or facilitate processing. Others may require cooling before the next manufacturing stage.
Jacketed vessels can provide controlled heating and cooling by circulating an appropriate utility through the vessel jacket.
Accurate temperature monitoring helps operators maintain the required process conditions without unnecessary overheating or cooling.
7. Filtration
After mixing, the liquid may pass through a suitable filtration system.
Filtration can help remove unwanted particulate matter and improve the clarity and quality of the finished liquid, depending on the formulation and filtration strategy.
The filtration method should always be selected according to the product characteristics and validated manufacturing process.
8. Storage and Holding
Once processing is completed, the finished syrup may be transferred to a hygienic storage or holding vessel.
The storage vessel allows the product to remain under controlled conditions until it is ready for the next stage, such as filling and packaging.
Sanitary transfer pumps and appropriately designed pipelines help move the product between different stages while reducing unnecessary manual handling.
What Are the Main Components of a Liquid Syrup Manufacturing Plant?
A complete plant may contain several interconnected systems. The exact configuration depends on the customer's formulation and production requirements.
Sugar Syrup Preparation Vessel
The sugar syrup preparation vessel is used for dissolving sugar and preparing the syrup base. It may include heating, agitation, temperature monitoring, and other process controls.
Manufacturing Vessel
The manufacturing vessel is the primary processing unit where ingredients are mixed and the final formulation is developed.
It may include an agitator, jacket, temperature sensors, spray devices, load cells, and other customized features depending on the application.
Storage Vessel
Storage vessels provide hygienic holding capacity for prepared or finished products before filling or further processing.
Transfer Pumps
Sanitary transfer pumps help move liquid formulations from one vessel to another. Proper pump selection is important because syrup viscosity can vary considerably from one product to another.
Filtration System
The filtration system can be incorporated into the product transfer line to support the required filtration stage.
Control Panel
A modern control panel can provide centralized monitoring and control of important process parameters. PLC and HMI-based systems can also improve repeatability and simplify operator interaction.
Sanitary Piping
Product-contact pipelines should be designed with hygiene and cleanability in mind. Appropriate materials, surface finishes, drainage, and connections help support pharmaceutical manufacturing requirements.
CIP System
Cleaning is a major consideration in any pharmaceutical liquid manufacturing facility. A suitable Clean-In-Place system can reduce the need to dismantle equipment manually and can make cleaning operations more consistent.
Mediclave Industries provides a dedicated CIP & SIP System designed for automated cleaning and sterilization applications in pharmaceutical and other hygienic processing environments.
Why Is Stainless Steel Important in Pharmaceutical Syrup Production?
Material selection is an important part of pharmaceutical equipment design.
Product-contact surfaces are commonly manufactured using pharmaceutical-grade stainless steel such as SS316L because it offers good corrosion resistance, durability, cleanability, and compatibility with many pharmaceutical processing applications.
The internal surface finish is also important. Smooth and hygienic surfaces can make cleaning easier and reduce areas where product residues could accumulate.
The exact material grade, surface finish, welding requirements, and design specifications should be selected according to the product formulation, cleaning chemicals, temperature, regulatory requirements, and customer specifications.
How Does Automation Improve Syrup Manufacturing?
Automation has become an important feature of modern pharmaceutical manufacturing.
A PLC and HMI-based system can allow operators to monitor and control selected process parameters from a centralized interface. Depending on the system configuration, automation may be used for temperature control, agitator operation, pump operation, process timing, valve operation, and alarm monitoring.
Automation offers several advantages.
First, it can reduce unnecessary manual intervention. Second, it can improve process repeatability. Third, it can make it easier for operators to monitor the production cycle.
Automation can also help pharmaceutical manufacturers establish more standardized operating procedures, particularly when multiple batches are produced regularly.
The appropriate level of automation depends on the size of the facility, production volume, process complexity, budget, and documentation requirements.
What Products Can Be Manufactured Using a Syrup Manufacturing Plant?
One of the major advantages of a properly designed liquid processing plant is its versatility.
Depending on the equipment configuration and validated formulation, applications can include:
Cough syrups
Pediatric syrups
Antacid formulations
Vitamin syrups
Iron supplements
Nutraceutical liquids
Herbal syrups
Ayurvedic liquid formulations
Oral solutions
Oral suspensions
Health tonics
Flavored pharmaceutical liquids
Other liquid healthcare formulations
The plant should always be designed around the actual products that the manufacturer intends to produce.
For example, a low-viscosity oral solution may require different mixing and transfer characteristics than a highly viscous syrup or suspension.
How Should You Choose the Right Syrup Manufacturing Plant?
Selecting equipment only on the basis of tank capacity is not enough.
Before finalizing a Liquid Syrup Manufacturing Process Plant, manufacturers should consider several factors.
Production Capacity
Determine the required batch size and expected number of batches per day. This helps establish the appropriate vessel capacities and supporting equipment.
Product Characteristics
Viscosity, density, ingredients, sensitivity to temperature, and mixing requirements all influence equipment design.
Mixing Requirements
Different products require different agitation arrangements. The agitator should be selected according to the product characteristics and desired mixing performance.
Heating and Cooling Requirements
If the formulation requires heating or cooling, the vessel jacket and utility requirements should be designed accordingly.
Cleaning Requirements
Cleaning should be considered from the beginning rather than after installation. Hygienic vessel geometry, sanitary piping, drainability, and CIP compatibility can make routine cleaning easier.
Automation Level
Determine whether the facility needs manual, semi-automatic, or fully automated operation.
Future Expansion
A pharmaceutical company may start with one production capacity and expand later. Designing the plant with future production requirements in mind can help reduce the cost and disruption of future upgrades.
How Does a Syrup Plant Fit Into a Larger Pharmaceutical Facility?
A Liquid Syrup Manufacturing Process Plant is often only one part of a complete pharmaceutical production facility.
A company producing multiple dosage forms may require different process equipment for different products.
For example, manufacturers producing creams, ointments, gels, or other semi-solid products may require a specialized Ointment Manufacturing Plant.
Similarly, companies manufacturing sterile injectable formulations require specialized equipment designed for much more stringent sterile processing requirements. Mediclave Industries offers an Injectable Liquid Manufacturing Vessel with Magnetic Stirrer for applications involving injectable liquid manufacturing.
This type of equipment should not be treated as interchangeable with an ordinary syrup processing vessel. Injectable production requires specialized hygienic and sterile-processing considerations.
Why Are Cleaning and Sterilization Important?
Pharmaceutical production equipment comes into contact with raw materials and finished products repeatedly. If residues are not properly removed, they can affect subsequent batches and create contamination risks.
This is why cleaning system design is an important consideration when purchasing a liquid manufacturing plant.
A properly configured CIP system can circulate cleaning solutions through vessels and pipelines without requiring complete dismantling of the equipment.
For applications where sterilization is required, SIP can also be integrated into the overall system.
The Mediclave Industries CIP & SIP System provides an integrated approach to cleaning and sterilization for suitable pharmaceutical processing applications.
The actual cleaning and sterilization cycle should be established and validated according to the specific equipment, formulation, cleaning agents, process requirements, and applicable regulations.
What Role Does Water Quality Play in Syrup Manufacturing?
Water is one of the most important raw materials in many liquid pharmaceutical formulations.
Poor-quality process water can negatively affect the manufacturing process and potentially compromise the final product. Therefore, pharmaceutical manufacturers need to establish appropriate water-quality controls based on their product and regulatory requirements.
A complete pharmaceutical facility may include specialized water treatment and purification equipment alongside its process equipment.
Mediclave Industries' pharmaceutical process portfolio includes water-system solutions such as multi-column distillation technology and other pharmaceutical water-related equipment. This allows manufacturers to consider their process equipment and utility requirements as part of a broader pharmaceutical manufacturing setup.
Why Is GMP-Oriented Design Important?
Good Manufacturing Practice, commonly referred to as GMP, focuses on ensuring that pharmaceutical products are consistently produced and controlled according to appropriate quality standards.
Equipment design is an important part of this approach.
A GMP-oriented liquid manufacturing plant should consider:
Hygienic construction
Appropriate product-contact materials
Smooth and cleanable surfaces
Proper drainage
Suitable sanitary connections
Controlled processing conditions
Cleaning procedures
Maintenance access
Process monitoring
Documentation and validation requirements where applicable
It is important to remember that equipment being described as “GMP compliant” does not automatically make an entire manufacturing facility GMP compliant. Compliance depends on the complete facility, processes, utilities, procedures, documentation, qualification, validation, and applicable regulatory requirements.
What Are the Benefits of Working With an Experienced Manufacturer?
A pharmaceutical processing plant is a long-term investment. The equipment must not only work correctly on the day it is installed but also support reliable production over many years.
An experienced equipment manufacturer can help customers evaluate vessel capacity, process requirements, material selection, agitation, heating and cooling, automation, piping, cleaning, and other technical requirements before manufacturing begins.
This engineering approach is particularly important when a customer requires a customized plant rather than a standard machine.
Mediclave Industries Pvt. Ltd. focuses on pharmaceutical process equipment and provides solutions for liquid, semi-solid, sterile, and pharmaceutical utility applications. Its product range includes liquid syrup manufacturing systems, ointment manufacturing plants, injectable manufacturing vessels, CIP & SIP systems, and pharmaceutical water-system equipment.
Why Choose Mediclave Industries for a Liquid Syrup Manufacturing Process Plant?
Choosing the right supplier is just as important as choosing the right equipment.
Mediclave Industries develops pharmaceutical processing equipment with a focus on hygienic construction, controlled processing, customization, and practical production requirements.
A Liquid Syrup Manufacturing Process Plant from an experienced manufacturer can be configured according to the customer's required batch capacity, product characteristics, automation level, utility availability, and production workflow.
The goal is not simply to supply a vessel or a collection of machines. The goal is to create a coordinated processing system that can support reliable pharmaceutical production.
For companies expanding their production capacity, setting up a new pharmaceutical facility, or upgrading an existing manufacturing line, customized process equipment can provide a practical path toward improved productivity and process consistency.
Conclusion
A Liquid Syrup Manufacturing Process Plant is an essential part of modern pharmaceutical liquid production. It brings together controlled mixing, heating, cooling, filtration, storage, transfer, and cleaning operations to create a more consistent and hygienic manufacturing process.
From cough syrups and pediatric formulations to nutraceutical liquids and herbal preparations, different products require different processing conditions. That is why plant design should always begin with the formulation, production capacity, cleaning requirements, material compatibility, and future manufacturing plans.
The right plant can help reduce manual handling, improve batch consistency, increase production efficiency, simplify cleaning, and provide better control over important manufacturing parameters.
For pharmaceutical manufacturers looking for a reliable and customizable solution, Mediclave Industries Pvt. Ltd. offers pharmaceutical process equipment designed around modern manufacturing requirements. Its solutions can also be integrated with related equipment such as an Ointment Manufacturing Plant, Injectable Liquid Manufacturing Vessel, and CIP & SIP System, depending on the manufacturing facility's requirements.
Ultimately, investing in a well-engineered Liquid Syrup Manufacturing Process Plant is not just about increasing production capacity. It is about building a controlled, hygienic, efficient, and scalable manufacturing process that can support consistent product quality as the pharmaceutical business grows.
