
The Complete Guide to Liquid Syrup Manufacturing Process Plants for Modern Pharmaceutical Production
The pharmaceutical industry depends on precision, hygiene, and consistency to manufacture safe and effective medicines. Among the most widely used dosage forms, liquid syrups hold a special place because they are easy to consume, especially for children, elderly patients, and individuals who have difficulty swallowing tablets or capsules. However, producing high-quality liquid syrups requires much more than simply mixing ingredients together. Every stage, from water preparation to ingredient blending, filtration, storage, and filling, must be carried out under strict quality standards.
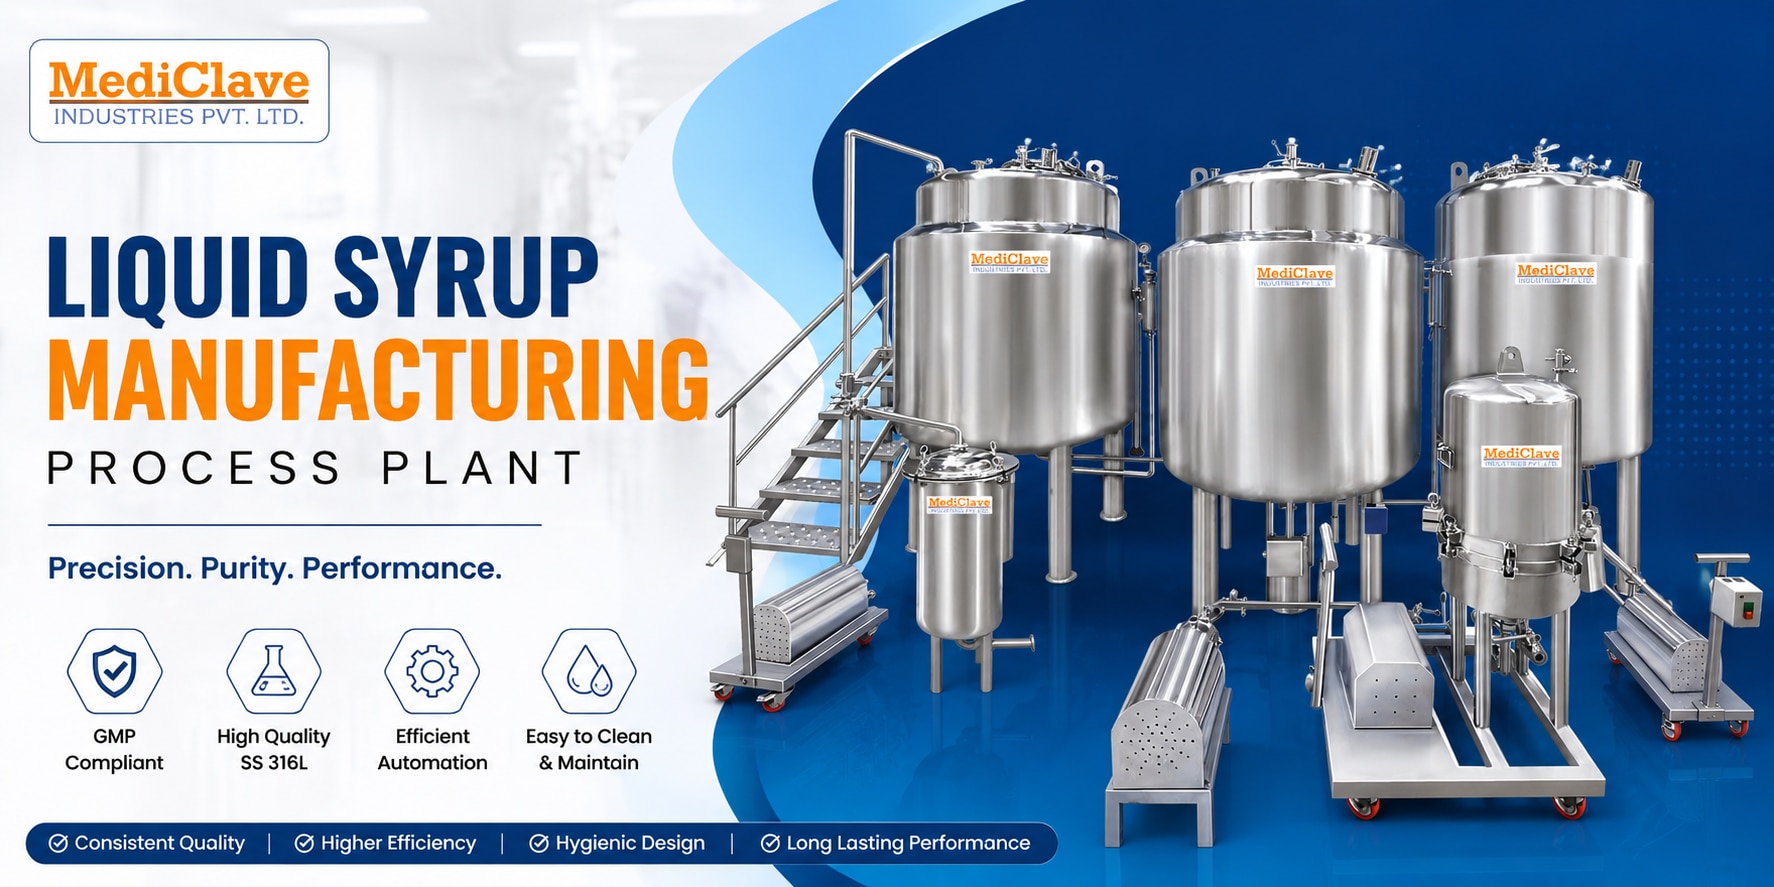
This is where a Liquid Syrup Manufacturing Process Plant becomes an essential part of pharmaceutical manufacturing. A modern manufacturing plant is designed to ensure accurate formulation, hygienic processing, efficient production, and compliance with GMP guidelines. Whether you are establishing a new pharmaceutical facility or upgrading an existing production line, investing in the right manufacturing system improves product quality while reducing operational costs.
At Mediclave Industries Pvt. Ltd., we specialize in manufacturing advanced pharmaceutical process equipment designed to meet the needs of modern pharmaceutical industries. Our Liquid Syrup Manufacturing Process Plant combines innovative engineering, high-quality stainless steel construction, and intelligent automation to deliver reliable and consistent production performance.
In this complete guide, you will learn everything about Liquid Syrup Manufacturing Process Plants, including their working principle, components, benefits, applications, selection criteria, maintenance practices, and why Mediclave Industries is the preferred manufacturing partner for pharmaceutical companies.
What is a Liquid Syrup Manufacturing Process Plant?
A Liquid Syrup Manufacturing Process Plant is an integrated pharmaceutical processing system used to manufacture oral liquid medicines such as syrups, suspensions, medicated solutions, herbal syrups, vitamin syrups, cough syrups, pediatric formulations, and nutraceutical liquids.
The plant combines multiple processing operations into one efficient production system, including:
- Water preparation
- Sugar syrup preparation
- Ingredient mixing
- Heating and cooling
- Homogenization
- Filtration
- Storage
- Transfer to filling machines
Modern plants are designed to maintain product quality while minimizing contamination risks through closed-loop processing systems.
Why Pharmaceutical Companies Need Advanced Syrup Manufacturing Plants
Liquid medicines require precise manufacturing because even small formulation errors can affect product stability, taste, effectiveness, and shelf life.
Modern pharmaceutical companies require equipment capable of maintaining:
- Accurate ingredient proportions
- Uniform mixing
- Controlled temperatures
- Hygienic production
- Batch repeatability
- Regulatory compliance
- Minimal product loss
- Efficient cleaning procedures
A professionally designed manufacturing process plant ensures every production batch maintains identical quality standards.
Main Components of a Liquid Syrup Manufacturing Process Plant
A complete syrup manufacturing system consists of several interconnected units working together.
1. Sugar Syrup Preparation Vessel
The sugar syrup preparation vessel dissolves sugar in purified water under controlled heating conditions. Proper agitation ensures complete dissolution without burning or caramelization.
2. Manufacturing Vessel
The manufacturing vessel is where active pharmaceutical ingredients (APIs), preservatives, colors, flavors, stabilizers, and other ingredients are mixed with the prepared sugar syrup.
The vessel includes:
- Variable speed agitator
- Bottom homogenizer
- Heating jacket
- Cooling jacket
- Temperature monitoring
- Level indicators
3. Storage Vessel
After manufacturing, the finished syrup is transferred into a storage vessel before filling operations.
Storage vessels maintain product quality by protecting the formulation from contamination.
4. Transfer Pump
Sanitary transfer pumps move the product between vessels without affecting the formulation.
5. Filtration System
Filtration removes unwanted particles while maintaining product clarity.
6. Control Panel
Modern PLC-based control panels automate production parameters including:
- Mixing speed
- Heating
- Cooling
- Batch timing
- Temperature control
- Pump operation
Automation minimizes operator errors and improves production consistency.
Working Process of a Liquid Syrup Manufacturing Plant
The production process follows a carefully controlled sequence.
Step 1: Purified Water Preparation
High-quality purified water forms the foundation of every pharmaceutical syrup.
Mediclave Industries also manufactures advanced Pure Steam Generators and pharmaceutical water systems that help pharmaceutical manufacturers maintain sterile production environments. Learn more about our Pure Steam Generator here:
https://www.mediclaveindustries.in/product/pure-steam-generator/
Step 2: Sugar Syrup Preparation
Sugar is dissolved in purified water under controlled temperature conditions.
The syrup is continuously mixed until a clear solution is obtained.
Step 3: Ingredient Addition
APIs, preservatives, sweeteners, colors, and flavors are gradually added while maintaining constant agitation.
Step 4: Homogenization
Homogenization ensures all ingredients are evenly dispersed throughout the solution.
This process improves:
- Uniformity
- Stability
- Product appearance
- Shelf life
Step 5: Cooling
The syrup is cooled to the required filling temperature.
Controlled cooling prevents ingredient degradation.
Step 6: Filtration
The finished syrup passes through pharmaceutical-grade filters to remove fine particles.
Step 7: Storage
The filtered syrup is transferred into a sterile storage vessel.
Step 8: Filling
The syrup is then transferred to the filling machine for bottle filling and packaging.
Key Features of Mediclave Liquid Syrup Manufacturing Process Plant
Mediclave Industries designs every system according to pharmaceutical industry requirements.
Major features include:
- SS 316L product contact parts
- SS 304 external structure
- GMP-compliant design
- CIP compatible construction
- Closed processing system
- Mirror-finished surfaces
- Variable speed agitator
- Bottom homogenizer
- PLC automation
- Easy maintenance
- Low operating cost
- High production efficiency
- Batch consistency
- Energy-efficient operation
- Long equipment life
Applications of Liquid Syrup Manufacturing Process Plants
These systems are widely used for manufacturing:
- Cough syrups
- Pediatric syrups
- Vitamin syrups
- Iron tonics
- Herbal syrups
- Ayurvedic formulations
- Nutraceutical syrups
- Antacid syrups
- Antihistamine syrups
- Multivitamin liquids
- Digestive syrups
- Pharmaceutical suspensions
- Oral solutions
Benefits of Using an Automated Manufacturing Plant
Superior Product Quality
Automation minimizes manual errors and ensures consistent product quality.
Faster Production
Integrated processing significantly reduces production time.
Better Hygiene
Closed systems reduce contamination risks.
Regulatory Compliance
Modern pharmaceutical plants are designed according to GMP requirements.
Reduced Product Loss
Efficient transfer systems minimize wastage.
Improved Cleaning
CIP-compatible systems reduce downtime between production batches.
Importance of Pharmaceutical Water Systems
Water quality directly affects syrup quality.
Pharmaceutical manufacturers often combine syrup plants with advanced water purification systems like the Multi Column Distillation Plant.
Learn more:
https://www.mediclaveindustries.in/product/multi-column-distillation-plant/
High-quality water improves:
- Product stability
- Taste
- Purity
- Shelf life
- Regulatory compliance
Integration with CIP & SIP Systems
Cleaning is one of the most critical aspects of pharmaceutical manufacturing.
Modern syrup plants are often integrated with CIP & SIP Systems for automatic cleaning and sterilization.
Discover our solution:
https://www.mediclaveindustries.in/product/cip-sip-system/
Benefits include:
- Reduced contamination
- Faster cleaning
- Lower labor requirements
- Consistent hygiene
- Reduced downtime
Importance of Sterilization Before Manufacturing
Before manufacturing liquid medicines, many pharmaceutical facilities sterilize equipment using advanced sterilization systems.
Mediclave Industries manufactures Saturated Steam Sterilizers (Autoclaves) that provide reliable sterilization for pharmaceutical equipment.
Product information:
https://www.mediclaveindustries.in/product/saturated-steam-sterilizer/
Proper sterilization improves:
- Product safety
- Equipment cleanliness
- Regulatory compliance
- Production reliability
Manufacturing Other Pharmaceutical Products
Many pharmaceutical companies manufacture multiple dosage forms under one facility.
Besides syrup plants, Mediclave Industries also manufactures advanced Cream Manufacturing Plants for ointments, creams, gels, and toothpaste production.
Explore the product:
https://www.mediclaveindustries.in/product/cream-manufacturing-plant/
Having multiple pharmaceutical processing solutions from a single manufacturer ensures compatibility, easier maintenance, and streamlined support.
Factors to Consider Before Buying a Liquid Syrup Manufacturing Process Plant
Choosing the right equipment requires careful evaluation.
Consider the following factors:
Production Capacity
Select a plant that matches your current production while allowing future expansion.
Material of Construction
Product contact parts should be manufactured from SS 316L stainless steel.
Automation Level
PLC-based automation improves efficiency and repeatability.
GMP Compliance
Always choose equipment manufactured according to pharmaceutical standards.
Cleaning System
CIP compatibility reduces downtime.
Technical Support
Reliable after-sales service ensures uninterrupted production.
Customization
Every pharmaceutical company has unique production requirements.
Choose a manufacturer capable of providing customized solutions.
Maintenance Tips
Proper maintenance increases equipment lifespan.
Recommended practices include:
- Clean equipment after every production batch.
- Inspect gaskets regularly.
- Lubricate moving parts according to schedule.
- Calibrate temperature sensors periodically.
- Check agitator alignment.
- Monitor pumps for unusual noise.
- Inspect pipelines for leakage.
- Validate cleaning procedures.
- Replace worn seals promptly.
- Maintain proper maintenance records.
Preventive maintenance reduces unexpected breakdowns.
Why Choose Mediclave Industries?
Mediclave Industries Pvt. Ltd. has established itself as a trusted manufacturer of pharmaceutical process equipment through quality engineering and customer-focused solutions.
Customers choose Mediclave because of:
- Years of manufacturing expertise
- Advanced engineering
- GMP-compliant equipment
- Premium stainless steel construction
- Customized solutions
- Competitive pricing
- Reliable technical support
- Nationwide service
- Modern manufacturing facilities
- Commitment to innovation
- Timely project execution
Every Liquid Syrup Manufacturing Process Plant is manufactured with strict quality control to ensure dependable long-term performance.
Future Trends in Syrup Manufacturing
The pharmaceutical industry continues to evolve with increasing demand for automation and digital manufacturing.
Future-ready syrup plants are expected to include:
- Smart PLC automation
- Industry 4.0 integration
- Remote monitoring
- Energy-efficient operation
- Automatic batch recording
- Digital maintenance alerts
- Improved product traceability
- Enhanced process validation
- Sustainable manufacturing practices
Manufacturers investing in advanced technology today will be better prepared to meet future regulatory and market requirements.
Conclusion
A Liquid Syrup Manufacturing Process Plant is much more than a mixing system—it is the heart of pharmaceutical liquid production. From preparing purified water and dissolving sugar to blending ingredients, homogenizing formulations, filtering, storing, and transferring finished products for filling, every stage demands precision, hygiene, and consistency. A well-designed manufacturing plant helps pharmaceutical companies produce high-quality syrups while reducing production time, minimizing contamination risks, and ensuring compliance with GMP standards.
Mediclave Industries Pvt. Ltd. offers reliable, high-performance Liquid Syrup Manufacturing Process Plants that are engineered to meet the evolving needs of pharmaceutical manufacturers. Combined with complementary solutions such as Pure Steam Generators, Multi Column Distillation Plants, CIP & SIP Systems, Saturated Steam Sterilizers, and Cream Manufacturing Plants, Mediclave provides complete pharmaceutical processing solutions under one roof.
Whether you are setting up a new production facility, expanding your manufacturing capacity, or modernizing your existing plant, choosing a trusted equipment manufacturer is a critical investment. With advanced engineering, premium-quality materials, customizable designs, and dedicated technical support, Mediclave Industries helps pharmaceutical companies achieve efficient, hygienic, and reliable production.
If you are looking for a dependable Liquid Syrup Manufacturing Process Plant that delivers consistent performance, long service life, and excellent manufacturing efficiency, Mediclave Industries is your trusted partner for complete pharmaceutical processing solutions.
