Ahmedabad
08042755106
+917041232204
Pharma - Process Equipment by Mediclave Industries

Liquid Syrup Manufacturing Process Plant

In stock•cod not available

Subcategory Tags

Liquid Syrup Manufacturing Process Plant Manufacturer in Maharastra Liquid Syrup Manufacturing Process Plant Manufacturer in Mumbai Liquid Syrup Manufacturing Process Plant Manufacturer in Pune Liquid Syrup Manufacturing Process Plant Manufacturer in Navi Mumbai Liquid Syrup Manufacturing Process Plant Manufacturer in Nagpur Liquid Syrup Manufacturing Process Plant Manufacturer in Uttar Pradesh Liquid Syrup Manufacturing Process Plant Manufacturer in Lucknow Liquid Syrup Manufacturing Process Plant Manufacturer in Noida Liquid Syrup Manufacturing Process Plant Manufacturer in Agra Liquid Syrup Manufacturing Process Plant Manufacturer in Karnataka Liquid Syrup Manufacturing Process Plant Manufacturer in Bengaluru Liquid Syrup Manufacturing Process Plant Manufacturer in Mysuru Liquid Syrup Manufacturing Process Plant Manufacturer in Mangalore Liquid Syrup Manufacturing Process Plant Manufacturer in Hubli-Dharwad Liquid Syrup Manufacturing Process Plant Manufacturer in Tamilnadu Liquid Syrup Manufacturing Process Plant Manufacturer in Chennai Liquid Syrup Manufacturing Process Plant Manufacturer in Coimbatore Liquid Syrup Manufacturing Process Plant Manufacturer in Madurai Liquid Syrup Manufacturing Process Plant Manufacturer in West Bengal Liquid Syrup Manufacturing Process Plant Manufacturer in Kolkata Liquid Syrup Manufacturing Process Plant Manufacturer in Siliguri Liquid Syrup Manufacturing Process Plant Manufacturer in Kharagpur Liquid Syrup Manufacturing Process Plant Manufacturer in Gujarat Liquid Syrup Manufacturing Process Plant Manufacturer in Ahmedabad Liquid Syrup Manufacturing Process Plant Manufacturer in Surat Liquid Syrup Manufacturing Process Plant Manufacturer in Vadodara Liquid Syrup Manufacturing Process Plant Manufacturer in Rajkot Liquid Syrup Manufacturing Process Plant Manufacturer in Gandhinagar Liquid Syrup Manufacturing Process Plant Manufacturer in Madhya Pradesh Liquid Syrup Manufacturing Process Plant Manufacturer in Indore Liquid Syrup Manufacturing Process Plant Manufacturer in Bhopal Liquid Syrup Manufacturing Process Plant Manufacturer in Jabalpur Liquid Syrup Manufacturing Process Plant Manufacturer in Gwalior Liquid Syrup Manufacturing Process Plant Manufacturer in Ujjain Liquid Syrup Manufacturing Process Plant Manufacturer in Rajasthan Liquid Syrup Manufacturing Process Plant Manufacturer in Bihar Liquid Syrup Manufacturing Process Plant Manufacturer in Patna Liquid Syrup Manufacturing Process Plant Manufacturer in Muzaffarpur Liquid Syrup Manufacturing Process Plant Manufacturer in Bhubaneshwar Liquid Syrup Manufacturing Process Plant Manufacturer in Manali Liquid Syrup Manufacturing Process Plant Manufacturer in Solan Liquid Syrup Manufacturing Process Plant Manufacturer in Kullu "Liquid Syrup Manufacturing Process Plant Manufacturer in Amritsar " Liquid Syrup Manufacturing Process Plant Manufacturer in Ludhiana Liquid Syrup Manufacturing Process Plant Manufacturer in Bathinda "Liquid Syrup Manufacturing Process Plant Manufacturer in Rishikesh " Liquid Syrup Manufacturing Process Plant Manufacturer in Nainital Liquid Syrup Manufacturing Process Plant Manufacturer in Roorkee Liquid Syrup Manufacturing Process Plant Manufacturer in Ambala Liquid Syrup Manufacturing Process Plant Manufacturer in Yamunanagar Liquid Syrup Manufacturing Process Plant Manufacturer in Pune Liquid Syrup Manufacturing Process Plant Manufacturer in Nashik Liquid Syrup Manufacturing Process Plant Manufacturer in Thane Liquid Syrup Manufacturing Process Plant Manufacturer in Amravati Liquid Syrup Manufacturing Process Plant Manufacturer in GOA Liquid Syrup Manufacturing Process Plant Manufacturer in Sagar Liquid Syrup Manufacturing Process Plant Manufacturer in Rewa Liquid Syrup Manufacturing Process Plant Manufacturer in Satna Liquid Syrup Manufacturing Process Plant Manufacturer in BIHAR Liquid Syrup Manufacturing Process Plant Manufacturer in Darbhanga Liquid Syrup Manufacturing Process Plant Manufacturer in Jamshedpur Liquid Syrup Manufacturing Process Plant Manufacturer in Khammam Liquid Syrup Manufacturing Process Plant Manufacturer in ANDHRA PRADESH Liquid Syrup Manufacturing Process Plant Manufacturer in TELANGANA KARANATAKA Liquid Syrup Manufacturing Process Plant Manufacturer in Visakhapatnam Liquid Syrup Manufacturing Process Plant Manufacturer in Vijayawada Liquid Syrup Manufacturing Process Plant Manufacturer in Kadapa Liquid Syrup Manufacturing Process Plant Manufacturer in Mysuru Liquid Syrup Manufacturing Process Plant Manufacturer in TAMILNADU Liquid Syrup Manufacturing Process Plant Manufacturer in Coimbatore Liquid Syrup Manufacturing Process Plant Manufacturer in Madurai Liquid Syrup Manufacturing Process Plant Manufacturer in kerala Liquid Syrup Manufacturing Process Plant Manufacturer in ODISHA Liquid Syrup Manufacturing Process Plant Manufacturer in Cuttack Liquid Syrup Manufacturing Process Plant Manufacturer in SIKKIM Liquid Syrup Manufacturing Process Plant Manufacturer in New Delhi Liquid Syrup Manufacturing Process Plant Manufacturer in Old Delhi Liquid Syrup Manufacturing Process Plant Manufacturer in South Delhi Liquid Syrup Manufacturing Process Plant Manufacturer in North Delhi Liquid Syrup Manufacturing Process Plant Manufacturer in East Delhi Liquid Syrup Manufacturing Process Plant Manufacturer in West Delhi Liquid Syrup Manufacturing Process Plant Manufacturer in Central Delhi
Phone Number

08042755106

Please keep 0 before dialling the number.

Mon-Thu: 10 AM - 2 PM • Fri: 3 PM - 7AM

Other Website Visit our other website
Address 418, 4th Floor , Arth Business Center (ABC , Galaxy Heights, Nikol

Ahmedabad, India, 382415

Description

Liquid Syrup Manufacturing Process Plant – Description A Liquid Syrup Manufacturing Process Plant is a fully integrated system designed for the hygienic and efficient production of pharmaceutical syrups, oral liquids, and suspensions. The plant ensures accurate mixing, uniform consistency, and contamination-free processing, meeting stringent cGMP and regulatory requirements. Our syrup manufacturing plants are engineered with precision using high-grade stainless steel and advanced automation to deliver reliable and repeatable batch production. The system typically includes sugar melting vessels, manufacturing tanks, filtration units, storage tanks, and transfer systems, all interconnected for smooth and controlled operations. The process begins with the preparation of sugar syrup, followed by the addition of active ingredients and excipients under controlled conditions. Homogeneous mixing is achieved using specially designed stirrers, ensuring uniformity in every batch. The final product is filtered and transferred hygienically for filling and packaging. Designed for ease of operation, cleaning, and maintenance, our plants are ideal for pharmaceutical companies seeking high productivity, quality assurance, and regulatory compliance. Key Features > Complete integrated system for syrup manufacturing > cGMP-compliant design with hygienic construction > SS 316L contact parts for product safety > Uniform mixing with advanced agitator design > Closed system to prevent contamination > PLC-based automation for process control (optional) > Easy cleaning with CIP (Clean-In-Place) system > Energy-efficient and user-friendly operation Applications > Pharmaceutical syrup production > Oral liquid formulations > Nutraceutical and herbal syrups > Veterinary liquid medicines > Food and beverage liquid processing

Type Liquid Syrup Manufacturing Process Plant
Application Pharmaceutical, Nutraceutical, Healthcare Industries
Product Range Syrups, Suspensions, Oral Liquids
Batch Capacity 100 Liters to 10,000+ Liters (Customizable)
Main Equipment Sugar Syrup Vessel, Manufacturing Vessel, Storage Vessel
Material of Construction SS 316 / SS 316L (Product Contact Parts), SS 304 (Non-contact Parts)
Design Standard GMP / cGMP Compliant Design
Mixing System Variable Speed Agitator (Anchor / Propeller Type)
Homogenization Inline / Bottom Homogenizer (Optional)
Heating System Steam Jacketed Vessel / Electrical Heating
Cooling System Chilled Water Circulation
Filtration System Multi-stage Filtration (Sparkler / Cartridge Filter)
Transfer System Sanitary Transfer Pump (Centrifugal / Lobe Pump)
Piping & Valves SS 316L with Tri-Clamp / TC Fittings
Control System PLC Based with HMI Touchscreen
Operation Mode Fully Automatic / Semi-Automatic
Temperature Range Ambient to 120°C
Vacuum System Optional (for deaeration)
CIP System Optional (Fully Automatic CIP System)
Safety Features Overload Protection, Dry Run Protection, Emergency Stop
Monitoring System Digital Display for Temperature, RPM & Process Parameters
Data Logging SCADA / USB / Printer (Optional)
Power Supply 415 V, 3 Phase, 50 Hz
Surface Finish Mirror Finish Internal (Ra < 0.8 µm), Matt Finish External
Accessories Storage Tanks, Working Platform, Flow Meters
Installation Skid Mounted / Floor Mounted
Compliance GMP / WHO-GMP / FDA (Optional)

Keywords

Other Products

view all
product image
Pharma - Sterilization

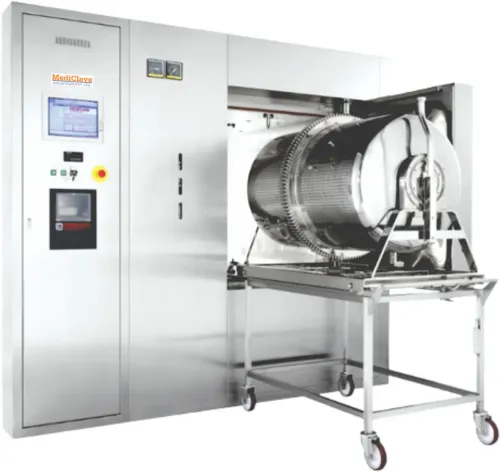
In pharmaceutical manufacturing, maintaining product quality and sterility is essential. Sterilization equipment plays a critical role in ensuring that products, containers, and other components are processed under controlled and validated conditions. One advanced solution used for this purpose is the Super Heated Water Shower Sterilizer. A Super Heated Water Shower Sterilizer is designed to sterilize heat-sensitive and liquid-filled products using circulating super-heated water under controlled pressure and temperature. The system provides uniform heat distribution and helps minimize the risk of thermal damage while achieving effective sterilization. • What Is a Super Heated Water Shower Sterilizer? A Super Heated Water Shower Sterilizer is a pharmaceutical sterilization system that uses heated water as the sterilizing medium. During the sterilization cycle, hot water is continuously circulated and sprayed or showered over the load inside the sterilization chamber. Unlike conventional steam sterilization, this technology can be particularly useful for sealed containers, liquid products, bottles, vials, and other pharmaceutical products where direct steam contact may not be desirable. The system operates with controlled temperature, pressure, circulation, and cooling parameters to provide consistent and reproducible sterilization cycles. • How Does a Super Heated Water Shower Sterilizer Work? The sterilization process generally involves several controlled stages. 1. Loading The products or containers to be sterilized are loaded into the chamber using suitable trays, baskets, or loading systems. 2. Heating Water is heated to the required sterilization temperature using an efficient heating arrangement. The heated water is then circulated through the chamber. 3. Water Showering and Circulation A powerful circulation system distributes hot water uniformly throughout the chamber. The continuous showering action helps ensure that all surfaces of the load receive consistent heat exposure. 4. Sterilization Holding Once the required temperature is achieved, the system maintains the programmed temperature for a specified holding time. This controlled exposure helps achieve the required microbial reduction. 5. Cooling After the sterilization stage, the product is gradually cooled under controlled conditions. Proper cooling helps protect containers and products from thermal shock and pressure-related damage. 6. Cycle Completion Once the programmed cycle parameters are completed, the chamber returns to safe conditions and the sterilized load can be unloaded according to the validated operating procedure. • Key Features of Super Heated Water Shower Sterilizer A modern Super Heated Water Shower Sterilizer can offer several important features, including: > Uniform heat distribution throughout the chamber > Controlled water circulation and showering > Precise temperature and pressure monitoring > Programmable sterilization cycles > Controlled heating and cooling > Stainless steel construction for pharmaceutical applications > Automatic process control options > Data recording and cycle monitoring > Suitable design for different batch sizes > Easy cleaning and maintenance The exact configuration, chamber capacity, automation level, and utilities can be customized according to the customer's process requirements. • Applications of Super Heated Water Shower Sterilizer Super Heated Water Shower Sterilizers are commonly considered for applications where controlled heat treatment of sealed or liquid-filled products is required. Typical applications may include: > Pharmaceutical liquid products > Sealed bottles and containers > Vials and ampoules > Parenteral preparations > Infusion-related products > Heat-sensitive pharmaceutical formulations > Laboratory and healthcare products > Other suitable sealed-container applications The actual application should be evaluated according to product characteristics, container type, required sterilization parameters, and validated process requirements. • Advantages of Super Heated Water Shower Sterilization One of the major advantages of this technology is uniform heat transfer. Continuous circulation of heated water helps maintain consistent temperature throughout the chamber. It can also provide controlled heating and cooling, which may reduce the possibility of thermal stress on containers and products. The process can be automated to improve repeatability and operational efficiency. Another important benefit is that the system can be designed with monitoring and recording capabilities, helping manufacturers maintain process control and documentation requirements.
product image
Pharma - Sterilization

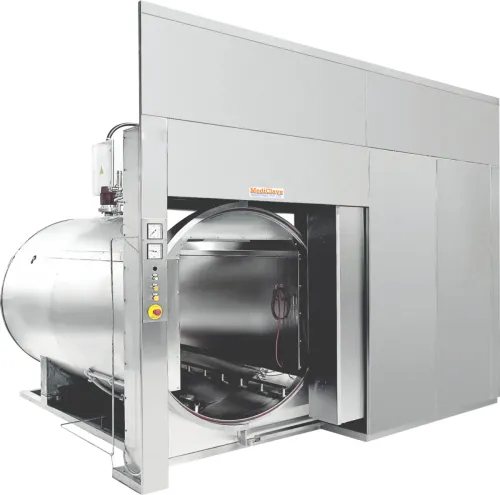
>> What Is a Rubber Bung Processor Cum Steam Sterilizer? A Rubber Bung Processor Cum Steam Sterilizer is pharmaceutical equipment used for the cleaning, treatment, and sterilization of rubber closures before they are used for filling and sealing pharmaceutical products. Rubber bungs can come into direct or indirect contact with sterile pharmaceutical products. Therefore, effective processing is essential to reduce microbial contamination and maintain the required level of cleanliness. The system uses controlled washing and saturated steam sterilization to process rubber bungs effectively. Depending on the equipment configuration and manufacturing requirements, the processing cycle can include washing, rinsing, sterilization, and drying or related controlled stages. >> Why Is Rubber Bung Sterilization Important? Rubber closures are an important part of injectable and other pharmaceutical packaging systems. If they are not properly processed, microorganisms, particles, or residues may affect the quality and safety of the final product. A properly designed rubber bung sterilization system helps pharmaceutical manufacturers achieve: • Effective microbial control • Consistent processing cycles • Improved cleanliness of rubber closures • Reduced contamination risk • Controlled sterilization conditions • Better production efficiency • Improved batch-to-batch consistency For sterile pharmaceutical manufacturing, reliable processing of rubber bungs is therefore an essential part of the overall production process. >> How Does a Rubber Bung Processor Work? The exact process depends on the equipment design and validated operating procedure. Generally, rubber bungs are loaded into the processing chamber and subjected to controlled washing and rinsing stages. After washing, the bungs undergo a steam sterilization cycle under controlled temperature, pressure, and exposure time. Steam penetrates the load and helps destroy microorganisms. A typical processing sequence may include: 1. Loading: Rubber bungs are placed into the processing system. 2. Washing: The bungs are washed to remove dirt, residues, and particulate matter. 3. Rinsing: Controlled rinsing helps remove remaining cleaning agents and contaminants. 4. Sterilization: Saturated steam is introduced at controlled conditions. 5. Holding: The load remains at the required sterilization conditions for the validated exposure period. 6. Cooling/Drying: Depending on the design, controlled cooling or drying may be carried out. 7. Unloading: Processed and sterilized rubber bungs are removed for further pharmaceutical use. >> Key Features of Rubber Bung Processor Cum Steam Sterilizer Modern pharmaceutical rubber bung processors are designed to provide reliable and repeatable operation. Important features can include: • Stainless steel construction • Controlled washing and rinsing • Saturated steam sterilization • Temperature and pressure monitoring • Programmable sterilization cycles • Automatic or semi-automatic operation • Hygienic chamber design • Easy cleaning and maintenance • Safety interlocks • Batch process monitoring The equipment can be customized according to production capacity, rubber bung type, process requirements, and pharmaceutical facility specifications. >> Applications of Rubber Bung Processor Cum Steam Sterilizer Rubber Bung Processor Cum Steam Sterilizers are primarily used in pharmaceutical manufacturing facilities, especially where sterile closures are required. Common applications include: • Injectable manufacturing • Vial filling operations • Parenteral production • Pharmaceutical formulation facilities • Sterile manufacturing plants • Biopharmaceutical production • Healthcare product manufacturing The equipment helps manufacturers prepare rubber closures before they are introduced into controlled sterile production areas. >> Why Choose a Reliable Manufacturer? Selecting the right equipment manufacturer is important because sterilization equipment must deliver consistent performance and support validated pharmaceutical processes. A reliable manufacturer can provide appropriate equipment configuration, suitable material selection, process controls, safety features, documentation, installation support, and after-sales assistance. Mediclave Industries manufactures pharmaceutical sterilization and process equipment for applications where hygiene, reliability, and controlled processing are important. You can explore the company's pharmaceutical equipment range through the Mediclave Industries website. >> Frequently Asked Questions 1. What type of steam is used? Saturated steam is commonly used for pharmaceutical sterilization applications, subject to the validated process requirements. 6. Who manufactures Rubber Bung Processor Cum Steam Sterilizers? Mediclave Industries manufactures pharmaceutical sterilization and process equipment, including Rubber Bung Processor Cum Steam Sterilizer systems.

product image
Pharma - Water Systems

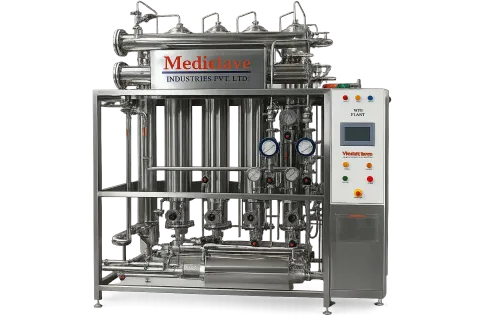
>> What Is a Multi Column Distillation Plant? A Multi Column Distillation Plant is a pharmaceutical water purification system consisting of multiple distillation columns arranged to work together efficiently. The system uses heat and steam to separate water from dissolved and suspended impurities. During the process, water is converted into vapour and then condensed to obtain purified distilled water. The use of multiple columns improves the efficiency of the distillation process. Depending on the design, the system can use energy from one column to support the operation of another column, helping reduce overall steam consumption. This makes the system suitable for pharmaceutical manufacturing facilities where large quantities of high-quality water are required continuously. >> How Does a Multi Column Distillation Plant Work? The working principle of a Multi Column Distillation Plant is based on evaporation and condensation. Initially, pre-treated feed water enters the first distillation column. Heat is supplied to convert the water into steam. Most non-volatile impurities remain behind while purified water vapour moves forward. The vapour generated from one column can be used as a heating medium for the next column. This process continues through multiple columns. The final vapour is condensed and collected as distilled water. Depending on the plant design and required pharmaceutical standards, the system can incorporate additional arrangements for monitoring, separation and collection. The overall process can be summarized as: Feed Water → Preheating → Evaporation → Multiple-Stage Distillation → Condensation → Distilled Pharmaceutical Water >> Why Is Multi Column Distillation Used in the Pharmaceutical Industry? Pharmaceutical manufacturing requires water with controlled chemical and microbiological quality. Water used in manufacturing must be produced and handled through properly designed systems. A Multi Column Distillation Plant provides several important advantages: 1. High-Quality Distilled Water The distillation process helps remove many dissolved impurities, microorganisms and other unwanted substances from feed water. 2. Suitable for Pharmaceutical Applications The system can be designed for pharmaceutical water requirements and integrated with other water treatment and distribution systems. 3. Energy-Efficient Operation Multiple columns can allow heat energy to be reused between stages. This can reduce steam consumption compared with less efficient single-stage arrangements. 4. Continuous Production Multi-column systems are suitable for facilities requiring a continuous supply of purified or distilled water. 5. Hygienic Construction Pharmaceutical distillation plants are generally designed using suitable stainless-steel materials and hygienic construction practices to minimize contamination risks. >> Applications of Multi Column Distillation Plants Multi Column Distillation Plants are widely used in industries where high-quality distilled water is essential. Typical applications include: • Pharmaceutical manufacturing plants • Injectable manufacturing facilities • Biotechnology industries • Bulk drug manufacturing • API manufacturing facilities • Sterile manufacturing units • Hospitals and specialized healthcare facilities • Research and laboratory facilities The distilled water generated by the plant can be used as part of pharmaceutical water systems, subject to the applicable process and quality requirements. >> Key Features to Consider When Selecting a Multi Column Distillation Plant Choosing the right distillation plant is important because pharmaceutical water requirements can vary from one facility to another. Before purchasing a system, manufacturers should consider: Production Capacity: The plant should provide sufficient water output according to current and future requirements. Material of Construction: Product-contact parts should use appropriate hygienic materials, commonly pharmaceutical-grade stainless steel such as SS 316L where required by the design. Steam Consumption: Energy efficiency is an important consideration for reducing operating costs. Automation: Modern systems can include automatic controls, monitoring instruments and safety features for easier operation. Hygienic Design: The system should minimize dead legs, contamination risks and areas where water can stagnate. Maintenance: Easy access to components can simplify inspection, cleaning and maintenance. Documentation: Pharmaceutical manufacturers should consider the required documentation, testing and qualification support when selecting equipment.