Ahmedabad
08042755106
+917041232204
Pharma - Sterilization by Mediclave Industries

Steam + Air Mixture Sterilizer & Terminal Steam Sterilizer

In stockcod not available

Subcategory Tags

Steam + Air Mixture Sterilizer Manufacturer in Maharastra Steam + Air Mixture Sterilizer Manufacturer in Mumbai Steam + Air Mixture Sterilizer Manufacturer in Pune Steam + Air Mixture Sterilizer Manufacturer in Navi Mumbai Steam + Air Mixture Sterilizer Manufacturer in Nagpur Steam + Air Mixture Sterilizer Manufacturer in Uttar Pradesh Steam + Air Mixture Sterilizer Manufacturer in Lucknow Steam + Air Mixture Sterilizer Manufacturer in Noida Steam + Air Mixture Sterilizer Manufacturer in Agra Steam + Air Mixture Sterilizer Manufacturer in Karnataka Steam + Air Mixture Sterilizer Manufacturer in Bengaluru Steam + Air Mixture Sterilizer Manufacturer in Mysuru Steam + Air Mixture Sterilizer Manufacturer in Tamilnadu Steam + Air Mixture Sterilizer Manufacturer in Chennai Steam + Air Mixture Sterilizer Manufacturer in Coimbatore Steam + Air Mixture Sterilizer Manufacturer in West Bengal Steam + Air Mixture Sterilizer Manufacturer in Kolkata Steam + Air Mixture Sterilizer Manufacturer in Siliguri Steam + Air Mixture Sterilizer Manufacturer in Kharagpur Steam + Air Mixture Sterilizer Manufacturer in Gujarat Steam + Air Mixture Sterilizer Manufacturer in Ahmedabad Steam + Air Mixture Sterilizer Manufacturer in Madhya Pradesh Steam + Air Mixture Sterilizer Manufacturer in Indore Steam + Air Mixture Sterilizer Manufacturer in Rajasthan Steam + Air Mixture Sterilizer Manufacturer in Bihar Steam + Air Mixture Sterilizer Manufacturer in Patna Steam + Air Mixture Sterilizer Manufacturer in Manali Steam + Air Mixture Sterilizer Manufacturer in Solan Steam + Air Mixture Sterilizer Manufacturer in Kullu Steam + Air Mixture Sterilizer Manufacturer in Ludhiana Steam + Air Mixture Sterilizer Manufacturer in Bathinda "Steam + Air Mixture Sterilizer Manufacturer in Rishikesh " Steam + Air Mixture Sterilizer Manufacturer in Nainital Steam + Air Mixture Sterilizer Manufacturer in Roorkee Steam + Air Mixture Sterilizer Manufacturer in Ambala Steam + Air Mixture Sterilizer Manufacturer in Yamunanagar Steam + Air Mixture Sterilizer Manufacturer in Pune Steam + Air Mixture Sterilizer Manufacturer in Nashik Steam + Air Mixture Sterilizer Manufacturer in Thane Steam + Air Mixture Sterilizer Manufacturer in Amravati Steam + Air Mixture Sterilizer Manufacturer in GOA Steam + Air Mixture Sterilizer Manufacturer in Rewa Steam + Air Mixture Sterilizer Manufacturer in Satna Steam + Air Mixture Sterilizer Manufacturer in Darbhanga Steam + Air Mixture Sterilizer Manufacturer in Jamshedpur Steam + Air Mixture Sterilizer Manufacturer in Khammam Steam + Air Mixture Sterilizer Manufacturer in Vijayawada Steam + Air Mixture Sterilizer Manufacturer in Mysuru Steam + Air Mixture Sterilizer Manufacturer in kerala Steam + Air Mixture Sterilizer Manufacturer in ODISHA Steam + Air Mixture Sterilizer Manufacturer in Cuttack Steam + Air Mixture Sterilizer Manufacturer in SIKKIM Steam + Air Mixture Sterilizer Manufacturer in New Delhi Steam + Air Mixture Sterilizer Manufacturer in West Delhi Steam + Air Mixture Sterilizer Manufacturer in East Delhi Steam + Air Mixture Sterilizer Manufacturer in North Delhi Steam + Air Mixture Sterilizer Manufacturer in South Delhi Terminal Steam Sterilizer Manufacturer in Maharastra Terminal Steam Sterilizer Manufacturer in Mumbai Terminal Steam Sterilizer Manufacturer in Pune Terminal Steam Sterilizer Manufacturer in Navi Mumbai Terminal Steam Sterilizer Manufacturer in Nagpur Terminal Steam Sterilizer Manufacturer in Uttar Pradesh Terminal Steam Sterilizer Manufacturer in Lucknow Terminal Steam Sterilizer Manufacturer in Noida Terminal Steam Sterilizer Manufacturer in Agra Terminal Steam Sterilizer Manufacturer in Karnataka Terminal Steam Sterilizer Manufacturer in Bengaluru Terminal Steam Sterilizer Manufacturer in Mysuru Terminal Steam Sterilizer Manufacturer in Tamilnadu Terminal Steam Sterilizer Manufacturer in Chennai Terminal Steam Sterilizer Manufacturer in Coimbatore Terminal Steam Sterilizer Manufacturer in West Bengal Terminal Steam Sterilizer Manufacturer in Kolkata Terminal Steam Sterilizer Manufacturer in Siliguri Terminal Steam Sterilizer Manufacturer in Kharagpur Terminal Steam Sterilizer Manufacturer in Gujarat Terminal Steam Sterilizer Manufacturer in Ahmedabad Terminal Steam Sterilizer Manufacturer in Madhya Pradesh Terminal Steam Sterilizer Manufacturer in Indore Terminal Steam Sterilizer Manufacturer in Rajasthan Terminal Steam Sterilizer Manufacturer in Bihar Terminal Steam Sterilizer Manufacturer in Patna Terminal Steam Sterilizer Manufacturer in Manali Terminal Steam Sterilizer Manufacturer in Solan Terminal Steam Sterilizer Manufacturer in Kullu Terminal Steam Sterilizer Manufacturer in Ludhiana Terminal Steam Sterilizer Manufacturer in Bathinda "Terminal Steam Sterilizer Manufacturer in Rishikesh " Terminal Steam Sterilizer Manufacturer in Nainital Terminal Steam Sterilizer Manufacturer in Roorkee Terminal Steam Sterilizer Manufacturer in Ambala Terminal Steam Sterilizer Manufacturer in Yamunanagar Terminal Steam Sterilizer Manufacturer in Pune Terminal Steam Sterilizer Manufacturer in Nashik Terminal Steam Sterilizer Manufacturer in Thane Terminal Steam Sterilizer Manufacturer in Amravati Terminal Steam Sterilizer Manufacturer in GOA Terminal Steam Sterilizer Manufacturer in Rewa Terminal Steam Sterilizer Manufacturer in Darbhanga Terminal Steam Sterilizer Manufacturer in Jamshedpur Terminal Steam Sterilizer Manufacturer in Khammam Terminal Steam Sterilizer Manufacturer in Vijayawada Terminal Steam Sterilizer Manufacturer in Mysuru Terminal Steam Sterilizer Manufacturer in kerala Terminal Steam Sterilizer Manufacturer in ODISHA Terminal Steam Sterilizer Manufacturer in SIKKIM Terminal Steam Sterilizer Manufacturer in New Delhi
Phone Number

08042755106

Please keep 0 before dialling the number.

Mon-Thu: 10 AM - 2 PM • Fri: 3 PM - 7AM

Other Website Visit our other website
Address 418, 4th Floor , Arth Business Center (ABC , Galaxy Heights, Nikol

Ahmedabad, India, 382415

Description

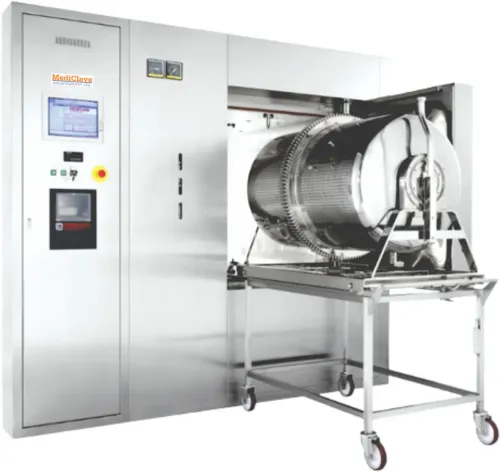
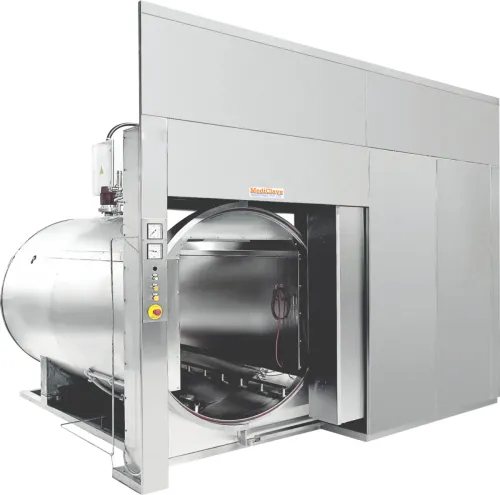
>> Steam + Air Mixture Sterilizer The Steam + Air Mixture Sterilizer is specially designed for the sterilization of heat-sensitive and deformable products such as IV fluids, plastic containers, syringes, and sealed bottles. This advanced system uses a precise combination of steam and filtered air to maintain uniform temperature distribution while simultaneously controlling chamber pressure. Unlike conventional steam sterilizers, this technology ensures that the external pressure inside the chamber balances the internal pressure of the product containers. This prevents deformation, leakage, or damage during the sterilization process, making it ideal for delicate pharmaceutical packaging. The system is equipped with advanced control mechanisms that continuously regulate temperature, pressure, and air-steam ratio, ensuring consistent and reliable sterilization results. With its robust design and compliance with GMP standards, it is widely used in pharmaceutical and healthcare industries where product integrity is critical. Key Highlights: > Uniform heat distribution using steam-air mixture > Precise pressure control to protect sensitive containers > Ideal for plastic bottles, IV fluids, and sealed products > PLC-based control system with programmable cycles > GMP-compliant design with high reliability >> Terminal Steam Sterilizer The Terminal Steam Sterilizer is a high-performance solution used for the final sterilization of sealed pharmaceutical products after filling and packaging. It ensures complete microbial destruction, providing the highest level of sterility assurance for products before they reach the end user. This sterilizer operates using saturated steam under controlled temperature and pressure conditions, delivering deep and uniform penetration of heat throughout the product load. It is commonly used for glass vials, ampoules, bottles, and other sealed containers in pharmaceutical manufacturing. Designed for efficiency and reliability, the system offers precise cycle control, consistent performance, and full compliance with GMP and regulatory standards. Its robust construction and advanced automation reduce human intervention and ensure repeatable, validated sterilization processes. Key Highlights: > Final (terminal) sterilization of sealed products > High sterility assurance level (SAL) > Uniform steam penetration and heat distribution > Suitable for vials, ampoules, bottles, and injectables > Fully automatic operation with PLC & HMI > GMP and cGMP compliant design

Type Steam + Air Mixture Sterilizer // Terminal Steam Sterilizer (Autoclave for Final Product Sterilization)
Application Sterilization of Sealed Containers (IV Fluids, Bottles, Plastic Containers, FFS/BFS Products) // Terminal Sterilization of Filled & Sealed Products (Ampoules, Vials, Bottles, IV Bags)
Sterilization Method Steam-Air Mixture with Overpressure Control // Saturated Steam Sterilization
Chamber Type Horizontal Cylindrical / Rectangular
Capacity Range 100 Liters to 3000+ Liters (Customizable)
Material of Construction SS 316L (Inner Chamber), SS 304 (Outer Body)
Operating Temperature 105°C to 125°C // 121°C to 134°C
Operating Pressure Controlled Overpressure (1.5 – 3.5 Bar) // 1.2 to 3 Bar
Air Circulation System High-Efficiency Fan for Uniform Heat Distribution
Heating System Direct Steam Injection // Steam Jacket / Direct Steam Injection
Cooling System Water Spray / Heat Exchanger Cooling // Water Spray Cooling (Optional)
Pressure Control Compressed Air Injection with PID Control
Temperature Uniformity ±0.5°C
Control System PLC Based with HMI Touchscreen
Operation Mode Fully Automatic
Sterilization Cycles Heating, Sterilization Hold, Cooling with Pressure Balance
Monitoring System Temperature, Pressure & F₀ Value Monitoring
Safety Features Overpressure Protection, Door Interlock, Emergency Stop
Vacuum System Not Required (Positive Pressure Process)
Data Logging SCADA / Printer / USB (Optional)
Power Supply 415 V, 3 Phase, 50 Hz
Accessories Loading Trolley, Baskets, Container Holders
Installation Floor Mounted
Compliance GMP / cGMP / FDA / EU Guidelines

Keywords

Other Products

view all

6814772a5d263414004dd4a4 Card 2

product image
Pharma - Sterilization

In pharmaceutical manufacturing, maintaining product quality and sterility is essential. Sterilization equipment plays a critical role in ensuring that products, containers, and other components are processed under controlled and validated conditions. One advanced solution used for this purpose is the Super Heated Water Shower Sterilizer. A Super Heated Water Shower Sterilizer is designed to sterilize heat-sensitive and liquid-filled products using circulating super-heated water under controlled pressure and temperature. The system provides uniform heat distribution and helps minimize the risk of thermal damage while achieving effective sterilization. • What Is a Super Heated Water Shower Sterilizer? A Super Heated Water Shower Sterilizer is a pharmaceutical sterilization system that uses heated water as the sterilizing medium. During the sterilization cycle, hot water is continuously circulated and sprayed or showered over the load inside the sterilization chamber. Unlike conventional steam sterilization, this technology can be particularly useful for sealed containers, liquid products, bottles, vials, and other pharmaceutical products where direct steam contact may not be desirable. The system operates with controlled temperature, pressure, circulation, and cooling parameters to provide consistent and reproducible sterilization cycles. • How Does a Super Heated Water Shower Sterilizer Work? The sterilization process generally involves several controlled stages. 1. Loading The products or containers to be sterilized are loaded into the chamber using suitable trays, baskets, or loading systems. 2. Heating Water is heated to the required sterilization temperature using an efficient heating arrangement. The heated water is then circulated through the chamber. 3. Water Showering and Circulation A powerful circulation system distributes hot water uniformly throughout the chamber. The continuous showering action helps ensure that all surfaces of the load receive consistent heat exposure. 4. Sterilization Holding Once the required temperature is achieved, the system maintains the programmed temperature for a specified holding time. This controlled exposure helps achieve the required microbial reduction. 5. Cooling After the sterilization stage, the product is gradually cooled under controlled conditions. Proper cooling helps protect containers and products from thermal shock and pressure-related damage. 6. Cycle Completion Once the programmed cycle parameters are completed, the chamber returns to safe conditions and the sterilized load can be unloaded according to the validated operating procedure. • Key Features of Super Heated Water Shower Sterilizer A modern Super Heated Water Shower Sterilizer can offer several important features, including: > Uniform heat distribution throughout the chamber > Controlled water circulation and showering > Precise temperature and pressure monitoring > Programmable sterilization cycles > Controlled heating and cooling > Stainless steel construction for pharmaceutical applications > Automatic process control options > Data recording and cycle monitoring > Suitable design for different batch sizes > Easy cleaning and maintenance The exact configuration, chamber capacity, automation level, and utilities can be customized according to the customer's process requirements. • Applications of Super Heated Water Shower Sterilizer Super Heated Water Shower Sterilizers are commonly considered for applications where controlled heat treatment of sealed or liquid-filled products is required. Typical applications may include: > Pharmaceutical liquid products > Sealed bottles and containers > Vials and ampoules > Parenteral preparations > Infusion-related products > Heat-sensitive pharmaceutical formulations > Laboratory and healthcare products > Other suitable sealed-container applications The actual application should be evaluated according to product characteristics, container type, required sterilization parameters, and validated process requirements. • Advantages of Super Heated Water Shower Sterilization One of the major advantages of this technology is uniform heat transfer. Continuous circulation of heated water helps maintain consistent temperature throughout the chamber. It can also provide controlled heating and cooling, which may reduce the possibility of thermal stress on containers and products. The process can be automated to improve repeatability and operational efficiency. Another important benefit is that the system can be designed with monitoring and recording capabilities, helping manufacturers maintain process control and documentation requirements.
6814772a5d263414004dd4a4 Card 2

product image
Pharma - Sterilization

>> What Is a Rubber Bung Processor Cum Steam Sterilizer? A Rubber Bung Processor Cum Steam Sterilizer is pharmaceutical equipment used for the cleaning, treatment, and sterilization of rubber closures before they are used for filling and sealing pharmaceutical products. Rubber bungs can come into direct or indirect contact with sterile pharmaceutical products. Therefore, effective processing is essential to reduce microbial contamination and maintain the required level of cleanliness. The system uses controlled washing and saturated steam sterilization to process rubber bungs effectively. Depending on the equipment configuration and manufacturing requirements, the processing cycle can include washing, rinsing, sterilization, and drying or related controlled stages. >> Why Is Rubber Bung Sterilization Important? Rubber closures are an important part of injectable and other pharmaceutical packaging systems. If they are not properly processed, microorganisms, particles, or residues may affect the quality and safety of the final product. A properly designed rubber bung sterilization system helps pharmaceutical manufacturers achieve: • Effective microbial control • Consistent processing cycles • Improved cleanliness of rubber closures • Reduced contamination risk • Controlled sterilization conditions • Better production efficiency • Improved batch-to-batch consistency For sterile pharmaceutical manufacturing, reliable processing of rubber bungs is therefore an essential part of the overall production process. >> How Does a Rubber Bung Processor Work? The exact process depends on the equipment design and validated operating procedure. Generally, rubber bungs are loaded into the processing chamber and subjected to controlled washing and rinsing stages. After washing, the bungs undergo a steam sterilization cycle under controlled temperature, pressure, and exposure time. Steam penetrates the load and helps destroy microorganisms. A typical processing sequence may include: 1. Loading: Rubber bungs are placed into the processing system. 2. Washing: The bungs are washed to remove dirt, residues, and particulate matter. 3. Rinsing: Controlled rinsing helps remove remaining cleaning agents and contaminants. 4. Sterilization: Saturated steam is introduced at controlled conditions. 5. Holding: The load remains at the required sterilization conditions for the validated exposure period. 6. Cooling/Drying: Depending on the design, controlled cooling or drying may be carried out. 7. Unloading: Processed and sterilized rubber bungs are removed for further pharmaceutical use. >> Key Features of Rubber Bung Processor Cum Steam Sterilizer Modern pharmaceutical rubber bung processors are designed to provide reliable and repeatable operation. Important features can include: • Stainless steel construction • Controlled washing and rinsing • Saturated steam sterilization • Temperature and pressure monitoring • Programmable sterilization cycles • Automatic or semi-automatic operation • Hygienic chamber design • Easy cleaning and maintenance • Safety interlocks • Batch process monitoring The equipment can be customized according to production capacity, rubber bung type, process requirements, and pharmaceutical facility specifications. >> Applications of Rubber Bung Processor Cum Steam Sterilizer Rubber Bung Processor Cum Steam Sterilizers are primarily used in pharmaceutical manufacturing facilities, especially where sterile closures are required. Common applications include: • Injectable manufacturing • Vial filling operations • Parenteral production • Pharmaceutical formulation facilities • Sterile manufacturing plants • Biopharmaceutical production • Healthcare product manufacturing The equipment helps manufacturers prepare rubber closures before they are introduced into controlled sterile production areas. >> Why Choose a Reliable Manufacturer? Selecting the right equipment manufacturer is important because sterilization equipment must deliver consistent performance and support validated pharmaceutical processes. A reliable manufacturer can provide appropriate equipment configuration, suitable material selection, process controls, safety features, documentation, installation support, and after-sales assistance. Mediclave Industries manufactures pharmaceutical sterilization and process equipment for applications where hygiene, reliability, and controlled processing are important. You can explore the company's pharmaceutical equipment range through the Mediclave Industries website. >> Frequently Asked Questions 1. What type of steam is used? Saturated steam is commonly used for pharmaceutical sterilization applications, subject to the validated process requirements. 6. Who manufactures Rubber Bung Processor Cum Steam Sterilizers? Mediclave Industries manufactures pharmaceutical sterilization and process equipment, including Rubber Bung Processor Cum Steam Sterilizer systems.

6814772a5d263414004dd4a4 Card 2

product image
Pharma - Water Systems

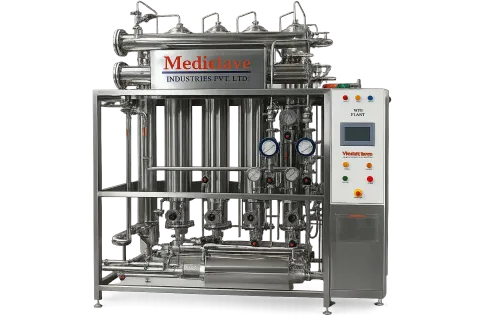
>> What Is a Multi Column Distillation Plant? A Multi Column Distillation Plant is a pharmaceutical water purification system consisting of multiple distillation columns arranged to work together efficiently. The system uses heat and steam to separate water from dissolved and suspended impurities. During the process, water is converted into vapour and then condensed to obtain purified distilled water. The use of multiple columns improves the efficiency of the distillation process. Depending on the design, the system can use energy from one column to support the operation of another column, helping reduce overall steam consumption. This makes the system suitable for pharmaceutical manufacturing facilities where large quantities of high-quality water are required continuously. >> How Does a Multi Column Distillation Plant Work? The working principle of a Multi Column Distillation Plant is based on evaporation and condensation. Initially, pre-treated feed water enters the first distillation column. Heat is supplied to convert the water into steam. Most non-volatile impurities remain behind while purified water vapour moves forward. The vapour generated from one column can be used as a heating medium for the next column. This process continues through multiple columns. The final vapour is condensed and collected as distilled water. Depending on the plant design and required pharmaceutical standards, the system can incorporate additional arrangements for monitoring, separation and collection. The overall process can be summarized as: Feed Water → Preheating → Evaporation → Multiple-Stage Distillation → Condensation → Distilled Pharmaceutical Water >> Why Is Multi Column Distillation Used in the Pharmaceutical Industry? Pharmaceutical manufacturing requires water with controlled chemical and microbiological quality. Water used in manufacturing must be produced and handled through properly designed systems. A Multi Column Distillation Plant provides several important advantages: 1. High-Quality Distilled Water The distillation process helps remove many dissolved impurities, microorganisms and other unwanted substances from feed water. 2. Suitable for Pharmaceutical Applications The system can be designed for pharmaceutical water requirements and integrated with other water treatment and distribution systems. 3. Energy-Efficient Operation Multiple columns can allow heat energy to be reused between stages. This can reduce steam consumption compared with less efficient single-stage arrangements. 4. Continuous Production Multi-column systems are suitable for facilities requiring a continuous supply of purified or distilled water. 5. Hygienic Construction Pharmaceutical distillation plants are generally designed using suitable stainless-steel materials and hygienic construction practices to minimize contamination risks. >> Applications of Multi Column Distillation Plants Multi Column Distillation Plants are widely used in industries where high-quality distilled water is essential. Typical applications include: • Pharmaceutical manufacturing plants • Injectable manufacturing facilities • Biotechnology industries • Bulk drug manufacturing • API manufacturing facilities • Sterile manufacturing units • Hospitals and specialized healthcare facilities • Research and laboratory facilities The distilled water generated by the plant can be used as part of pharmaceutical water systems, subject to the applicable process and quality requirements. >> Key Features to Consider When Selecting a Multi Column Distillation Plant Choosing the right distillation plant is important because pharmaceutical water requirements can vary from one facility to another. Before purchasing a system, manufacturers should consider: Production Capacity: The plant should provide sufficient water output according to current and future requirements. Material of Construction: Product-contact parts should use appropriate hygienic materials, commonly pharmaceutical-grade stainless steel such as SS 316L where required by the design. Steam Consumption: Energy efficiency is an important consideration for reducing operating costs. Automation: Modern systems can include automatic controls, monitoring instruments and safety features for easier operation. Hygienic Design: The system should minimize dead legs, contamination risks and areas where water can stagnate. Maintenance: Easy access to components can simplify inspection, cleaning and maintenance. Documentation: Pharmaceutical manufacturers should consider the required documentation, testing and qualification support when selecting equipment.