
How Does a Super Heated Water Shower Sterilizer Ensure Safe and Reliable Sterilization in Pharmaceutical Manufacturing?
Sterilization is one of the most important steps in pharmaceutical manufacturing. Every injectable medicine, IV fluid, eye drop, biological product, and many other healthcare products must be completely free from harmful microorganisms before reaching patients. Even a small contamination can affect product quality, reduce shelf life, and create serious health risks.
This is why pharmaceutical companies invest in advanced sterilization systems that deliver consistent, validated, and reliable performance. Among the most effective technologies available today is the Super Heated Water Shower Sterilizer. It is specially designed for sterilizing products packed in sealed containers while maintaining product integrity and ensuring uniform heat distribution throughout the sterilization cycle.
Whether you are planning a new pharmaceutical manufacturing facility or upgrading an existing production line, understanding how a Super Heated Water Shower Sterilizer works can help you make the right investment. In this guide, we will explain everything you need to know—from its working principle and applications to its benefits, features, validation process, and maintenance.
What Is a Super Heated Water Shower Sterilizer?
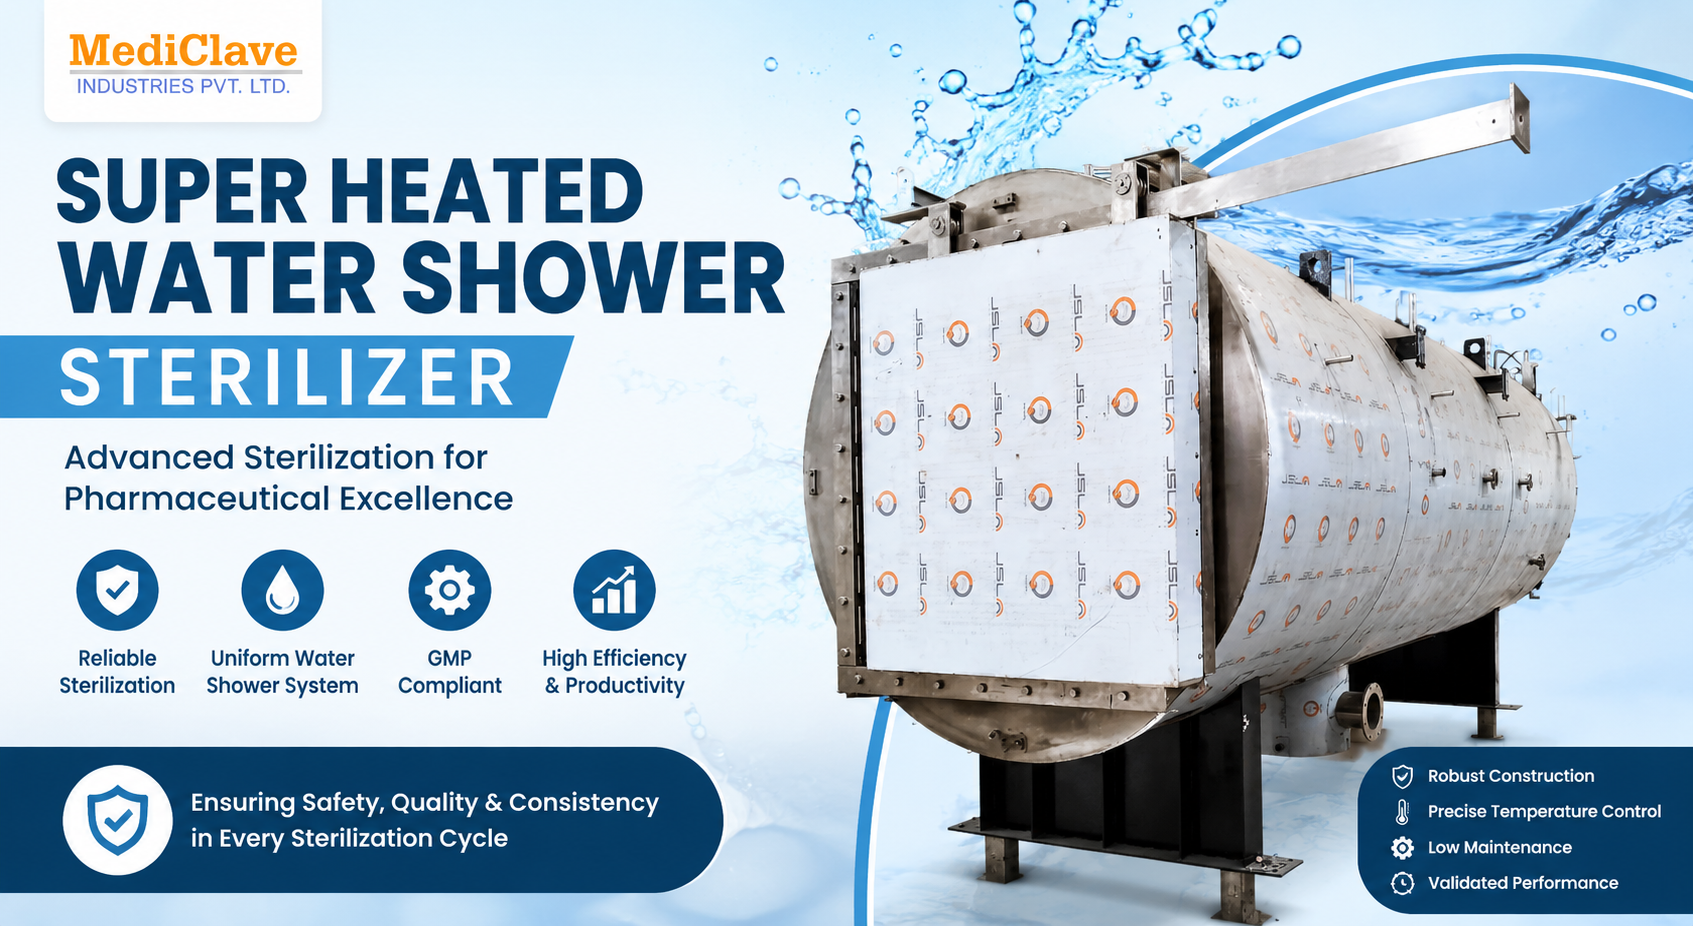
A Super Heated Water Shower Sterilizer is an advanced sterilization system used primarily in pharmaceutical and biotechnology industries. It sterilizes products by circulating super-heated water over the load while maintaining controlled pressure inside the chamber.
Unlike traditional steam sterilizers that rely only on saturated steam, this equipment continuously sprays heated water over the products from multiple directions. The heated water provides highly uniform temperature distribution and protects sensitive containers from thermal shock.
The sterilization process is carefully monitored through automated controls that regulate temperature, pressure, circulation, and cycle timing. This ensures every product receives the required sterilization conditions without damaging packaging or product quality.
Pharmaceutical manufacturers widely use this technology because it offers excellent repeatability, process validation, and compliance with international GMP standards.
Why Is Sterilization So Important?
Sterilization eliminates bacteria, fungi, viruses, spores, and other microorganisms that may contaminate pharmaceutical products.
Proper sterilization helps manufacturers:
Protect patient health
Maintain product sterility
Increase product shelf life
Meet GMP requirements
Pass regulatory inspections
Reduce product recalls
Improve manufacturing reliability
Ensure consistent product quality
Without effective sterilization, even a well-manufactured pharmaceutical product may become unsafe for human use.
How Does a Super Heated Water Shower Sterilizer Work?
The working process follows several carefully controlled stages.
1. Product Loading
Products are placed inside specially designed stainless steel trays or baskets. These baskets allow proper water circulation around every container.
The chamber door is securely locked before the cycle begins.
2. Chamber Pressurization
The chamber is pressurized using filtered compressed air. This pressure prevents deformation of plastic bottles, IV bags, and other flexible packaging during heating.
Maintaining proper pressure is one of the biggest advantages of this sterilization method.
3. Water Heating
Purified water stored in the circulation system is heated using steam through a heat exchanger.
The water reaches the desired sterilization temperature before it is sprayed inside the chamber.
4. Water Shower Circulation
Powerful circulation pumps spray super-heated water through multiple nozzles.
The water continuously showers the entire product load from every direction, ensuring:
Uniform heating
Consistent sterilization
No cold spots
Excellent temperature distribution
The water is collected, reheated, and recirculated throughout the cycle.
5. Sterilization Holding Time
Once the required temperature is achieved, the sterilizer maintains the programmed holding time.
This stage destroys microorganisms and bacterial spores.
The entire process is automatically controlled using PLC and HMI systems.
6. Controlled Cooling
After sterilization, the equipment gradually cools the products while maintaining chamber pressure.
This prevents:
Bottle deformation
Container breakage
Seal failure
Product damage
Controlled cooling is particularly important for glass containers and plastic packaging.
7. Cycle Completion
After cooling, the chamber pressure returns to normal.
The sterilized products are unloaded and transferred to the next manufacturing stage.
Which Products Can Be Sterilized?
A Super Heated Water Shower Sterilizer is suitable for many pharmaceutical products, including:
IV fluids
Injectable medicines
Ampoules
Glass bottles
Plastic bottles
BFS containers
Infusion bags
Eye drops
Biological products
Veterinary medicines
Nutraceutical liquids
Dialysis solutions
It is also suitable for products requiring terminal sterilization after filling and sealing.
Why Choose a Water Shower Sterilizer Instead of Traditional Steam Sterilization?
Traditional steam sterilizers work very well for many applications. However, certain products require better temperature control and protection during sterilization.
A Super Heated Water Shower Sterilizer provides several additional advantages.
Uniform Heat Distribution
Water transfers heat more efficiently than steam alone.
The continuous water shower minimizes temperature variation inside the chamber.
Protection of Sensitive Containers
Plastic bottles and flexible packaging can deform under high steam pressure.
The controlled chamber pressure prevents this problem.
Reduced Thermal Shock
Gradual heating and cooling reduce stress on glass containers.
This lowers the risk of cracks and breakage.
Better Product Quality
Uniform sterilization helps preserve product appearance, stability, and packaging integrity.
Higher Process Reliability
Automated monitoring ensures every cycle follows validated parameters.
Key Features of a Modern Super Heated Water Shower Sterilizer
Today's pharmaceutical sterilizers include advanced technologies that improve performance and compliance.
Common features include:
PLC-based automation
Touchscreen HMI
Stainless steel chamber
Stainless steel piping
High-capacity circulation pumps
Precision temperature sensors
Pressure monitoring
Automatic control valves
Data logging
Batch recording
Password-protected operation
Multiple validated sterilization programs
Alarm systems
Safety interlocks
GMP-compliant construction
Low maintenance design
These features improve both operational efficiency and regulatory compliance.
Industries That Use Super Heated Water Shower Sterilizers
Many industries rely on this equipment for reliable sterilization.
These include:
Pharmaceutical manufacturing
Biotechnology companies
Vaccine production
Injectable manufacturing plants
Nutraceutical industries
Veterinary pharmaceutical companies
Research laboratories
Medical device manufacturers
Healthcare product manufacturers
Its versatility makes it suitable for a wide range of sterile manufacturing environments.
Importance of Validation
Validation is essential in pharmaceutical manufacturing.
A sterilizer must consistently produce the same sterilization results every time.
Validation typically includes:
Installation Qualification (IQ)
Confirms the equipment is installed correctly.
Operational Qualification (OQ)
Verifies that every operating parameter functions within specified limits.
Performance Qualification (PQ)
Demonstrates consistent sterilization performance using actual production loads.
Regular validation builds confidence in product safety and satisfies regulatory authorities.
Compliance with International Standards
Modern Super Heated Water Shower Sterilizers are designed to comply with major pharmaceutical guidelines, including:
GMP
cGMP
WHO Guidelines
US FDA recommendations
EU GMP
GAMP principles
21 CFR Part 11 (where applicable)
Compliance helps pharmaceutical companies meet customer expectations and regulatory requirements.
How Does This Sterilizer Improve Manufacturing Efficiency?
Investing in advanced sterilization equipment provides several operational benefits.
These include:
Faster batch processing
Improved productivity
Reduced manual intervention
Lower rejection rates
Better batch consistency
Improved documentation
Reduced downtime
Enhanced process control
Easier validation
Higher production capacity
Over time, these improvements contribute to lower operating costs and greater manufacturing efficiency.
Integration with Other Pharmaceutical Equipment
A Super Heated Water Shower Sterilizer works best when integrated with other pharmaceutical processing equipment.
For example, pharmaceutical-grade purified water plays a critical role in sterilization. Manufacturers often use a Multi Column Distillation Plant to generate Water for Injection (WFI), ensuring high-purity water for critical processes. Learn more here:
https://www.mediclaveindustries.in/product/multi-column-distillation-plant/
Similarly, many facilities use a Pure Steam Generator to produce pharmaceutical-grade steam required for various sterilization applications:
https://www.mediclaveindustries.in/product/pure-steam-generator/
To maintain clean processing systems, manufacturers also install CIP & SIP Systems, which automate cleaning and sterilization of pipelines and equipment before production:
https://www.mediclaveindustries.in/product/cip-sip-system/
For products that require different sterilization technologies, manufacturers may also use a Saturated Steam Sterilizer, depending on product characteristics and packaging requirements:
https://www.mediclaveindustries.in/product/saturated-steam-sterilizer/
Together, these systems create a complete pharmaceutical manufacturing solution that supports product quality, process efficiency, and regulatory compliance.
Maintenance Tips
Proper maintenance helps maximize equipment life and maintain sterilization performance.
Recommended practices include:
Inspect spray nozzles regularly.
Check circulation pumps.
Verify sensor calibration.
Monitor pressure gauges.
Replace worn seals promptly.
Clean water filters.
Test safety interlocks.
Validate sterilization cycles periodically.
Maintain detailed service records.
Follow preventive maintenance schedules.
Routine maintenance minimizes unexpected downtime and ensures reliable operation.
Factors to Consider Before Purchasing
Before selecting a Super Heated Water Shower Sterilizer, evaluate several important factors.
Consider:
Chamber capacity
Production volume
Product type
Container material
Automation requirements
Utility availability
Validation support
Documentation package
Energy efficiency
After-sales service
Spare parts availability
Future production expansion
Choosing equipment that matches your manufacturing needs improves long-term productivity.
Why Mediclave Industries?
Mediclave Industries manufactures pharmaceutical sterilization equipment designed for modern production facilities.
The company focuses on:
High-quality stainless steel construction
Advanced automation
Reliable process control
GMP-compliant manufacturing
User-friendly operation
Excellent temperature distribution
Strong after-sales support
Custom-designed solutions
Comprehensive documentation
Long service life
Its equipment is designed to help pharmaceutical manufacturers improve productivity while maintaining the highest quality standards.
Conclusion
A Super Heated Water Shower Sterilizer is an essential solution for pharmaceutical manufacturers that require reliable, uniform, and validated sterilization of products in sealed containers. Its advanced water circulation technology, precise temperature control, controlled chamber pressure, and automated operation ensure that every batch is processed safely and consistently.
Compared with conventional sterilization methods, this technology provides superior heat distribution, protects sensitive packaging, minimizes thermal stress, and supports compliance with global pharmaceutical standards. It is an ideal choice for sterilizing IV fluids, injectable medicines, eye drops, biological products, infusion bags, and many other healthcare products.
When combined with complementary systems such as a Multi Column Distillation Plant, Pure Steam Generator, CIP & SIP System, and Saturated Steam Sterilizer, manufacturers can establish a complete, efficient, and GMP-compliant pharmaceutical production environment.
As the pharmaceutical industry continues to demand higher quality, better documentation, and greater operational efficiency, investing in a modern Super Heated Water Shower Sterilizer is a smart decision that supports long-term product safety, regulatory compliance, and business growth.
Frequently Asked Questions (FAQs)
1. What is a Super Heated Water Shower Sterilizer used for?
It is used to sterilize pharmaceutical products packed in sealed containers such as IV fluids, injectables, infusion bags, eye drops, plastic bottles, and glass bottles.
2. How is it different from a steam sterilizer?
A water shower sterilizer circulates super-heated water over the products while maintaining controlled pressure, providing more uniform heating and better protection for sensitive packaging.
3. Which industries commonly use this equipment?
Pharmaceutical, biotechnology, veterinary pharmaceutical, nutraceutical, and healthcare product manufacturing industries commonly use Super Heated Water Shower Sterilizers.
4. Why is chamber pressure important?
Controlled pressure prevents container deformation, package damage, and seal failure during the heating and cooling process.
5. Is the equipment suitable for GMP pharmaceutical manufacturing?
Yes. Modern Super Heated Water Shower Sterilizers are designed to meet GMP requirements and support validation for pharmaceutical manufacturing processes.