
Multi-Column Distillation Plant: The Complete Guide to High-Purity Water Generation for Pharmaceutical Manufacturing
Water is one of the most important raw materials used in the pharmaceutical industry. Whether you are manufacturing injectable medicines, liquid syrups, vaccines, ophthalmic solutions, or biotechnology products, the quality of water directly affects the quality of the final product. Even the smallest impurity can compromise product safety, reduce manufacturing efficiency, and create regulatory compliance issues.
This is why pharmaceutical companies invest in advanced water purification systems that consistently produce Water for Injection (WFI) and Pure Steam according to international standards. Among these systems, the Multi-Column Distillation Plant has become the preferred solution for pharmaceutical manufacturers around the world due to its exceptional purity, reliability, and energy-efficient operation.
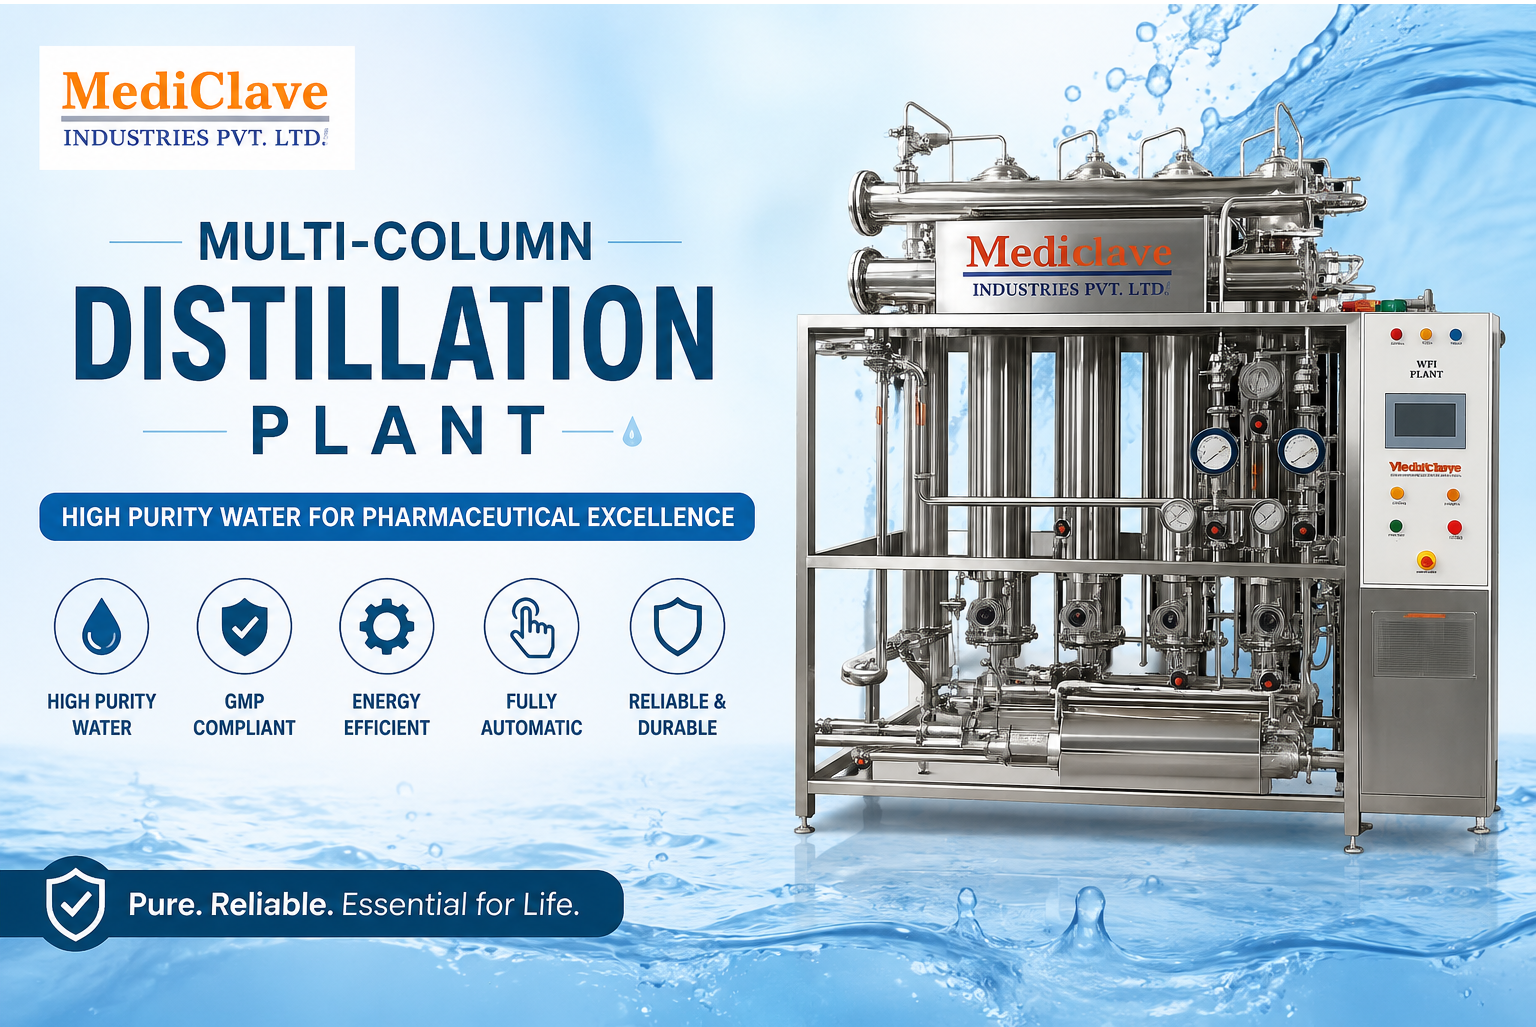
At Mediclave Industries Pvt. Ltd., we manufacture high-quality Multi-Column Distillation Plants designed to meet the demanding requirements of pharmaceutical, biotechnology, healthcare, and research industries. Our systems are engineered using premium stainless steel, advanced automation, and GMP-compliant designs to ensure reliable production of highly purified water.
In this complete guide, you will learn everything about Multi-Column Distillation Plants, including how they work, their advantages, applications, major components, maintenance requirements, selection criteria, and why Mediclave Industries is a trusted manufacturer in India.
What is a Multi-Column Distillation Plant?
A Multi-Column Distillation Plant (MCDP) is a pharmaceutical water generation system that produces Water for Injection (WFI) through the process of multiple-stage distillation.
Unlike conventional water purification methods, multi-column distillation uses several interconnected columns where purified steam transfers heat from one column to the next. This process efficiently removes dissolved salts, microorganisms, pyrogens, endotoxins, organic impurities, and other contaminants while conserving energy.
The final output is ultra-pure water that complies with the latest pharmacopeia standards including:
USP
EP
IP
JP
WHO GMP
FDA Guidelines
cGMP Standards
Because of its exceptional purity, Water for Injection generated by Multi-Column Distillation Plants is widely used in pharmaceutical manufacturing.
Why High-Purity Water Matters
Water is not simply another ingredient.
It is used throughout pharmaceutical manufacturing for:
Injectable medicines
IV fluids
Vaccine production
Liquid formulations
Equipment cleaning
CIP systems
SIP systems
Sterile manufacturing
Laboratory testing
Biotechnology production
If water quality is poor, it may introduce:
Microbial contamination
Endotoxins
Minerals
Organic compounds
Product instability
Batch rejection
Regulatory observations
A reliable Multi-Column Distillation Plant eliminates these risks by consistently producing pharmaceutical-grade purified water.
How Does a Multi-Column Distillation Plant Work?
The operating principle is based on repeated evaporation and condensation.
The process includes several stages:
Step 1: Feed Water Preparation
Purified water enters the first column after pretreatment.
Step 2: Steam Heating
Industrial steam heats the feed water until it evaporates.
Step 3: Multiple Distillation Columns
Instead of wasting heat after the first evaporation, the generated steam transfers energy to the next column.
Each successive column reuses energy from the previous stage, significantly improving efficiency.
Step 4: Removal of Contaminants
During evaporation:
Pyrogens remain behind
Salts remain behind
Heavy metals remain behind
Microorganisms are eliminated
Endotoxins are separated
Non-volatile impurities are removed
Step 5: Condensation
The purified steam condenses into pharmaceutical-grade Water for Injection.
Step 6: Collection
The WFI is transferred to a storage system for further distribution.
Many manufacturers pair the plant with a WFI Storage & Distribution System to maintain purity until point of use.
Learn more about Mediclave's WFI Storage & Distribution System:
https://www.mediclaveindustries.in/product/wfi-storage-distribution-system/
Major Components of a Multi-Column Distillation Plant
A standard pharmaceutical Multi-Column Distillation Plant includes:
Evaporator columns
Heat exchangers
Feed water pump
Steam separator
Condenser
Distillate cooler
Automatic control panel
PLC system
Temperature sensors
Pressure gauges
Safety valves
Stainless Steel piping
Sanitary valves
Instrumentation
Every component is designed to ensure contamination-free production.
Why Multiple Columns Are Used
Using multiple columns offers significant advantages compared to single-stage distillation.
Benefits include:
Higher thermal efficiency
Lower steam consumption
Lower operating costs
Better recovery of heat
Continuous operation
Stable production
Better product quality
This design has become the global standard for pharmaceutical Water for Injection generation.
Key Features of Mediclave Multi-Column Distillation Plant
Mediclave Industries manufactures systems featuring:
GMP compliant construction
SS316L contact parts
SS304 external body
PLC automation
Touch screen HMI
Fully automatic operation
Low maintenance
High energy efficiency
Compact footprint
Sanitary design
Easy cleaning
Continuous production
High safety standards
Long service life
Every plant is tested before dispatch to ensure dependable performance.
Advantages of Multi-Column Distillation Plant
Exceptional Water Purity
Produces Water for Injection meeting pharmaceutical standards.
Energy Efficient
Multiple columns recycle heat, reducing steam consumption.
Reliable Operation
Continuous production minimizes manufacturing downtime.
Low Maintenance
Simple design allows easy servicing.
Long Equipment Life
Premium stainless steel construction ensures durability.
Automation
PLC control reduces operator dependency.
Regulatory Compliance
Designed according to GMP and pharmaceutical validation requirements.
Better Manufacturing Quality
Consistent water quality improves product consistency.
Industries That Use Multi-Column Distillation Plants
These systems are widely installed in:
Pharmaceutical companies
Biotechnology industries
Injectable manufacturing plants
Vaccine manufacturers
Research laboratories
Healthcare industries
Medical device manufacturers
Veterinary pharmaceutical companies
Cosmetic manufacturing
Nutraceutical industries
Applications of Water Produced
Water generated by Multi-Column Distillation Plants is used for:
Injectable formulations
Vaccine manufacturing
Ampoule production
Eye drops
IV fluids
Sterile cleaning
Pharmaceutical washing
Sterile process equipment
Laboratory preparation
Biotechnology products
Integration with Other Pharmaceutical Systems
A complete pharmaceutical water system usually includes several interconnected systems.
For example, purified water generated through pretreatment is supplied to the Multi-Column Distillation Plant, while the generated Water for Injection is stored using a WFI Storage & Distribution System.
Many facilities also install a Pure Steam Generator to produce high-purity steam for sterilization applications.
Explore Mediclave's Pure Steam Generator:
https://www.mediclaveindustries.in/product/pure-steam-generator/
The generated pure steam is commonly used with pharmaceutical sterilization equipment such as the Saturated Steam Sterilizer.
Learn more:
https://www.mediclaveindustries.in/product/saturated-steam-sterilizer/
Cleaning pharmaceutical manufacturing equipment is equally important. Mediclave also provides advanced CIP & SIP Systems for automated cleaning and sterilization processes.
Read more:
https://www.mediclaveindustries.in/product/cip-sip-system/
Together, these systems create a complete pharmaceutical manufacturing solution.
Automation Features
Modern Multi-Column Distillation Plants include advanced automation such as:
PLC control
Recipe management
Alarm systems
Password protection
Data logging
Automatic shutdown
Automatic startup
Online monitoring
Validation support
Automation reduces human errors while increasing operational efficiency.
Importance of Validation
Pharmaceutical manufacturers must validate every water generation system.
Validation generally includes:
Design Qualification (DQ)
Installation Qualification (IQ)
Operational Qualification (OQ)
Performance Qualification (PQ)
These validation activities ensure the plant consistently produces compliant Water for Injection.
Maintenance Tips
Regular maintenance helps maximize equipment life.
Recommended practices include:
Inspect pressure gauges regularly.
Monitor conductivity.
Check temperature readings.
Clean condensers.
Replace worn gaskets.
Calibrate sensors.
Inspect valves.
Verify automation functions.
Maintain sanitary piping.
Schedule preventive maintenance.
Following these practices helps ensure uninterrupted production.
Factors to Consider Before Buying
Choosing the right Multi-Column Distillation Plant requires careful evaluation.
Consider:
Production Capacity
Select equipment according to daily WFI requirements.
Material Quality
SS316L contact parts are preferred.
Automation
PLC and HMI simplify operation.
GMP Compliance
Ensure pharmaceutical standards are met.
Energy Efficiency
Lower steam consumption reduces operating costs.
Service Support
Reliable after-sales service is essential.
Future Expansion
Choose a system that accommodates future production growth.
Why Mediclave Industries?
Mediclave Industries Pvt. Ltd. has built a strong reputation for manufacturing pharmaceutical equipment that combines quality, innovation, and reliability.
Customers choose Mediclave because of:
Experienced engineering team
Customized solutions
High-quality stainless steel construction
GMP-compliant manufacturing
Modern production facility
Strict quality inspections
Excellent after-sales support
Competitive pricing
Timely delivery
Comprehensive documentation
Our objective is to help pharmaceutical companies achieve consistent production with dependable equipment.
Building a Complete Pharmaceutical Manufacturing Facility
Many pharmaceutical manufacturers source multiple process systems from a single trusted supplier to ensure compatibility and streamlined support.
In addition to Multi-Column Distillation Plants, Mediclave Industries manufactures a wide range of pharmaceutical equipment including the Liquid Syrup Manufacturing Plant for oral liquid production:
https://www.mediclaveindustries.in/product/liquid-syrup-manufacturing-plant/
For semi-solid formulations, the Cream Manufacturing Plant (Ointment Manufacturing Plant) provides efficient mixing, homogenization, and processing:
https://www.mediclaveindustries.in/product/cream-manufacturing-plant/
By integrating high-quality water generation systems with advanced manufacturing equipment, pharmaceutical companies can build efficient, compliant, and future-ready production facilities.
Future of Pharmaceutical Water Systems
The pharmaceutical industry is moving toward smarter, more energy-efficient, and highly automated manufacturing processes.
Future Multi-Column Distillation Plants are expected to include:
Industry 4.0 integration
Remote diagnostics
Predictive maintenance
IoT monitoring
Advanced energy recovery
Digital validation records
Improved automation
Enhanced sustainability features
These innovations will further improve reliability while reducing operating costs.
Conclusion
A Multi-Column Distillation Plant is one of the most critical systems in any pharmaceutical manufacturing facility. It ensures the continuous production of Water for Injection with exceptional purity while maintaining compliance with global pharmaceutical standards. Thanks to its multi-stage design, it offers excellent thermal efficiency, lower operating costs, and dependable long-term performance.
When combined with complementary systems such as a Pure Steam Generator, WFI Storage & Distribution System, CIP & SIP System, and pharmaceutical sterilizers, it forms the backbone of a reliable and compliant pharmaceutical water and sterilization infrastructure.
If you are planning a new pharmaceutical facility or upgrading an existing one, investing in a high-quality Multi-Column Distillation Plant from Mediclave Industries Pvt. Ltd. can help you improve product quality, optimize operational efficiency, and meet stringent regulatory requirements. With robust engineering, GMP-compliant manufacturing, and dedicated customer support, Mediclave delivers solutions that pharmaceutical manufacturers can trust for years to come.
Frequently Asked Questions (FAQs)
1. What is a Multi-Column Distillation Plant used for?
It is used to produce Water for Injection (WFI) for pharmaceutical, biotechnology, and healthcare manufacturing applications.
2. Why is multi-column distillation preferred over single-stage distillation?
Multiple columns reuse heat energy, resulting in lower steam consumption, higher efficiency, and more economical operation.
3. Which industries require a Multi-Column Distillation Plant?
Pharmaceutical companies, biotech firms, vaccine manufacturers, research laboratories, cosmetic manufacturers, and medical device industries commonly use these systems.
4. Can the plant be integrated with other pharmaceutical equipment?
Yes. It is commonly integrated with Pure Steam Generators, WFI Storage & Distribution Systems, CIP & SIP Systems, and pharmaceutical sterilizers.
5. What material is typically used in a pharmaceutical Multi-Column Distillation Plant?
The product-contact parts are generally manufactured from high-quality SS316L stainless steel to ensure corrosion resistance, hygiene, and compliance with pharmaceutical standards.