
Introduction
Water purity is one of the most critical
requirements in pharmaceutical manufacturing. Pharmaceutical companies need
reliable water purification systems to maintain product quality, process
consistency, and compliance with applicable regulatory standards.
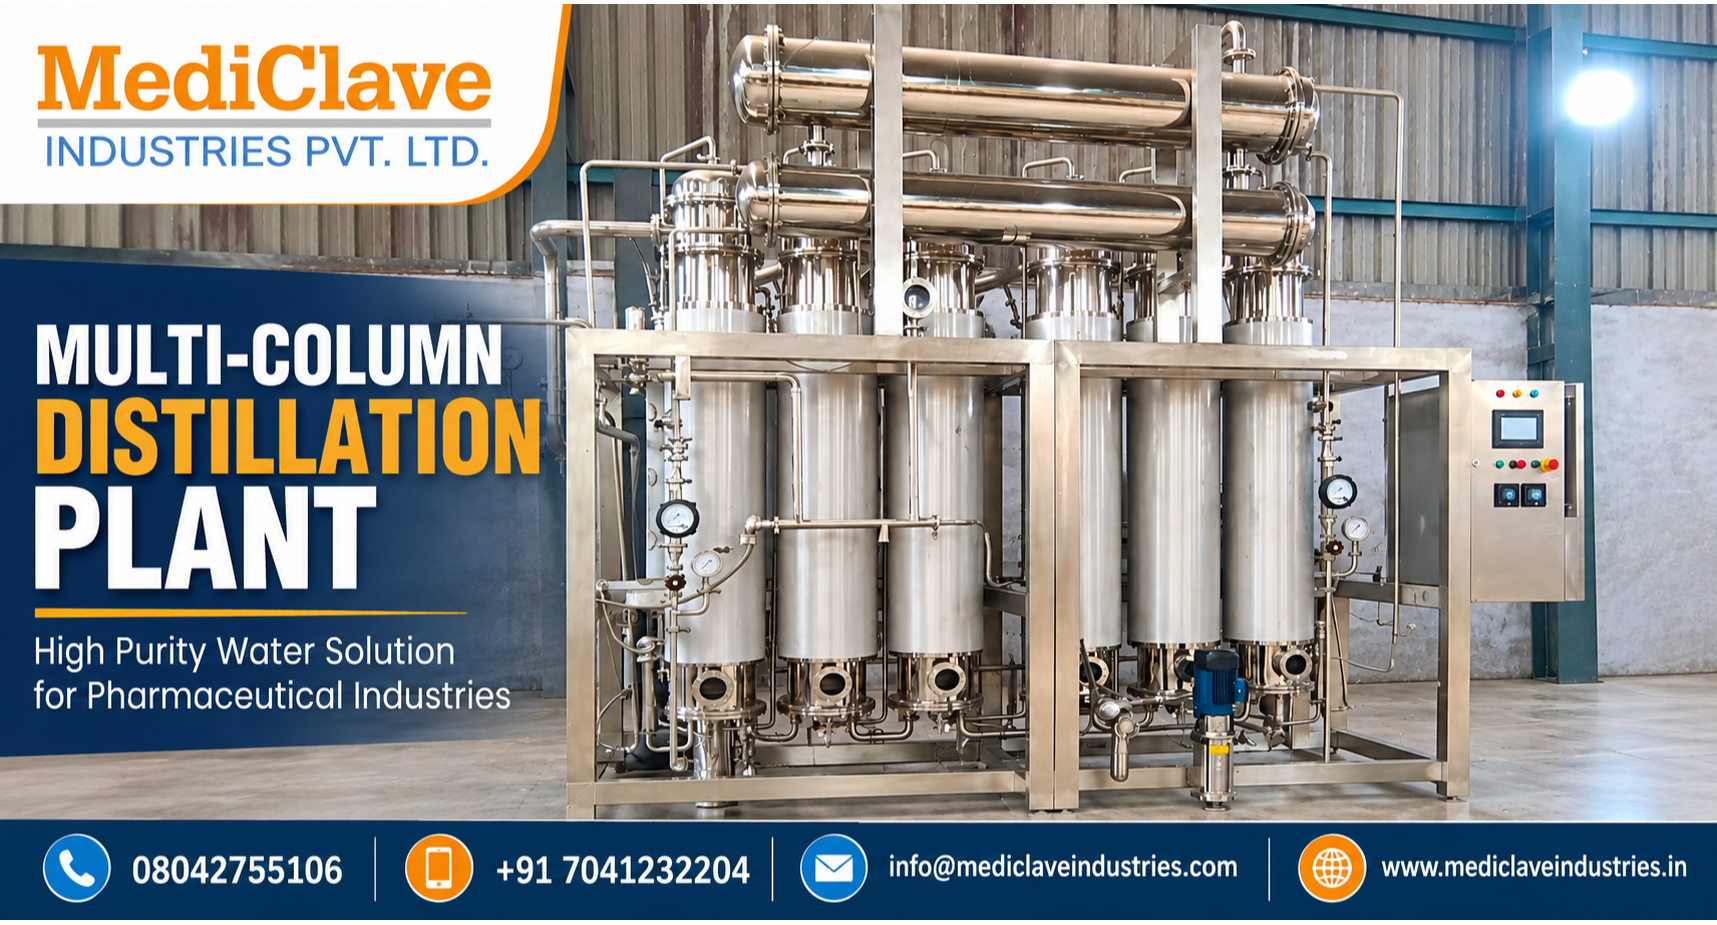
A Multi-Column Distillation Plant (MCDP) is an
advanced pharmaceutical water purification system designed to produce high-purity
distilled water, particularly Water for Injection (WFI), through controlled
evaporation, separation, and condensation.
Mediclave Industries Private Limited provides
pharmaceutical processing equipment solutions, including Multi-Column
Distillation Plants designed to support the demanding requirements of
pharmaceutical manufacturing facilities.
Our focus is on efficient equipment design,
reliable performance, hygienic construction, and long-term operational value.
What Is a Multi-Column
Distillation Plant?
A Multi-Column Distillation Plant is an industrial
water distillation system that uses multiple interconnected evaporation and
condensation stages to produce high-purity water.
Unlike conventional single-effect distillation
systems, multi-column or multi-effect distillation technology utilizes energy
from one stage to support evaporation in subsequent stages. This arrangement
helps improve thermal efficiency and reduce overall steam consumption.
The system is widely used in pharmaceutical
manufacturing facilities where controlled water quality is essential.
Properly designed, operated, and validated
distillation systems can produce Water for Injection that meets the applicable
pharmacopoeial requirements.
How Does a Multi-Column
Distillation Plant Work?
The working principle of a Multi-Column
Distillation Plant is based on multiple-effect evaporation and condensation.
Step 1: Feed Water Supply
Pre-treated feed water enters the distillation
system. Feed water quality must meet the equipment manufacturer's requirements
to minimize scaling, corrosion, and contamination risks.
Step 2: First Column Heating
In the first column, an external heating source
generates vapor from the feed water. Appropriate separation arrangements help
prevent liquid droplets and impurities from entering the purified vapor stream.
Step 3: Multiple-Effect Distillation
The generated vapor transfers heat to subsequent
columns, allowing additional water evaporation at progressively lower operating
pressures and temperatures.
Step 4: Vapor Separation
Specialized vapor separation arrangements reduce
liquid carryover and help control the transfer of nonvolatile contaminants,
including endotoxins.
Step 5: Condensation
The purified vapor is condensed under controlled
conditions to produce distilled water.
Step 6: WFI Collection
The distilled water is directed to a hygienic
collection or storage system. Its suitability as WFI must be established
through appropriate qualification, validation, and routine quality testing.
Key Features of Multi-Column
Distillation Plants
Mediclave Industries focuses on providing
pharmaceutical equipment solutions with features that can be configured
according to process and customer requirements.
- Stainless Steel Construction: Product-contact
components can be manufactured using suitable pharmaceutical-grade
stainless steel, such as SS 316L.
- Energy-Efficient Design: Multiple-effect
technology enables improved utilization of thermal energy.
- Automated Operation: PLC-based controls can
support monitoring and control of critical process parameters.
- Hygienic Construction: Appropriate piping,
surface finishes, and drainage arrangements help support contamination
control.
- Vapor Separation: Effective separation
technology helps reduce droplet carryover and associated impurities.
- Continuous Production: Systems can be designed
for continuous high-purity water generation.
- Safety Features: Pressure, temperature, and
other protective interlocks can be incorporated based on system design.
- Customizable Capacity: Equipment capacity and
configuration can be selected according to production requirements.
Note: Exact specifications, capacities, automation
features, and construction materials should be confirmed against the selected
Mediclave equipment model and technical quotation.
Applications of Multi-Column
Distillation Plants
Multi-Column Distillation Plants are used in
industries where consistent high-purity water production is essential.
1. Pharmaceutical Manufacturing
Used for generating WFI for pharmaceutical
manufacturing processes where the required water quality is specified.
2. Injectable Medicine Production
Supports the supply of qualified WFI for
manufacturing injectable pharmaceutical products.
3. Vaccine Manufacturing
Provides high-purity water for suitable vaccine
production processes and related applications.
4. Biotechnology Industries
Used in biotechnology facilities requiring
controlled water quality for manufacturing and processing operations.
5. Sterile Manufacturing
Facilities
Supports sterile manufacturing operations requiring
appropriately qualified WFI supplies.
6. Pharmaceutical Research and
Development
Useful for research, formulation development, and
pilot-scale operations where specified high-purity water is needed.
Benefits of Using a Multi-Column
Distillation Plant
High Water Purity
Distillation provides a robust purification barrier
for many dissolved and nonvolatile impurities. Effective design and process
control are essential for consistent performance.
Reduced Energy Consumption
By utilizing heat across multiple evaporation
effects, a Multi-Column Distillation Plant can offer lower steam consumption
than a comparable single-effect system.
Reliable WFI Production
When correctly installed, qualified, operated, and
maintained, the system supports consistent WFI production for pharmaceutical
applications.
Long Equipment Service Life
Suitable material selection, hygienic engineering,
proper maintenance, and appropriate operating conditions contribute to
equipment durability.
Automated Process Control
Automation can improve operational consistency,
process monitoring, alarm management, and recording of critical parameters.
Flexible Plant Integration
The equipment can be integrated with pharmaceutical
water pretreatment, storage, and distribution systems according to facility
requirements.
Multi-Column Distillation Plant
vs. Single-Effect Distillation Plant
|
Feature |
Multi-Column
Plant |
Single-Effect
Plant |
|
Distillation stages |
Multiple effects |
Single effect |
|
Energy utilization |
Generally more efficient |
Generally less efficient |
|
Steam consumption |
Typically lower per unit output |
Typically higher |
|
Initial investment |
Generally higher |
Generally lower |
|
System complexity |
Higher |
Lower |
|
Pharmaceutical WFI application |
Suitable with proper design and validation |
Possible with proper design and validation |
Actual performance and energy savings depend on
plant capacity, configuration, feed water conditions, and operating parameters.
Why Choose Mediclave Industries
Private Limited?
Choosing the right pharmaceutical equipment
manufacturer is important for long-term plant performance and reliable
production.
Mediclave Industries Private Limited focuses on
delivering pharmaceutical sterilization and processing equipment solutions that
meet customer-specific manufacturing requirements.
Key reasons to consider Mediclave Industries
include:
- Pharmaceutical equipment manufacturing
expertise
- Customer-specific equipment configurations
- Focus on hygienic design and suitable
materials
- Industrial automation options
- Technical coordination for equipment selection
- Solutions for pharmaceutical and healthcare
manufacturing applications
For additional pharmaceutical equipment solutions,
explore our website:
Mediclave Industries – Pharmaceutical
Equipment Manufacturer
You can also learn more about our pharmaceutical
processing and sterilization equipment solutions and
contact our team to discuss your project requirements.
Factors to Consider Before
Purchasing a Multi-Column Distillation Plant
Before selecting a Multi-Column Distillation Plant,
pharmaceutical manufacturers should evaluate the following requirements:
- Production capacity: Required WFI generation
capacity in liters per hour.
- Feed water quality: Pretreatment requirements
and acceptable feed water parameters.
- Utility availability: Steam, electrical power,
cooling water, and compressed air requirements.
- Material of construction: Suitable
pharmaceutical-grade materials and hygienic surface finishes.
- Automation requirements: PLC, HMI, alarms,
monitoring, and data-recording capabilities.
- Qualification documentation: Required design,
installation, operational, and performance qualification support.
- Maintenance accessibility: Ease of inspection,
servicing, and routine maintenance.
Careful equipment selection helps pharmaceutical
manufacturers optimize operational costs while meeting their process
requirements.
Conclusion
A Multi-Column Distillation Plant is an important
component of pharmaceutical water generation infrastructure. Its
multiple-effect distillation process enables efficient high-purity water
production while supporting stringent pharmaceutical manufacturing
requirements.
For companies looking for a Multi-Column
Distillation Plant Manufacturer in India, Mediclave Industries Private Limited
offers a point of contact for discussing pharmaceutical water generation
equipment requirements.
Whether you are planning a new pharmaceutical
facility or upgrading an existing water purification system, selecting the
right distillation technology is essential for reliable operation and long-term
performance.
Contact Mediclave Industries
Private Limited
Mediclave Industries Private Limited
08042755106
+91 7041232204
info@mediclaveindustries.com
Get in touch with our team for product information,
technical discussions, and quotation inquiries.