
Multi Column Distillation Plant: The Complete Guide to High-Purity Water Production for Pharmaceutical Manufacturing
Water is one of the most important raw materials used in the pharmaceutical industry. Every tablet, injection, syrup, ointment, and sterile product depends on high-quality purified water during manufacturing. Even the smallest contamination can affect product quality, reduce shelf life, or create safety concerns for patients. That is why pharmaceutical manufacturers invest in advanced water purification systems that consistently deliver water meeting international quality standards.
Among the most trusted technologies available today, the Multi Column Distillation Plant plays a vital role in producing Water for Injection (WFI) and high-purity distilled water required for pharmaceutical production. It combines advanced engineering, reliable performance, and consistent water quality to help manufacturers meet GMP, WHO, USFDA, and international regulatory requirements.
Whether you are planning a new pharmaceutical manufacturing facility or upgrading an existing water system, understanding how a Multi Column Distillation Plant works can help you make the right investment. In this comprehensive guide, we will explore everything you need to know about Multi Column Distillation Plants, including their working principle, components, benefits, applications, selection criteria, maintenance requirements, and why they remain one of the most dependable solutions for pharmaceutical water generation.
What is a Multi Column Distillation Plant?
A Multi Column Distillation Plant is an advanced pharmaceutical water purification system designed to produce high-purity distilled water or Water for Injection through multiple stages of evaporation and condensation. Unlike single-stage distillation systems, a multi-column design improves energy efficiency by reusing steam generated during each stage of the distillation process.
The system removes dissolved salts, bacteria, endotoxins, pyrogens, organic impurities, and other contaminants, ensuring the final water meets stringent pharmaceutical standards.
Multi Column Distillation Plants are widely used in pharmaceutical manufacturing, biotechnology, healthcare, research laboratories, vaccine production, injectable manufacturing, and medical device industries where the highest level of water purity is essential.
Why High-Purity Water Matters
Water is not just an ingredient; it is an essential part of the manufacturing process. It is used for:
Manufacturing injectable medicines
Producing IV fluids
Syrup manufacturing
Cleaning equipment
Sterilization processes
Laboratory testing
Washing pharmaceutical containers
CIP (Cleaning In Place)
SIP (Sterilization In Place)
Poor-quality water can introduce contaminants that compromise product quality, regulatory compliance, and patient safety. A properly designed Multi Column Distillation Plant eliminates these risks by consistently producing pharmaceutical-grade water.
How Does a Multi Column Distillation Plant Work?
The operating principle is based on multiple stages of evaporation and condensation.
The process begins with purified feed water entering the first distillation column. Clean steam heats the feed water, causing it to evaporate. As the steam rises, impurities, dissolved solids, microorganisms, and endotoxins remain behind.
The generated pure steam then enters the next column, where it serves as the heating source for another batch of feed water. This process continues through several columns, allowing energy to be reused efficiently while maintaining excellent water purity.
Finally, the purified steam is condensed into high-quality distilled water or Water for Injection. The finished water is then transferred to a storage and distribution system while maintaining pharmaceutical standards.
This multi-stage design offers significantly better thermal efficiency compared to conventional distillation systems.
Main Components of a Multi Column Distillation Plant
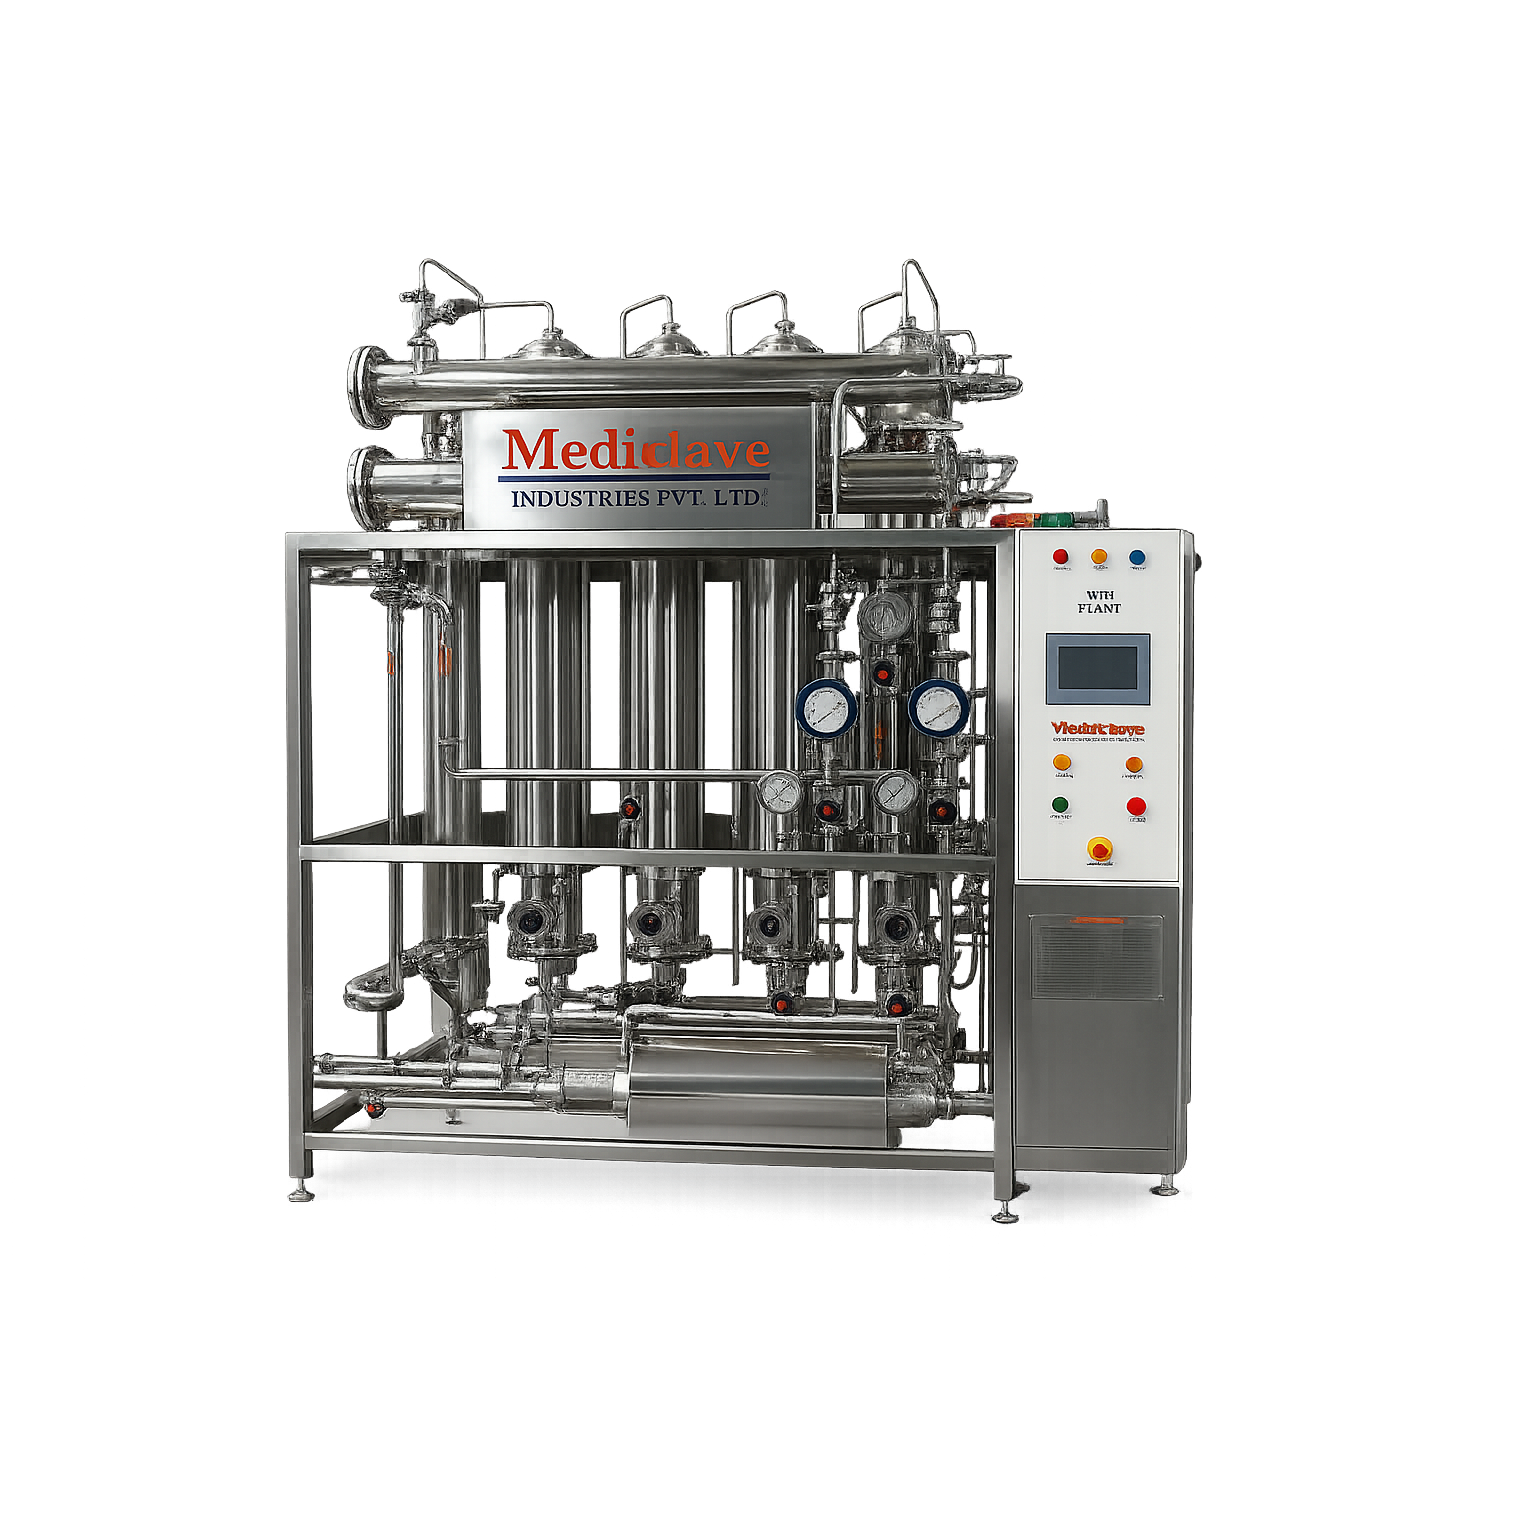
A typical pharmaceutical Multi Column Distillation Plant consists of several precisely engineered components, including:
Multiple distillation columns
Evaporators
Condensers
Steam separator
Feed water preheater
Heat exchangers
Instrumentation and sensors
Automatic control panel
Stainless steel piping
Safety valves
Temperature monitoring system
Pressure monitoring system
Product water outlet
Drain system
Each component is manufactured using pharmaceutical-grade stainless steel to ensure hygiene, durability, and corrosion resistance.
Key Features
Modern Multi Column Distillation Plants offer numerous advanced features such as:
Fully automatic operation
PLC-based control system
Touchscreen HMI
GMP-compliant construction
SS316L product contact parts
Low maintenance
Continuous production
High thermal efficiency
Low operating cost
Stable output quality
Automatic monitoring
Safety interlocks
Compact design
Reliable performance
Long service life
These features help pharmaceutical companies maximize production while maintaining regulatory compliance.
Advantages of Using a Multi Column Distillation Plant
Superior Water Quality
The biggest advantage is the production of consistently high-purity water that meets pharmaceutical standards.
Excellent Energy Efficiency
Multiple evaporation stages reuse thermal energy, reducing steam consumption and operating costs.
Continuous Operation
The plant is designed for uninterrupted production, ensuring a constant supply of purified water.
Reduced Operating Costs
Efficient energy utilization lowers long-term utility expenses.
Reliable Performance
Modern systems deliver stable production even during continuous manufacturing operations.
Regulatory Compliance
The plant supports GMP, WHO, FDA, and international pharmaceutical manufacturing standards.
Low Maintenance
High-quality stainless steel construction minimizes maintenance requirements and extends equipment life.
Applications of Multi Column Distillation Plants
The system is widely used across numerous industries.
Pharmaceutical Industry
Injectable manufacturing
Vaccine production
IV fluid production
Sterile drug manufacturing
Antibiotic production
Biotechnology
Biotechnology companies use high-purity water for sensitive biological manufacturing processes.
Hospitals
Large healthcare facilities require distilled water for sterilization, laboratory work, and critical applications.
Research Laboratories
Analytical laboratories rely on ultra-pure water for testing and research.
Medical Device Manufacturing
Medical device manufacturers use distilled water during production and cleaning processes.
Industries That Depend on Multi Column Distillation Plants
Pharmaceutical manufacturing
Biotechnology
Nutraceuticals
Cosmetics
Healthcare
Research institutions
Food processing
Chemical manufacturing
Vaccine production
Medical device manufacturing
Importance of Integration with Other Pharmaceutical Systems
A Multi Column Distillation Plant performs best when integrated with other pharmaceutical utility systems.
The purified water generated is typically stored and circulated using a WFI Storage & Distribution System, ensuring continuous availability throughout the production facility.
Similarly, pharmaceutical manufacturers often integrate the distillation system with Pure Steam Generators for sterilization applications and CIP & SIP Systems for automated equipment cleaning and sterilization.
Mediclave Industries manufactures these complementary systems to create complete pharmaceutical utility solutions that improve operational efficiency and regulatory compliance.
Relevant product pages include:
Multi Column Distillation Plant: https://www.mediclaveindustries.in/multi-column-distillation-plant
Pure Steam Generator: https://www.mediclaveindustries.in/pure-steam-generator
WFI Storage & Distribution System: https://www.mediclaveindustries.in/wfi-storage-distribution-system
CIP & SIP System: https://www.mediclaveindustries.in/cip-sip-system
Saturated Steam Sterilizer: https://www.mediclaveindustries.in/saturated-steam-sterilizer
These integrated solutions help pharmaceutical companies establish a complete, efficient, and GMP-compliant manufacturing environment.
How to Choose the Right Multi Column Distillation Plant
Selecting the right system requires careful evaluation of several factors.
Production Capacity
Choose a plant that matches your daily water consumption while allowing room for future expansion.
Material of Construction
SS316L contact parts provide excellent corrosion resistance and pharmaceutical compatibility.
Automation Level
A PLC-controlled automatic system improves process reliability and minimizes operator intervention.
Validation Support
Ensure the manufacturer provides IQ, OQ, PQ documentation and validation assistance.
Energy Consumption
Compare steam usage and overall operating costs before making a decision.
Service Support
Reliable after-sales service and spare parts availability are essential for uninterrupted production.
Regulatory Standards
Pharmaceutical manufacturers should ensure that the selected system complies with:
WHO GMP
USFDA guidelines
EU GMP
cGMP
ISPE recommendations
Pharmacopoeia requirements
ISO quality standards
Compliance helps manufacturers pass audits and maintain product quality.
Maintenance Tips
Routine maintenance ensures consistent performance and extends equipment life.
Recommended practices include:
Regular inspection of pipelines
Calibration of sensors
Cleaning heat exchangers
Checking steam pressure
Monitoring feed water quality
Inspecting valves
Verifying instrumentation
Replacing worn seals
Maintaining automatic controls
Recording maintenance activities
Preventive maintenance significantly reduces downtime and improves productivity.
Common Challenges and Their Solutions
Some common operational challenges include scaling, reduced steam efficiency, feed water fluctuations, improper maintenance, and instrumentation errors.
These issues can be minimized by using properly pretreated feed water, following preventive maintenance schedules, monitoring operating parameters, and choosing equipment manufactured according to pharmaceutical engineering standards.
Why Pharmaceutical Companies Prefer Multi Column Distillation Plants
Pharmaceutical companies prioritize equipment that delivers consistent quality, operational reliability, and regulatory compliance. A Multi Column Distillation Plant fulfills all these requirements while reducing operating costs and improving energy efficiency.
Its ability to produce Water for Injection with minimal contamination risk makes it an indispensable utility in modern pharmaceutical manufacturing facilities.
As production demands increase and regulatory expectations become more stringent, investing in advanced water purification technology becomes even more critical.
Why Choose Mediclave Industries?
Mediclave Industries is committed to manufacturing high-quality pharmaceutical process equipment and water systems designed for reliability, efficiency, and compliance.
The company's engineering expertise, precision manufacturing, and focus on customer satisfaction make it a trusted partner for pharmaceutical manufacturers across India and international markets.
In addition to Multi Column Distillation Plants, Mediclave Industries offers a complete range of pharmaceutical equipment, including Pure Steam Generators, WFI Storage & Distribution Systems, CIP & SIP Systems, Saturated Steam Sterilizers, Injectable Manufacturing Vessels, Liquid Syrup Manufacturing Plants, Ointment Manufacturing Plants, and many other process solutions.
By choosing an integrated solution from a single manufacturer, pharmaceutical companies can simplify installation, improve compatibility between systems, and ensure long-term operational reliability.
Conclusion
A Multi Column Distillation Plant is far more than a water purification system—it is the foundation of pharmaceutical-quality manufacturing. From producing Water for Injection to supporting sterile manufacturing, laboratory operations, cleaning processes, and regulatory compliance, it plays an essential role in ensuring product safety and manufacturing excellence.
With its energy-efficient multi-stage design, automatic operation, superior water purity, and dependable performance, it remains the preferred choice for pharmaceutical manufacturers worldwide. When integrated with systems such as Pure Steam Generators, WFI Storage & Distribution Systems, CIP & SIP Systems, and pharmaceutical sterilizers, it creates a complete utility infrastructure capable of meeting today's demanding production requirements.
If your organization is planning to establish or upgrade a pharmaceutical water generation facility, investing in a high-quality Multi Column Distillation Plant from Mediclave Industries can help improve productivity, reduce operating costs, and maintain the highest standards of pharmaceutical manufacturing for years to come.