
In the pharmaceutical and healthcare industries, sterilization is one of the most important steps in ensuring product safety and quality. Every injectable medicine, IV fluid, biological product, or temperature-sensitive pharmaceutical item must be sterilized properly before it reaches patients. Even the smallest contamination can affect product quality, reduce shelf life, and, more importantly, put patient safety at risk.
As pharmaceutical products become more advanced and packaging materials become more delicate, traditional steam sterilization alone is not always enough. Many products cannot tolerate direct saturated steam because it may damage the packaging, alter the product, or create uneven heating. This is where the Steam + Air Mixture Sterilizer becomes the preferred solution.
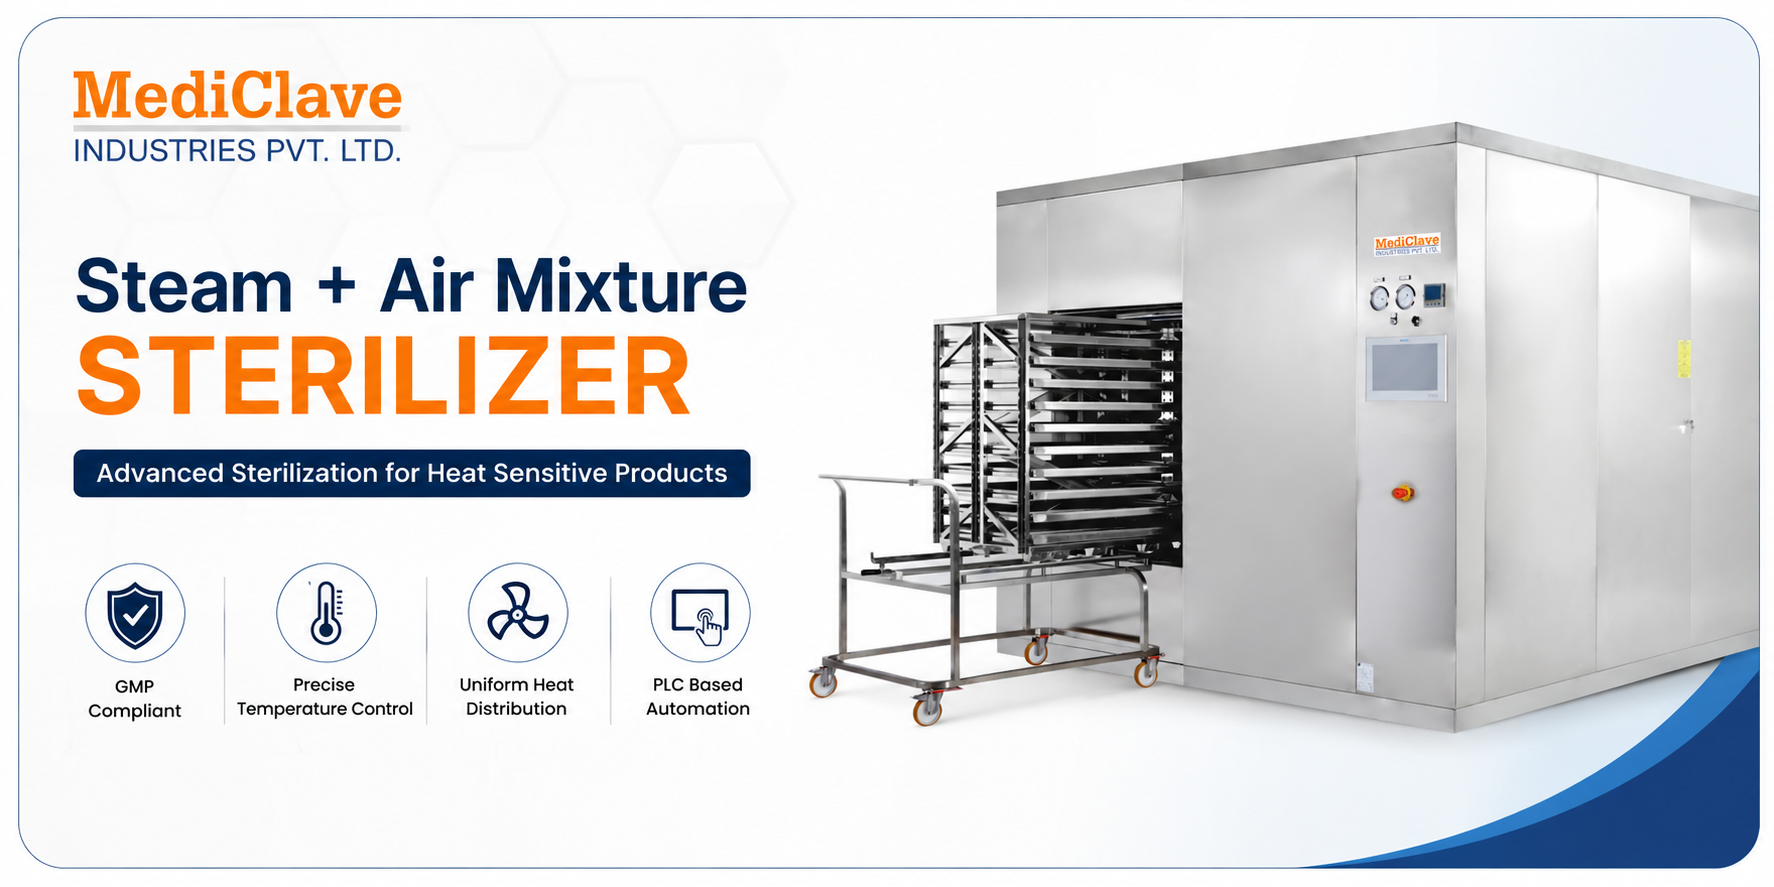
A Steam + Air Mixture Sterilizer combines saturated steam with filtered compressed air to create uniform temperature distribution throughout the sterilization chamber. This technology allows pharmaceutical manufacturers to sterilize sensitive products safely while maintaining packaging integrity and ensuring complete sterilization.
In this comprehensive guide, we'll explain everything you need to know about Steam + Air Mixture Sterilizers, including their working principle, applications, advantages, components, validation requirements, and why they are becoming an essential part of modern pharmaceutical manufacturing.
What Is a Steam + Air Mixture Sterilizer?
A Steam + Air Mixture Sterilizer is a high-performance pharmaceutical sterilization system designed specifically for products that require controlled pressure during sterilization.
Unlike conventional steam sterilizers that rely solely on saturated steam, this system injects both clean steam and sterile filtered compressed air into the chamber. Powerful circulation fans continuously mix the steam and air, ensuring an even temperature throughout the chamber.
The added air pressure supports delicate containers such as:
- Plastic bottles
- IV bags
- Blow-Fill-Seal (BFS) containers
- Prefilled syringes
- Flexible pouches
- Plastic ampoules
- Ophthalmic containers
Without this controlled air pressure, these containers could deform, collapse, or burst during sterilization.
Why Is Steam Alone Not Always Enough?
Traditional saturated steam sterilization works perfectly for metal instruments, glass bottles, and laboratory equipment because steam can freely contact every surface.
However, many pharmaceutical products are packaged in flexible or plastic materials. During sterilization, internal pressure inside these containers increases significantly.
If external chamber pressure is not properly balanced:
- Containers may swell
- Plastic bottles may collapse
- IV bags may burst
- Packaging seals may fail
- Product quality may be compromised
Steam + Air Mixture Sterilizers solve this problem by maintaining carefully controlled external pressure throughout the sterilization cycle.
How Does a Steam + Air Mixture Sterilizer Work?
The sterilization process follows several carefully controlled stages.
1. Loading
Products are loaded into stainless steel trays or racks.
The chamber door is closed and automatically locked.
2. Air Removal
The chamber removes unwanted air using vacuum or controlled displacement.
This improves steam penetration.
3. Steam Introduction
Clean saturated steam enters the chamber.
Instead of completely replacing the air, a controlled amount of sterile compressed air is introduced simultaneously.
4. Steam-Air Mixing
A high-capacity circulation fan continuously mixes:
- Steam
- Sterile compressed air
This produces extremely uniform temperature distribution.
5. Sterilization Hold Time
The chamber maintains:
- Temperature
- Pressure
- Humidity
- Exposure time
Typical sterilization temperatures include:
- 105°C
- 110°C
- 115°C
- 121°C
- 124°C
depending on product requirements.
6. Controlled Cooling
Cooling begins while maintaining chamber pressure.
This prevents deformation of plastic containers.
7. Drying
Remaining moisture is removed before unloading.
Products exit dry, sterile, and ready for further processing.
Main Components of a Steam + Air Mixture Sterilizer
A pharmaceutical-grade Steam + Air Mixture Sterilizer typically includes:
- Stainless steel sterilization chamber
- Steam inlet system
- Sterile compressed air system
- High-efficiency circulation fan
- Cooling water system
- PLC automation
- Touchscreen HMI
- Pressure sensors
- Temperature sensors
- Safety valves
- Automatic control valves
- Drain system
- Data logger
- Validation ports
Every component is designed according to pharmaceutical GMP requirements.
Why Is Uniform Temperature Distribution So Important?
One of the biggest challenges in sterilization is achieving exactly the same temperature throughout the chamber.
Even small temperature variations may leave certain products under-sterilized.
Steam + Air Mixture technology offers excellent temperature uniformity because:
- Steam and air circulate continuously.
- Fans eliminate cold spots.
- Heat reaches every product evenly.
- Sterilization becomes highly repeatable.
This improves both product safety and process validation.
Products That Can Be Sterilized
Steam + Air Mixture Sterilizers are widely used for:
- IV fluids
- Infusion bottles
- Plastic bottles
- Plastic ampoules
- BFS containers
- Eye drops
- Nasal sprays
- Dialysis solutions
- Injectable solutions
- Saline bottles
- Irrigation solutions
- Flexible pouches
- Prefilled syringes
- Biological products
- Medical liquids
- Heat-sensitive pharmaceutical products
Industries That Use Steam + Air Mixture Sterilizers
These sterilizers are commonly installed in:
- Pharmaceutical manufacturing plants
- Injectable production facilities
- Biotechnology companies
- Vaccine manufacturing plants
- Medical device industries
- Contract manufacturing organizations (CMOs)
- Research laboratories
- Healthcare manufacturing facilities
Advantages of Steam + Air Mixture Sterilizers
Manufacturers choose these systems because they provide several important benefits.
Excellent Temperature Uniformity
Steam and air circulation create consistent heating throughout the chamber.
Protection of Packaging
Flexible containers remain stable because chamber pressure matches internal product pressure.
Reduced Product Damage
The risk of deformation or bursting is significantly reduced.
Reliable Sterility Assurance
Uniform heat distribution helps achieve reliable sterilization validation.
Suitable for Sensitive Products
Products that cannot tolerate conventional steam sterilization can often be processed safely.
Fully Automatic Operation
Modern systems operate using programmable PLC controls with minimal operator intervention.
Data Recording
Automatic recording of:
- Temperature
- Pressure
- Cycle parameters
- Alarm history
supports regulatory compliance.
GMP Compliance
High-quality systems are designed according to:
- GMP
- cGMP
- FDA
- WHO
- EU GMP
guidelines.
Difference Between Steam Sterilizer and Steam + Air Mixture Sterilizer
Many people confuse these two technologies.
A conventional saturated steam sterilizer relies only on steam. It is ideal for metal instruments, glass containers, surgical equipment, and products that allow direct steam contact.
A Steam + Air Mixture Sterilizer, on the other hand, combines steam with sterile compressed air to maintain pressure while delivering highly uniform heating. This makes it especially suitable for plastic containers, IV bags, BFS products, and other pressure-sensitive pharmaceutical packaging.
For applications involving traditional pharmaceutical sterilization, manufacturers often also use the Saturated Steam Sterilizer (Autoclave) available from Mediclave Industries. Likewise, products requiring terminal sterilization with circulating water may benefit from the Super Heated Water Shower Sterilizer, depending on the product and packaging design. Selecting the right sterilization technology depends on the product characteristics, packaging material, and process requirements.
Validation Requirements
Validation is essential before production begins.
Common validation activities include:
Installation Qualification (IQ)
Verifies correct installation.
Operational Qualification (OQ)
Confirms that every function operates correctly.
Performance Qualification (PQ)
Demonstrates successful sterilization under actual production conditions.
Heat Distribution Study
Temperature sensors are placed throughout the chamber.
This verifies uniform heating.
Heat Penetration Study
Temperature probes are inserted inside representative products.
This confirms complete sterilization.
Biological Indicator Testing
Biological indicators verify microbial destruction during sterilization cycles.
Automation Features
Modern pharmaceutical sterilizers include advanced automation such as:
- PLC control
- Recipe management
- Password protection
- Batch recording
- Electronic data storage
- Alarm monitoring
- Automatic report generation
- Remote diagnostics
- SCADA compatibility
- Audit trail
- 21 CFR Part 11 support (where required)
Automation reduces operator errors while improving process consistency.
Energy Efficiency
Modern Steam + Air Mixture Sterilizers are designed to reduce operating costs.
Energy-saving features may include:
- Optimized steam consumption
- Insulated chambers
- Efficient circulation fans
- Heat recovery systems
- Water-saving cooling systems
- Automatic cycle optimization
Lower utility consumption reduces manufacturing costs over time.
Maintenance Tips
Regular maintenance helps maximize equipment life.
Recommended maintenance includes:
- Cleaning the chamber
- Inspecting door seals
- Checking steam traps
- Calibrating sensors
- Verifying pressure gauges
- Inspecting air filters
- Lubricating moving parts
- Validating sterilization cycles periodically
- Testing safety valves
- Reviewing PLC alarms
Preventive maintenance minimizes unexpected downtime.
Choosing the Right Steam + Air Mixture Sterilizer
When selecting a system, consider:
- Chamber size
- Production capacity
- Product type
- Packaging material
- Utility availability
- Automation level
- Validation support
- Regulatory requirements
- Future production expansion
- Service availability
Working with an experienced manufacturer helps ensure the equipment matches your production needs.
Building a Complete Pharmaceutical Sterilization System
A Steam + Air Mixture Sterilizer often works alongside other critical pharmaceutical equipment to create an efficient and compliant manufacturing process. For example, high-quality clean steam generated by the Pure Steam Generator is essential for many sterilization applications. Similarly, pharmaceutical-grade water produced through the Multi Column Distillation Plant supports sterile manufacturing processes where Water for Injection (WFI) is required. To maintain hygiene across processing equipment, CIP & SIP Systems play an important role by enabling effective cleaning and sterilization of production lines before manufacturing begins.
By integrating these systems, pharmaceutical companies can establish a complete sterile manufacturing environment that supports consistent product quality, operational efficiency, and regulatory compliance.
Future Trends in Steam + Air Mixture Sterilization
The pharmaceutical industry continues to evolve rapidly.
Future Steam + Air Mixture Sterilizers are expected to include:
- AI-assisted process optimization
- Predictive maintenance
- IoT connectivity
- Cloud-based monitoring
- Digital validation support
- Enhanced energy efficiency
- Faster sterilization cycles
- Advanced analytics
- Improved data integrity
- Remote service capabilities
These innovations will further improve productivity while maintaining strict quality standards.
Why Choose Mediclave Industries?
Mediclave Industries designs and manufactures advanced pharmaceutical sterilization equipment that meets the demanding requirements of modern pharmaceutical production. With a focus on quality, reliability, automation, and regulatory compliance, the company provides solutions that help manufacturers achieve safe, efficient, and validated sterilization processes.
From Steam + Air Mixture Sterilizers to Saturated Steam Sterilizers, Super Heated Water Shower Sterilizers, Pure Steam Generators, Multi Column Distillation Plants, and CIP & SIP Systems, Mediclave Industries offers a comprehensive range of pharmaceutical process and sterilization equipment designed to support complete sterile manufacturing facilities.
Whether you are setting up a new production line or upgrading an existing plant, choosing the right sterilization technology is essential for protecting your products, ensuring patient safety, and meeting global regulatory standards.
Conclusion
A Steam + Air Mixture Sterilizer is one of the most advanced and reliable sterilization solutions available for pharmaceutical manufacturers handling pressure-sensitive products. By combining saturated steam with sterile compressed air, it delivers exceptional temperature uniformity while protecting delicate packaging from damage. This technology is especially valuable for sterilizing IV fluids, BFS containers, plastic bottles, flexible pouches, prefilled syringes, and other heat-sensitive pharmaceutical products.
Beyond providing dependable sterilization, these systems support GMP compliance, simplify validation, improve process consistency, and reduce the risk of product loss. When integrated with complementary equipment such as Pure Steam Generators, Multi Column Distillation Plants, and CIP & SIP Systems, they form the foundation of a complete sterile manufacturing environment.
As pharmaceutical manufacturing continues to advance, investing in modern sterilization technology is not just about meeting regulatory requirements—it is about delivering safer, higher-quality products to patients. A well-designed Steam + Air Mixture Sterilizer is a long-term investment in product integrity, operational efficiency, and manufacturing excellence.