
Transforming Pharmaceutical Sterilization: A Complete Guide to Steam + Air Mixture Sterilizer Technology
Sterilization is one of the most important stages in pharmaceutical manufacturing. When medicines, IV fluids, injectable products, or other sterile pharmaceutical products are manufactured, the sterilization process must be effective enough to destroy microorganisms while also protecting the product and its packaging. This becomes especially challenging when the products are filled into flexible or sealed containers that may deform, leak, or break if exposed to uncontrolled pressure.
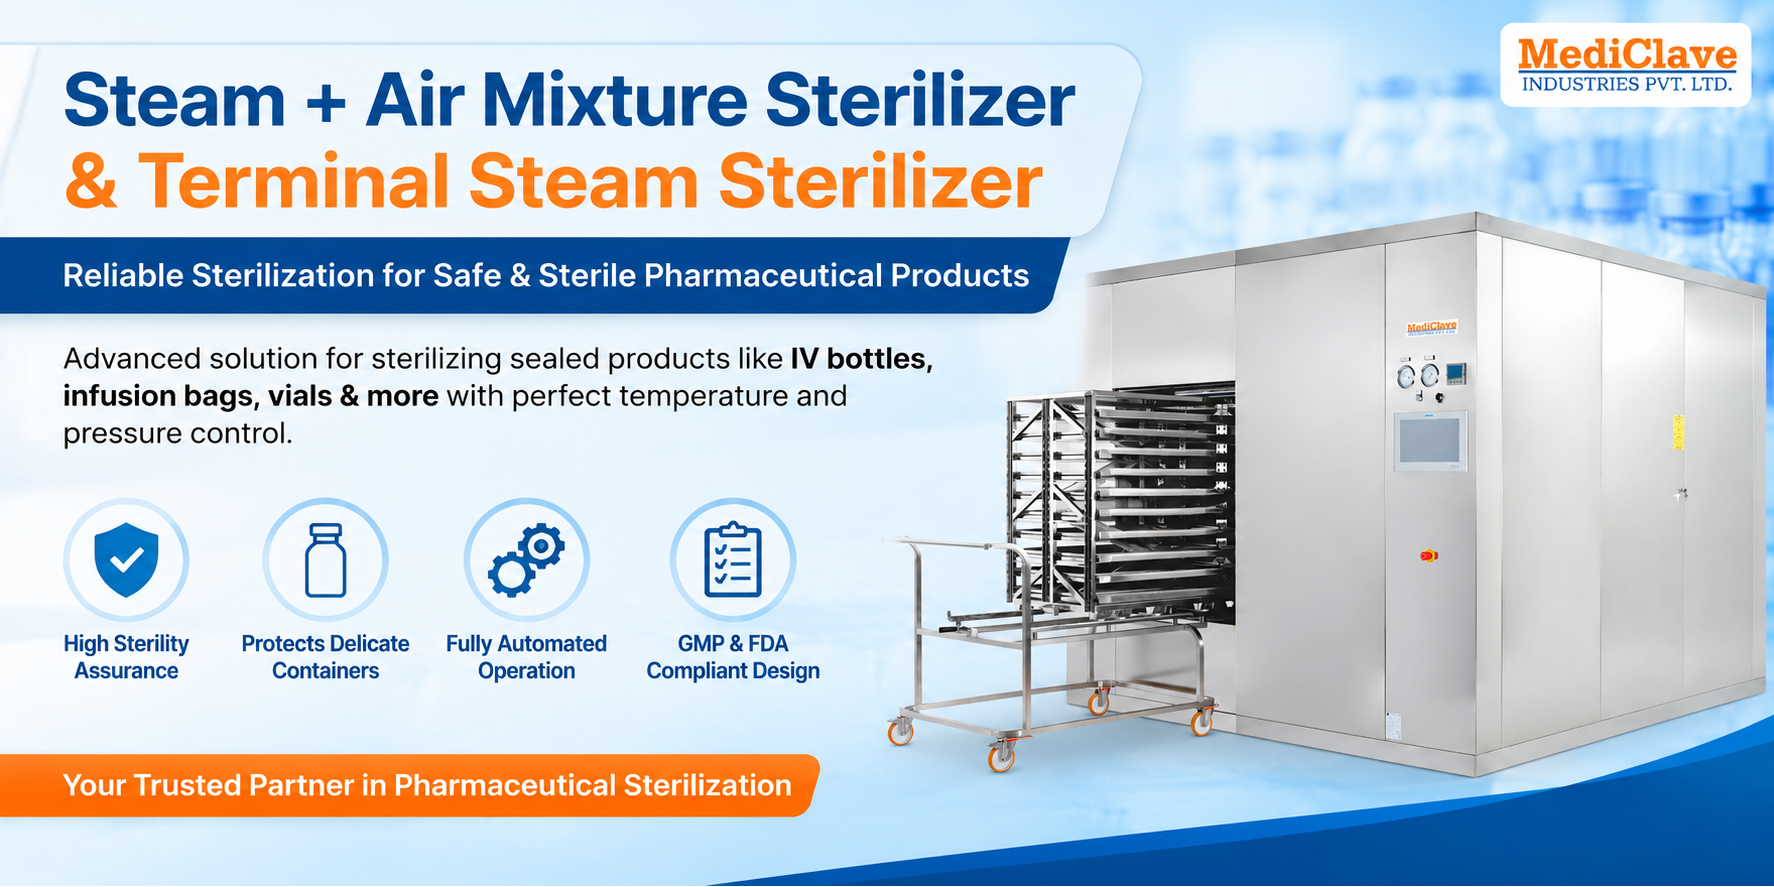
This is where a Steam + Air Mixture Sterilizer becomes an important solution. Unlike a conventional saturated steam sterilizer that relies primarily on steam, this advanced system uses a controlled combination of steam and filtered air to maintain a carefully balanced pressure and temperature environment. It is particularly useful for sterilizing sealed pharmaceutical products such as IV bags, infusion bottles, parenteral solutions, liquid injectables, and other products where container integrity is critical.
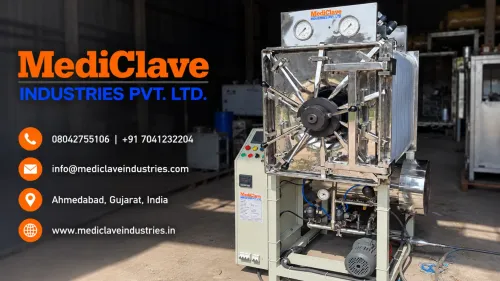
Mediclave Industries Pvt. Ltd. manufactures pharmaceutical sterilization systems designed for modern production environments, with solutions intended for pharmaceutical, biotechnology, healthcare, and life-science applications. Its Steam + Air Mixture Sterilizer is designed around controlled temperature, pressure, air circulation, and uniform heat distribution to support reliable sterilization processes.
What Is a Steam + Air Mixture Sterilizer?
A Steam + Air Mixture Sterilizer is a pharmaceutical sterilization system that combines saturated steam with filtered compressed air inside a controlled chamber. The steam provides the heat required for sterilization, while the controlled air pressure helps balance the pressure between the sterilization chamber and sealed containers.
This pressure-balancing capability is particularly important when sterilizing flexible or deformable containers. During a conventional steam cycle, differences between internal container pressure and chamber pressure can create mechanical stress. In sensitive applications, this may result in deformation, leakage, broken containers, or damaged seals.
A steam-air mixture system helps reduce these risks by continuously controlling the chamber environment.
The system can provide controlled management of:
Temperature
Chamber pressure
Steam supply
Filtered air supply
Air circulation
Cooling conditions
Sterilization holding time
This makes the technology especially valuable for pharmaceutical manufacturers that need both sterilization effectiveness and product protection.
Why Is Steam + Air Mixture Sterilization Important?
Traditional steam sterilization remains an excellent choice for many heat-resistant materials. However, not every pharmaceutical product can tolerate the same pressure conditions.
Consider an IV bag filled with liquid. During heating, the liquid and air inside the container expand. If the external chamber pressure does not remain appropriately balanced with the internal pressure of the container, the packaging may experience stress.
The same concern can apply to:
Plastic bottles
Infusion bags
Sealed vials
Pharmaceutical liquid containers
Syringes
Flexible packaging
Parenteral solutions
A Steam + Air Mixture Sterilizer addresses this challenge by combining steam with controlled filtered air. The objective is to create a stable sterilization environment in which the product receives the required heat exposure without unnecessary pressure shock.
This approach can help manufacturers protect packaging integrity, reduce product rejection, and achieve more consistent sterilization cycles.
How Does a Steam + Air Mixture Sterilizer Work?
The sterilization cycle consists of several controlled stages. The exact cycle parameters should always be established and validated according to the product, container, load configuration, and applicable process requirements.
1. Loading the Products
The first step is loading the pharmaceutical products into the sterilization chamber.
Products may include sealed IV bags, infusion bottles, injectable products, or other suitable pharmaceutical containers. Proper loading is important because the arrangement of products affects steam circulation, heat penetration, and overall temperature distribution.
The chamber is then securely closed before the sterilization cycle begins.
2. Air Management and Conditioning
The chamber environment is conditioned according to the programmed cycle.
Air management is important because uncontrolled air can interfere with heat transfer and temperature uniformity. In advanced systems, filtered air is introduced and controlled to establish the required pressure relationship within the chamber.
3. Steam Introduction
Clean or pharmaceutical-grade steam is introduced into the chamber.
Steam provides the thermal energy required to raise the product and chamber temperature to the selected sterilization condition. The steam and filtered air are circulated and controlled to achieve a uniform environment around the load.
4. Steam and Air Mixing
This is the key feature that differentiates the system from a conventional saturated steam sterilizer.
Steam and filtered air are mixed under controlled conditions. The air pressure helps balance the pressure around sealed containers while the steam supplies the heat necessary for sterilization.
The result is a controlled environment that can be particularly suitable for flexible and pressure-sensitive pharmaceutical packaging.
5. Sterilization Holding Phase
Once the required temperature and pressure conditions are achieved, the system maintains the programmed sterilization parameters for the validated holding period.
Depending on the product and validated cycle, pharmaceutical sterilization processes may use temperatures such as 121°C or other appropriate conditions. The exact temperature, holding time, pressure, and cycle profile must be determined through process development and validation rather than selected solely from a standard value.
6. Controlled Cooling
Cooling is another critical stage.
If a sealed container is suddenly exposed to a significant pressure change during cooling, the container may become damaged or deformed. Therefore, controlled cooling and pressure management are important for maintaining product and packaging integrity.
Filtered air and controlled cooling conditions can help maintain a suitable pressure balance while the product temperature gradually decreases.
7. Unloading
After the validated cycle is completed and the chamber reaches safe unloading conditions, the sterilized products can be removed for further processing, inspection, or storage according to the manufacturing process.
What Products Can Be Sterilized Using This Technology?
Steam + Air Mixture Sterilizers are particularly useful for pharmaceutical products where controlled pressure is important.
Typical applications can include:
IV bags
Infusion bottles
Parenteral solutions
Liquid injectables
Plastic pharmaceutical containers
Sealed bottles
Certain glass containers
Eye-care liquid products
Dialysis solutions
Nutritional solutions
Veterinary pharmaceutical products
Selected biotechnology products
The suitability of a particular product must always be confirmed through product-specific process development and validation.
For manufacturers producing injectable liquids, sterilization is only one part of the complete production process. The manufacturing vessel, mixing system, water quality, transfer system, cleaning process, and sterilization process must work together. Mediclave also provides an [Injectable Liquid Manufacturing Vessel]https://www.mediclaveindustries.in/ solution for pharmaceutical liquid manufacturing applications.
Steam + Air Mixture Sterilizer vs Saturated Steam Sterilizer
Both systems use steam, but their applications can be different.
A conventional saturated steam sterilizer is generally suitable for products and equipment that can tolerate direct exposure to saturated steam under pressure. It is widely used for sterilizing equipment, components, instruments, glassware, and other heat-resistant materials.
For pharmaceutical applications requiring this type of sterilization, Mediclave offers a [Saturated Steam Sterilizer (Autoclave)]https://www.mediclaveindustries.in/pharma-sterilization/saturated-steam-sterilizer-autoclave designed for controlled steam sterilization.
A Steam + Air Mixture Sterilizer is more specifically suited to applications where pressure balancing is important, especially sealed or flexible pharmaceutical containers.
The selection should therefore be based on:
Product characteristics
Container material
Product volume
Container geometry
Pressure sensitivity
Heat sensitivity
Required sterilization cycle
Production capacity
Validation requirements
Choosing equipment based only on the sterilization temperature is not enough. The complete product and packaging system must be considered.
Major Components of a Steam + Air Mixture Sterilizer
A modern pharmaceutical Steam + Air Mixture Sterilizer consists of several integrated systems designed to provide repeatable operation.
Stainless Steel Sterilization Chamber
The chamber is the main processing area. Pharmaceutical equipment commonly uses stainless steel construction and sanitary design principles for product-contact and critical surfaces.
Steam Distribution System
The steam distribution system delivers steam into the chamber and supports uniform heating of the load.
Filtered Air Supply
Filtered compressed air is introduced to control chamber pressure and support pressure balancing during sterilization and cooling.
Air Circulation System
Air circulation helps maintain a uniform chamber environment. Proper circulation reduces temperature variation and supports consistent heat distribution.
Temperature Sensors
Temperature sensors continuously monitor process conditions at selected locations.
Pressure Sensors
Pressure monitoring is essential because the process depends on accurate pressure control and balancing.
PLC Control System
A PLC-based automation system can manage programmed sterilization recipes, temperature, pressure, timing, alarms, and other process parameters.
HMI Touchscreen
The HMI provides operators with an easy-to-use interface for viewing process information and controlling authorized functions.
Data Recording
Process data recording is valuable for documentation, traceability, process review, and validation support.
Safety Interlocks
Safety systems help prevent unsafe operation, such as opening the chamber under inappropriate pressure conditions.
Key Benefits of Steam + Air Mixture Sterilizers
1. Better Protection of Flexible Containers
The controlled pressure environment can help reduce deformation and mechanical stress on flexible containers.
2. Uniform Heat Distribution
Controlled circulation of the steam-air mixture supports uniform exposure throughout the chamber.
3. Improved Product Integrity
When pressure and temperature are carefully managed, the risk of packaging-related failures can be reduced.
4. Consistent Sterilization
Automated process control helps maintain repeatable sterilization cycles when the process has been properly developed and validated.
5. Reduced Product Loss
Packaging damage can lead to rejected batches or individual units. Better pressure management can help minimize avoidable losses.
6. Automated Operation
PLC and HMI-based controls can reduce manual intervention and make routine operation easier.
7. Pharmaceutical Application Flexibility
The technology can be configured for different pharmaceutical products and container formats depending on process requirements.
8. Validation Support
Modern systems can incorporate temperature and pressure monitoring, data recording, alarms, and other features that support pharmaceutical process validation.
Why Pure Steam Quality Matters
The quality of steam used in pharmaceutical manufacturing is extremely important. Steam that comes into contact with critical pharmaceutical equipment or products should be suitable for the intended application.
This is why pharmaceutical facilities may require dedicated pure steam generation.
A [Pure Steam Generator]https://www.mediclaveindustries.in/latest-update/pure-steam-generator-ahmedabad/99 can produce high-purity steam for applications such as sterilization-in-place, pharmaceutical equipment sterilization, and sterile manufacturing processes.
The steam generation system and sterilizer should therefore be considered together when planning a new pharmaceutical facility or upgrading an existing production line.
Role of CIP and SIP in Pharmaceutical Manufacturing
Sterilization does not happen in isolation. Pharmaceutical production equipment must also be cleaned and sterilized properly before production.
CIP means Clean-In-Place, while SIP means Sterilize-In-Place. These systems allow process equipment such as vessels, tanks, pipelines, and associated equipment to be cleaned and sterilized without extensive dismantling.
Mediclave's [CIP & SIP System]https://www.mediclaveindustries.in/products/cip-sip-system/14 is designed for automated cleaning and sterilization of process equipment in pharmaceutical and biotechnology environments.
An integrated approach combining manufacturing equipment, CIP/SIP, pure steam, water systems, and terminal sterilization can create a more efficient and controlled sterile manufacturing environment.
Steam + Air Mixture Sterilization and Terminal Sterilization
Terminal sterilization means sterilizing a pharmaceutical product after it has been filled and sealed in its final container.
This approach can be highly valuable because the final packaged product undergoes the sterilization process, helping reduce the possibility of contamination after sterilization.
Steam + Air Mixture Sterilizers are particularly relevant to terminal sterilization applications involving sealed liquid products and flexible containers.
For pharmaceutical manufacturers producing IV fluids, parenteral solutions, or other suitable liquid products, terminal sterilization can become an important part of the overall contamination-control strategy.
Mediclave also provides a dedicated [Steam + Air Mixture Sterilizer & Terminal Steam Sterilizer]https://www.mediclaveindustries.in/latest-update/steam-air-mixture-sterilizer-terminal-steam-sterilizer/29 solution for these applications.
What Should You Consider Before Buying a Steam + Air Mixture Sterilizer?
Selecting the right sterilizer is an important investment decision. The machine should be selected according to the actual production process rather than simply choosing the largest chamber or the most automated model.
Consider the following factors:
Product Type
Identify exactly what you need to sterilize and whether the product is liquid, solid, flexible, or packaged.
Container Material
Plastic, glass, flexible bags, bottles, and other packaging materials can behave differently under temperature and pressure.
Batch Capacity
Calculate the number of units that need to be processed per batch and the required production frequency.
Chamber Size
The chamber should accommodate the required load while still allowing appropriate circulation and heat penetration.
Pressure Requirements
Pressure control is one of the most important factors when sterilizing sealed products.
Temperature Requirements
The sterilization temperature should be established according to product characteristics and validated process requirements.
Automation
Determine whether manual, semi-automatic, or fully automatic operation is appropriate for your facility.
Data Recording
For regulated pharmaceutical manufacturing, process data management and traceability can be important considerations.
Utility Availability
Check requirements for steam, compressed air, electricity, cooling water, drainage, and other utilities before installation.
Validation and Documentation
Discuss IQ, OQ, PQ, calibration, documentation, and other validation requirements with the equipment manufacturer before finalizing the machine.
Steam + Air Mixture Sterilizer for Pharmaceutical Manufacturing
Modern pharmaceutical manufacturing increasingly demands equipment that can combine sterilization effectiveness with product protection.
A Steam + Air Mixture Sterilizer is especially useful where conventional steam sterilization may create pressure-related challenges for sealed or flexible containers. By controlling the relationship between steam, filtered air, temperature, and chamber pressure, the system can provide a more suitable environment for sensitive pharmaceutical products.
The technology can support applications in pharmaceutical plants, injectable manufacturing facilities, biotechnology companies, veterinary pharmaceutical production, healthcare manufacturing, and other sterile processing environments.
For facilities that also need conventional high-volume steam sterilization, Mediclave's [Horizontal Rectangular High Pressure Steam Sterilizer]https://www.mediclaveindustries.in/ can be considered for suitable heat-resistant loads and applications.
For moisture-sensitive products or components, a [Dry Heat Sterilizer]https://www.mediclaveindustries.in/latest-update/dry-heat-sterilizer-the-complete-guide-to-reliable-sterilization-for-pharmaceutical-and-healthcare/227 may provide a more appropriate alternative because it uses high-temperature dry air instead of steam.
The key lesson is simple: there is no single sterilization technology that is ideal for every product. The right solution depends on the product, packaging, process requirements, and validated sterilization strategy.
Why Choose Mediclave Industries for Pharmaceutical Sterilization Equipment?
Mediclave Industries Pvt. Ltd. is an Indian manufacturer and engineering provider of pharmaceutical process equipment and sterilization solutions. The company offers equipment for pharmaceutical manufacturing, hospital CSSD applications, process systems, and pharmaceutical water systems.
For Steam + Air Mixture Sterilization, the focus is on controlled processing, reliable temperature and pressure management, hygienic construction, automation, and application-specific engineering.
A good sterilizer should not simply be treated as a machine purchase. It should be viewed as part of the complete manufacturing process. Proper equipment selection, installation, commissioning, operator training, preventive maintenance, calibration, and validation all contribute to long-term performance.
Final Thoughts
A Steam + Air Mixture Sterilizer is an advanced solution for pharmaceutical manufacturers who need reliable sterilization while protecting sealed and pressure-sensitive products. Its ability to combine steam with controlled filtered air makes it particularly valuable for applications involving IV bags, infusion fluids, parenteral solutions, liquid injectables, and other suitable pharmaceutical products.
The biggest advantage is not simply the use of steam. It is the ability to carefully control the sterilization environment so that temperature and pressure work together without unnecessarily compromising product or packaging integrity.
When selecting a system, manufacturers should consider the product, container, batch size, sterilization cycle, utilities, automation, validation requirements, and future production needs. A properly designed system can improve process consistency, reduce packaging-related losses, and support a more reliable sterile manufacturing operation.
Mediclave Industries provides pharmaceutical sterilization and process equipment for facilities looking to develop efficient and dependable manufacturing systems. From Steam + Air Mixture Sterilizers and Saturated Steam Sterilizers to Pure Steam Generators and CIP & SIP Systems, the right combination of technologies can help pharmaceutical manufacturers build a stronger and more controlled production environment.
Looking for a Steam + Air Mixture Sterilizer for your pharmaceutical manufacturing facility?
Contact Mediclave Industries Pvt. Ltd. to discuss your product, capacity, container type, sterilization requirements, automation preferences, and customized equipment needs.
Mediclave Industries Pvt. Ltd.
Email: info@mediclaveindustries.com
Phone: 08042755106
Website: https://www.mediclaveindustries.in/